A core component of the NI drivers, a security fix, and a date from which Windows may decide not to load it any more. The subject is dry, the check takes three minutes, and it is worth doing on every test bench running on NI Emerson (formerly National Instruments) hardware.
There is one kind of failure we really dislike: the one that turns up on a Monday morning on a test bench nobody has touched. Same software, same hardware, and yet the acquisition boards no longer appear in NI MAX. The cause almost always lies below the application, in the stack of drivers and services the bench depends on without anyone giving them a thought. The next opportunity of this kind has a date: 10 November 2026. NI Emerson has released a security fix for NI-PAL, a low-level component present on most PCs with NI drivers installed, and Microsoft has added the older versions of this component to its vulnerable driver list, the one Windows can refuse to load. Our colleagues at Mesulog published an information note on 22 October that goes through NI's instructions point by point; here, we look at what it actually changes for a test bench. This article explains what NI-PAL is, what the security advisory says, why the date matters, how to check a bench in three minutes, and where the pitfalls are.
A core component, but an inconspicuous one
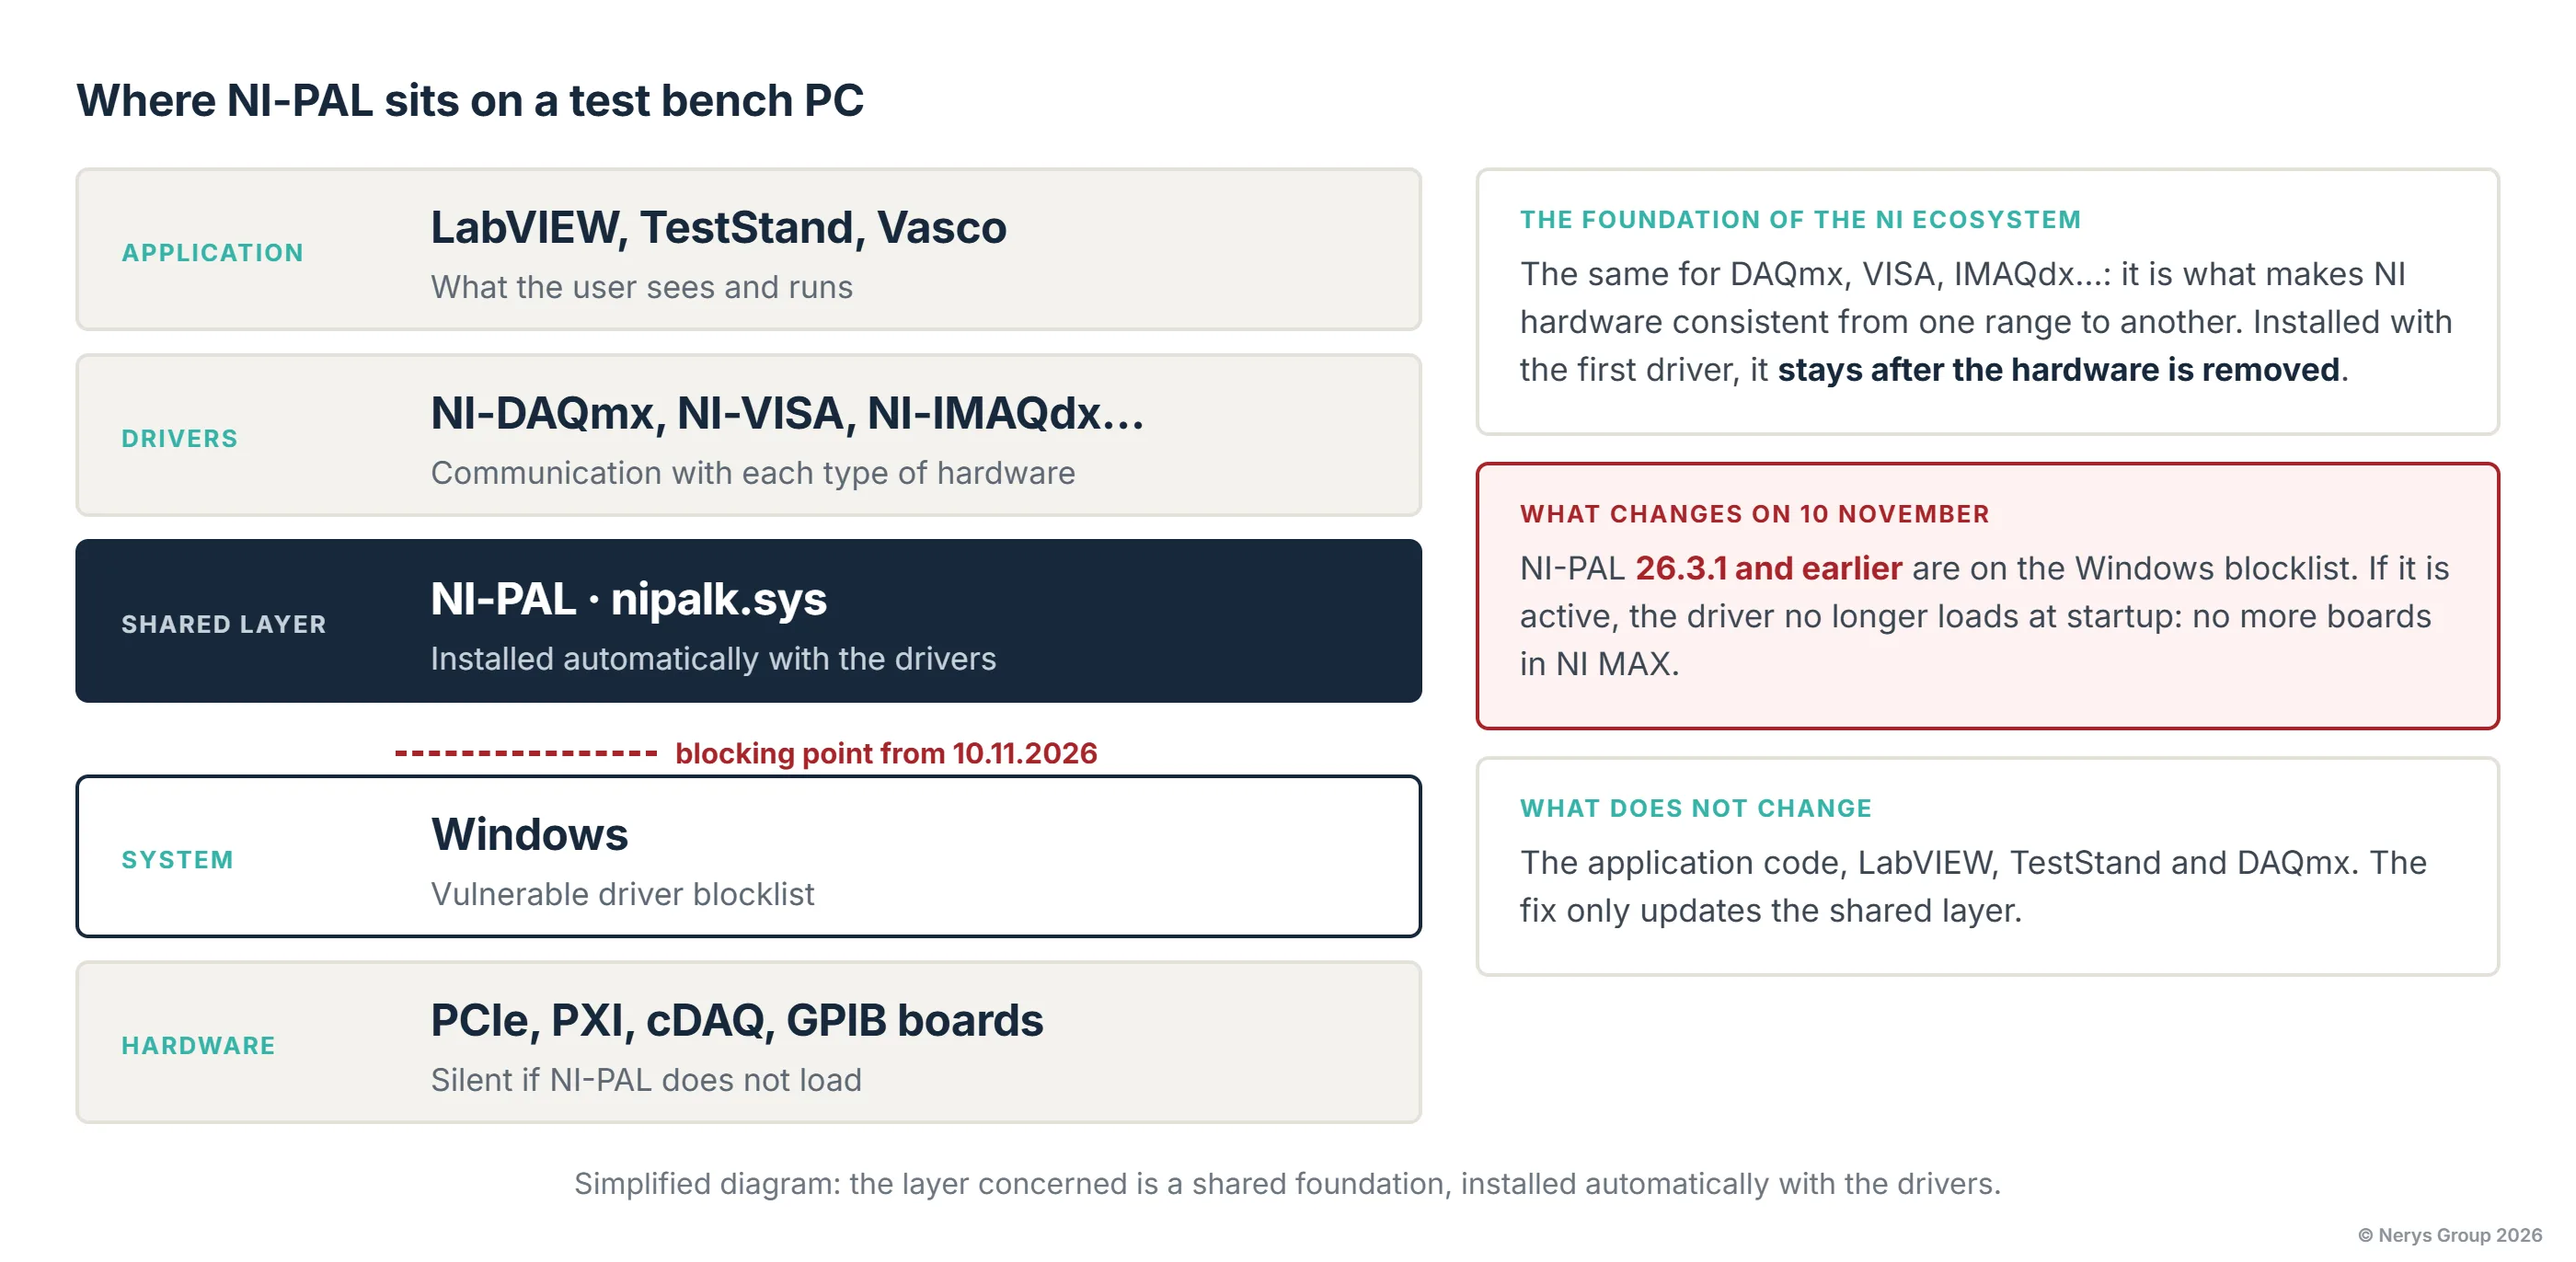
NI-PAL, short for Platform Abstraction Layer, is the common foundation of the NI Emerson drivers. It is what gives NI-DAQmx, NI-VISA, NI-IMAQdx and the others low-level access to the hardware and system resources, in the same way whatever the Windows version. It is also what makes the NI ecosystem strong: a PCIe board, a PXI chassis, a cDAQ and a GPIB instrument can all be controlled from the same application, with the same behaviour, because they rest on the same foundation. On a typical test bench, the stack looks like this: the LabVIEW or TestStand application runs the test, NI-DAQmx talks to the board, NI-PAL provides it with the system services it needs, and Windows arbitrates the whole thing. Users see the first layer, sometimes the second; the third is installed automatically with the drivers, and that is how it should be: a good foundation goes unnoticed as long as it works.
That is what makes the issue broader than it seems. A PC that once had an NI PCI board, a GPIB interface or just NI-VISA to control a multimeter has NI-PAL installed, and keeps it after the hardware has been removed. You do not need to develop in LabVIEW to be affected; installing an NI driver is enough. Note: our own software is in the same situation. Every Vasco installation includes a Windows PC, even when acquisition runs on a real-time target, and that PC carries NI drivers: it depends on NI-PAL exactly as an in-house LabVIEW application does. The criterion is not the name of the application, but the version of the installed component.
Where NI-PAL sits on your test bench.
What the security advisory says
NI has published an advisory for vulnerability CVE-2026-18485, which affects NI-PAL 26.3.1 and all earlier versions on Windows. It is a local privilege escalation: a user already logged on to the machine can obtain system rights they should not have. So it is not an open door from the Internet, and on a bench isolated from the network with two operator accounts, the pure security risk should be kept in perspective.
A word of caution, though: keeping it in perspective does not mean ignoring it. A test bench with access to the company network, or one that subcontractors log on to, is exactly the kind of PC where a local privilege escalation becomes a problem for someone other than the bench. Above all, the reason to deal with it now is not security. It is availability.
Why 10 November
Windows keeps a list of drivers considered vulnerable, and can block them from loading at startup. The affected versions of NI-PAL are now on it, with an announced effective date of 10 November 2026. On Windows 11, this protection is enabled by default. On Windows 10, it generally is not, unless the company's security policy has enabled it, which is increasingly common.
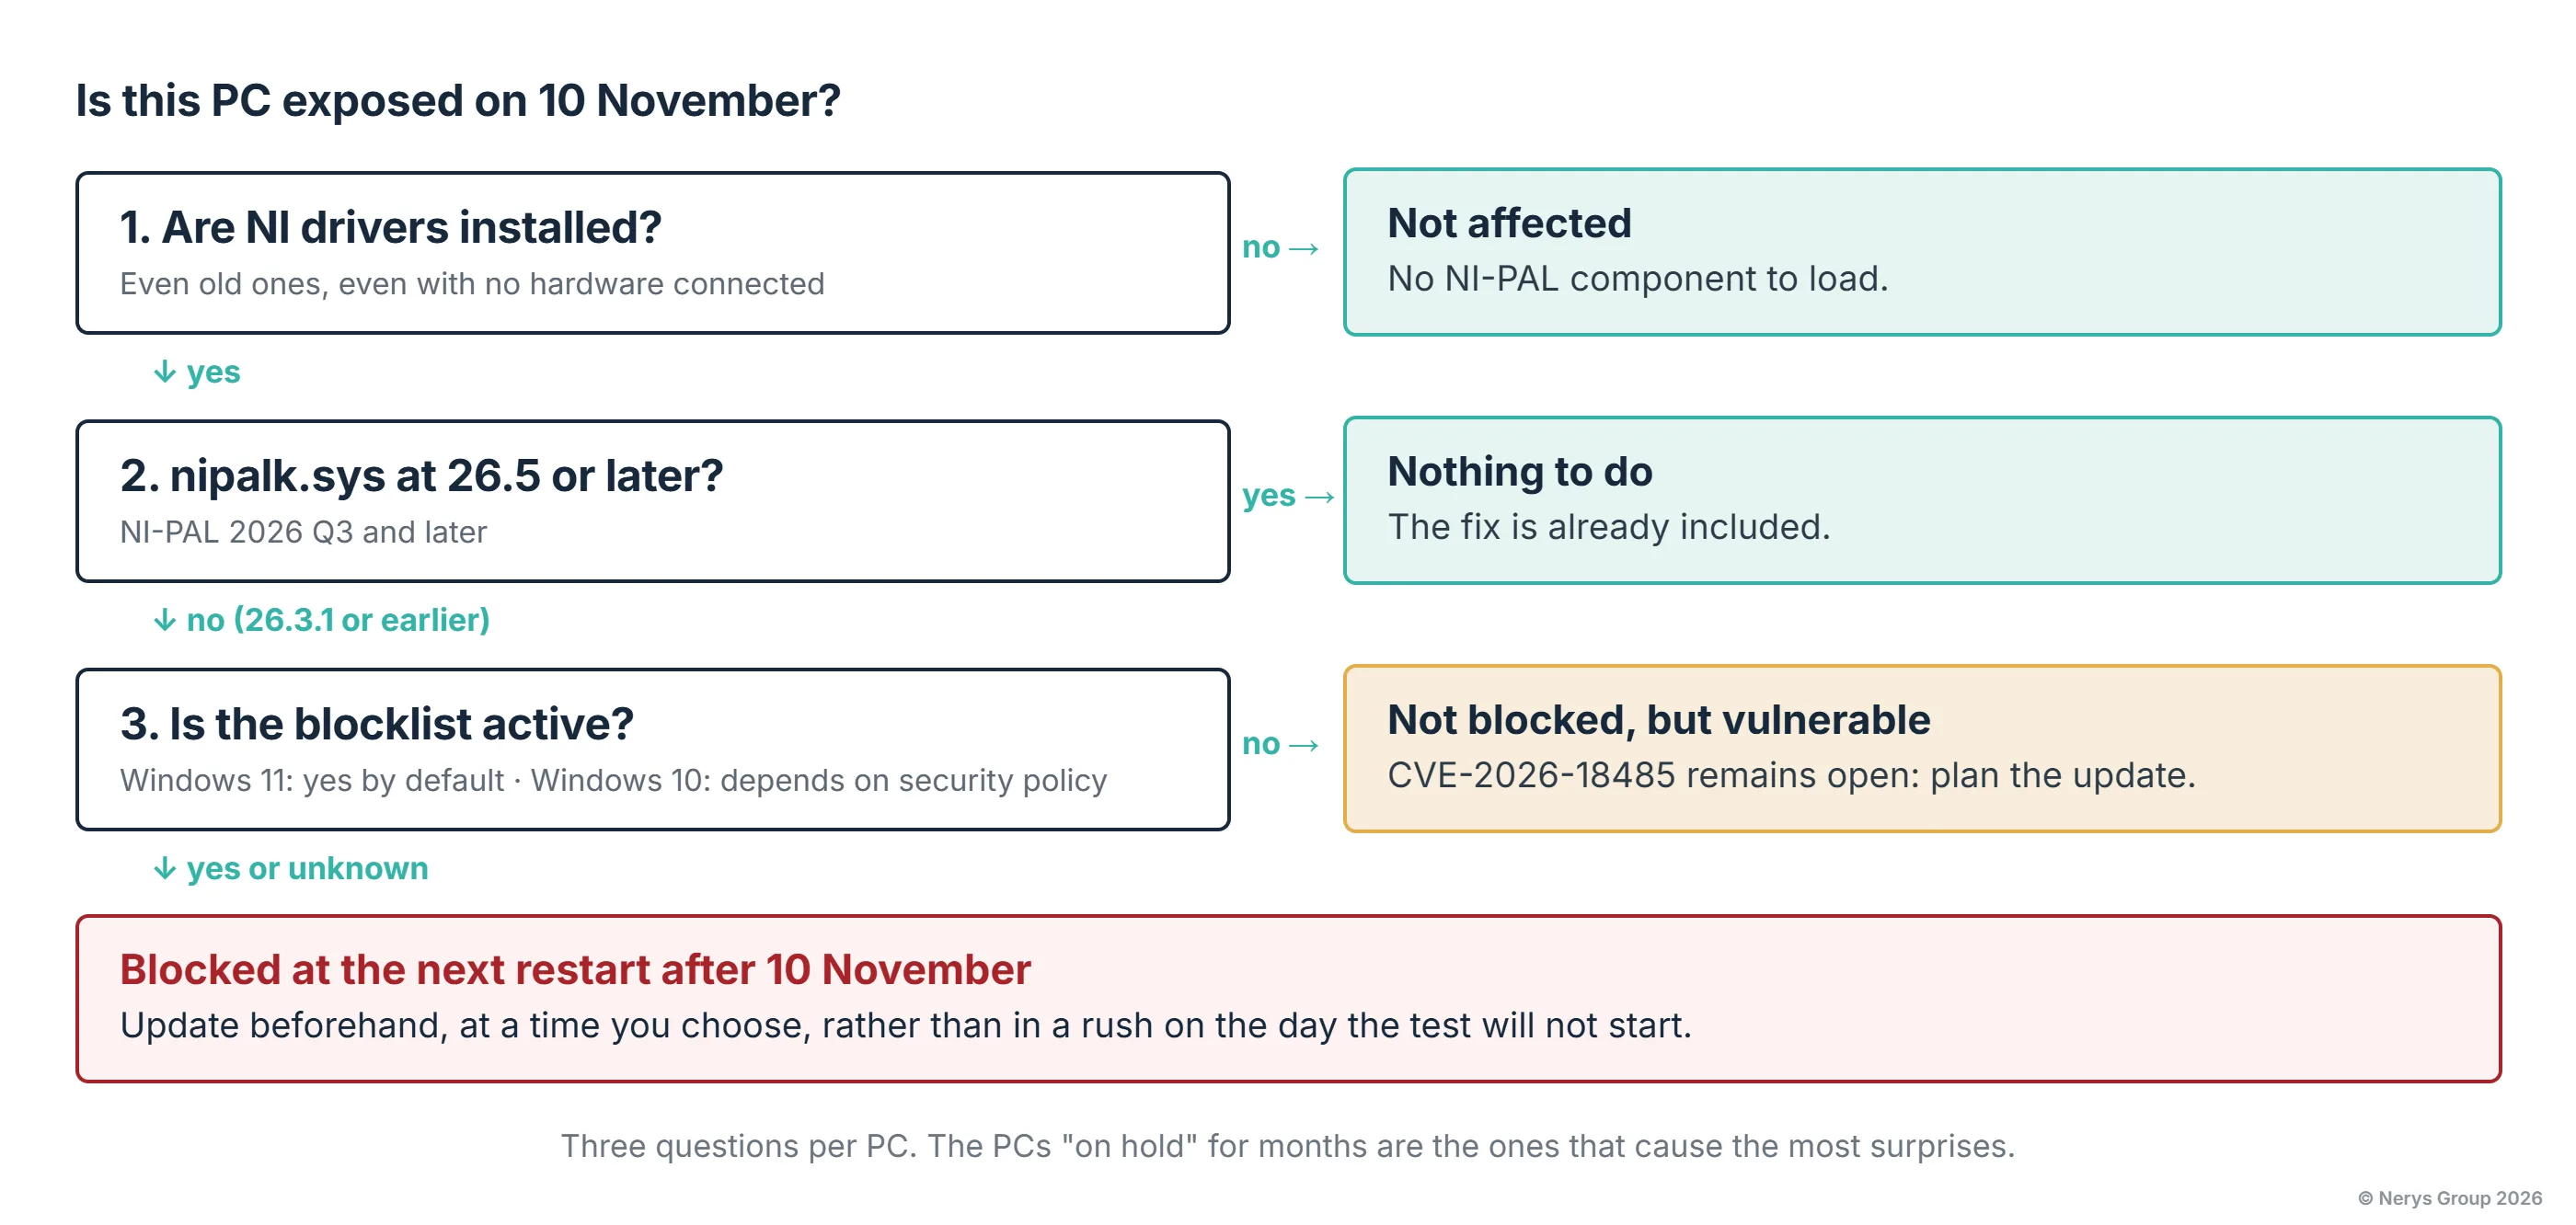
In practice, a bench whose NI-PAL is blocked at startup no longer recognises its boards in NI MAX, the application reports communication errors, and today's test does not happen. Nothing breaks, but nothing works. It is important to be precise about what this means: 10 November is not the date on which every test bench will stop. It is the date from which, on a system where the blocklist is active, the risk becomes real. So the question is not "are we affected?" but "which of our PCs are, and which will get through the date without noticing anything?".
Is this PC exposed on 10 November? Three questions per PC.
The three-minute check
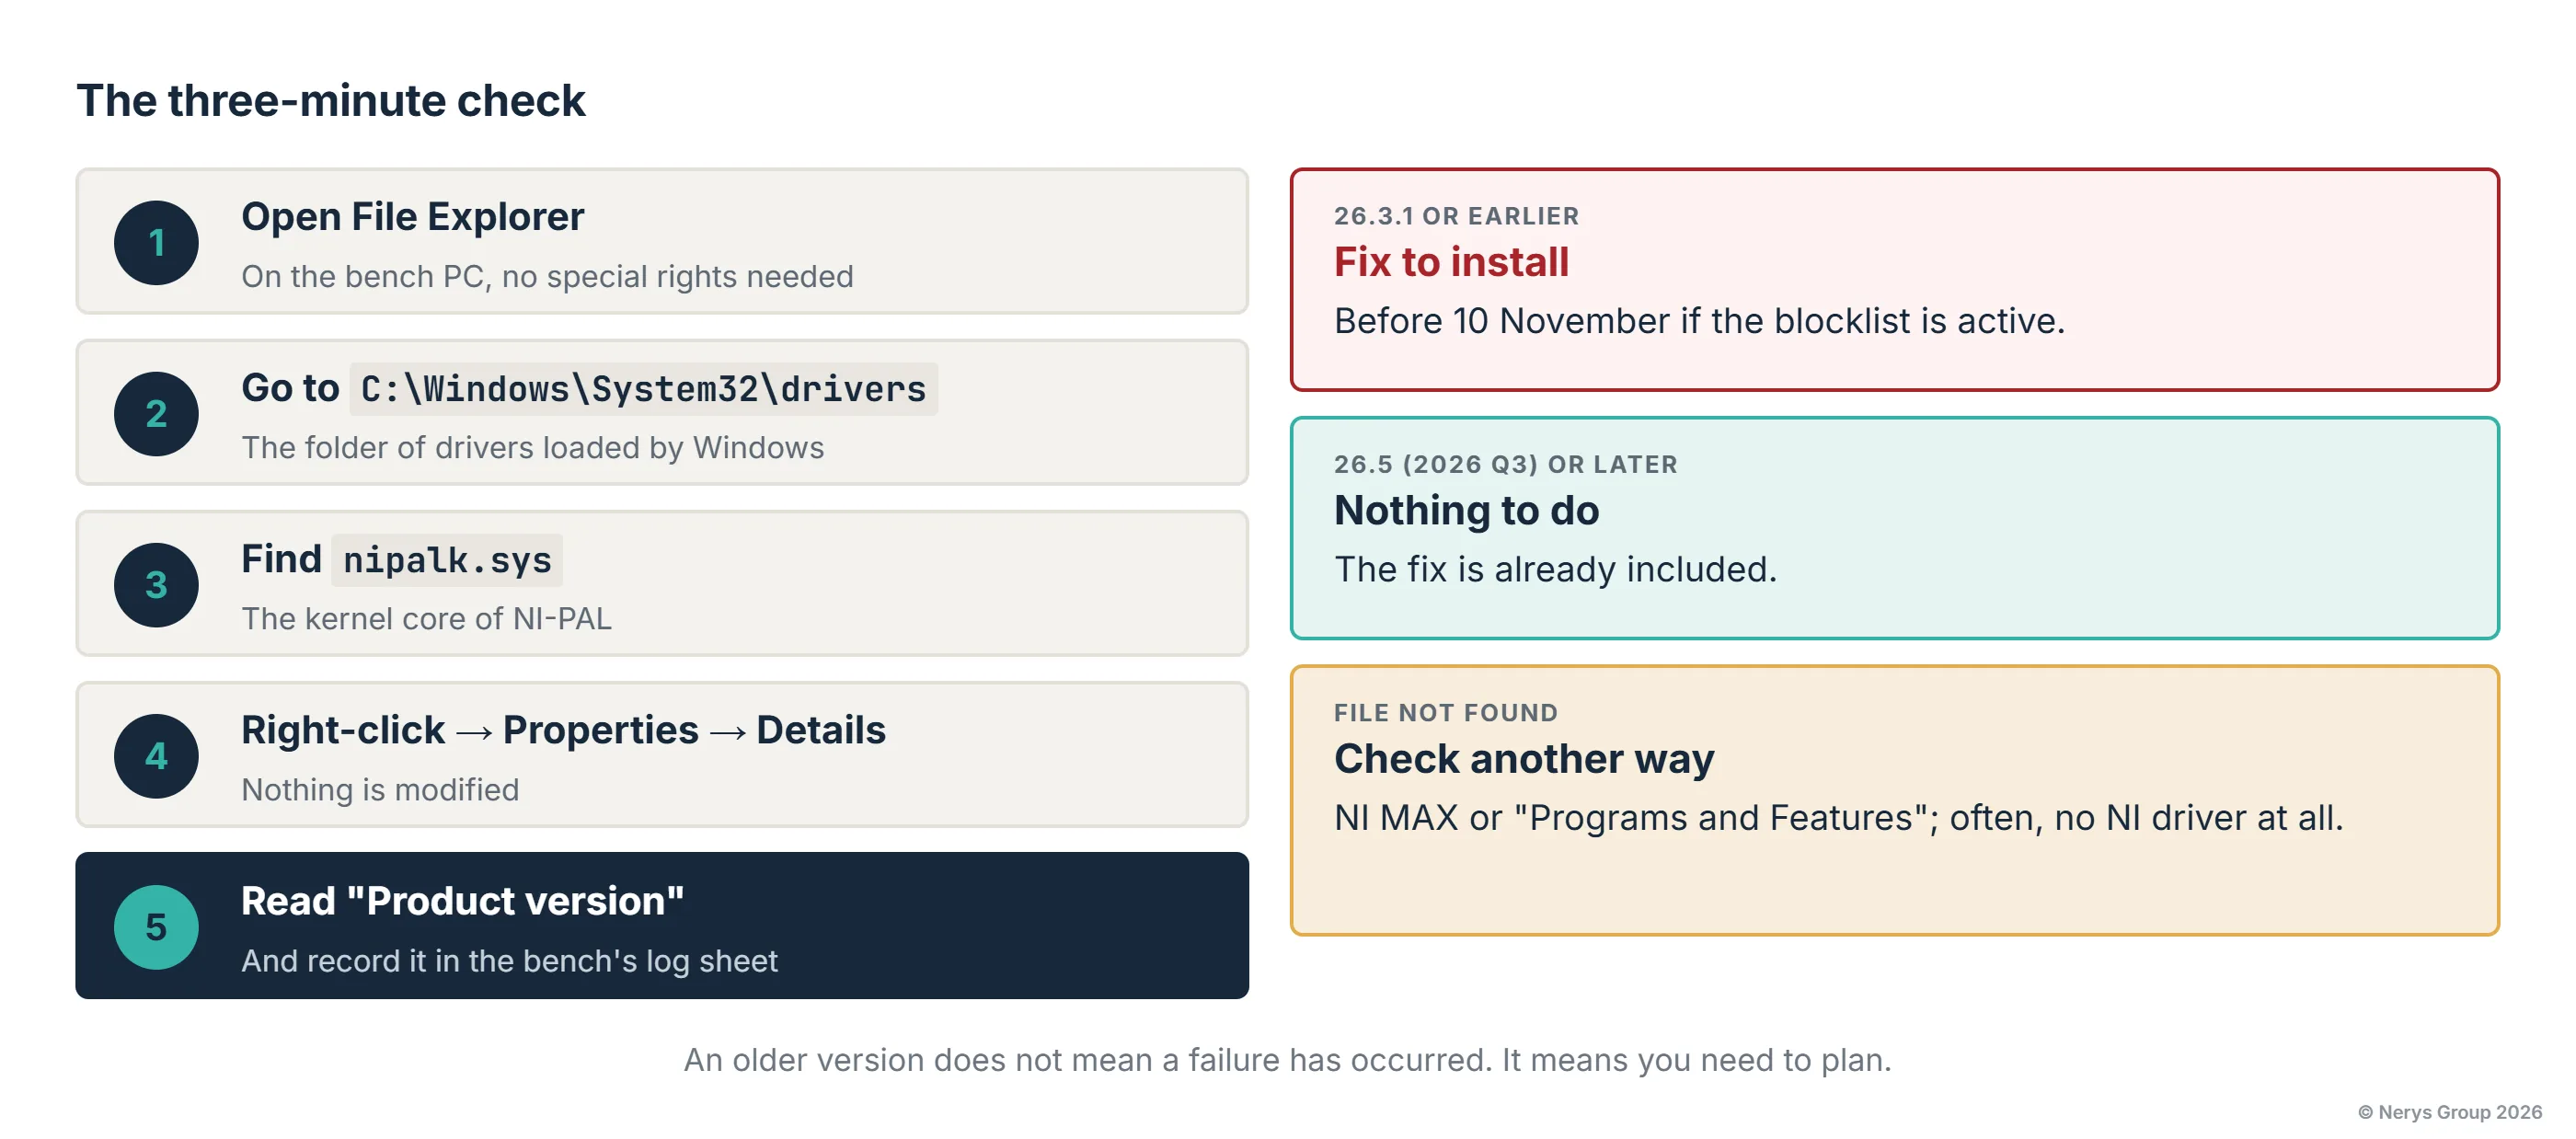
It requires no special rights and makes no change to the installation. On the bench PC, open File Explorer, go to C:\Windows\System32\drivers, find the file nipalk.sys, right-click, Properties, Details tab, and read the "Product version" field.
Three cases. Version 26.3.1 or earlier: the fix needs to be installed. Version 26.5 (NI-PAL 2026 Q3) or later: the fix is already included, nothing to do. File not found: either the PC has no NI drivers, or NI-PAL is installed differently; if in doubt, NI MAX or the "Programs and Features" panel will tell you. Note: an older version does not mean that something has gone wrong. It means you need to plan.
The three-minute check, and how to read the result.
We recommend doing this check on every PC connected to NI hardware, including those whose bench has been "on hold" for a year; they are the ones that get restarted on the day they are needed, and reveal the failure at that very moment.
A targeted update, and what it does not change
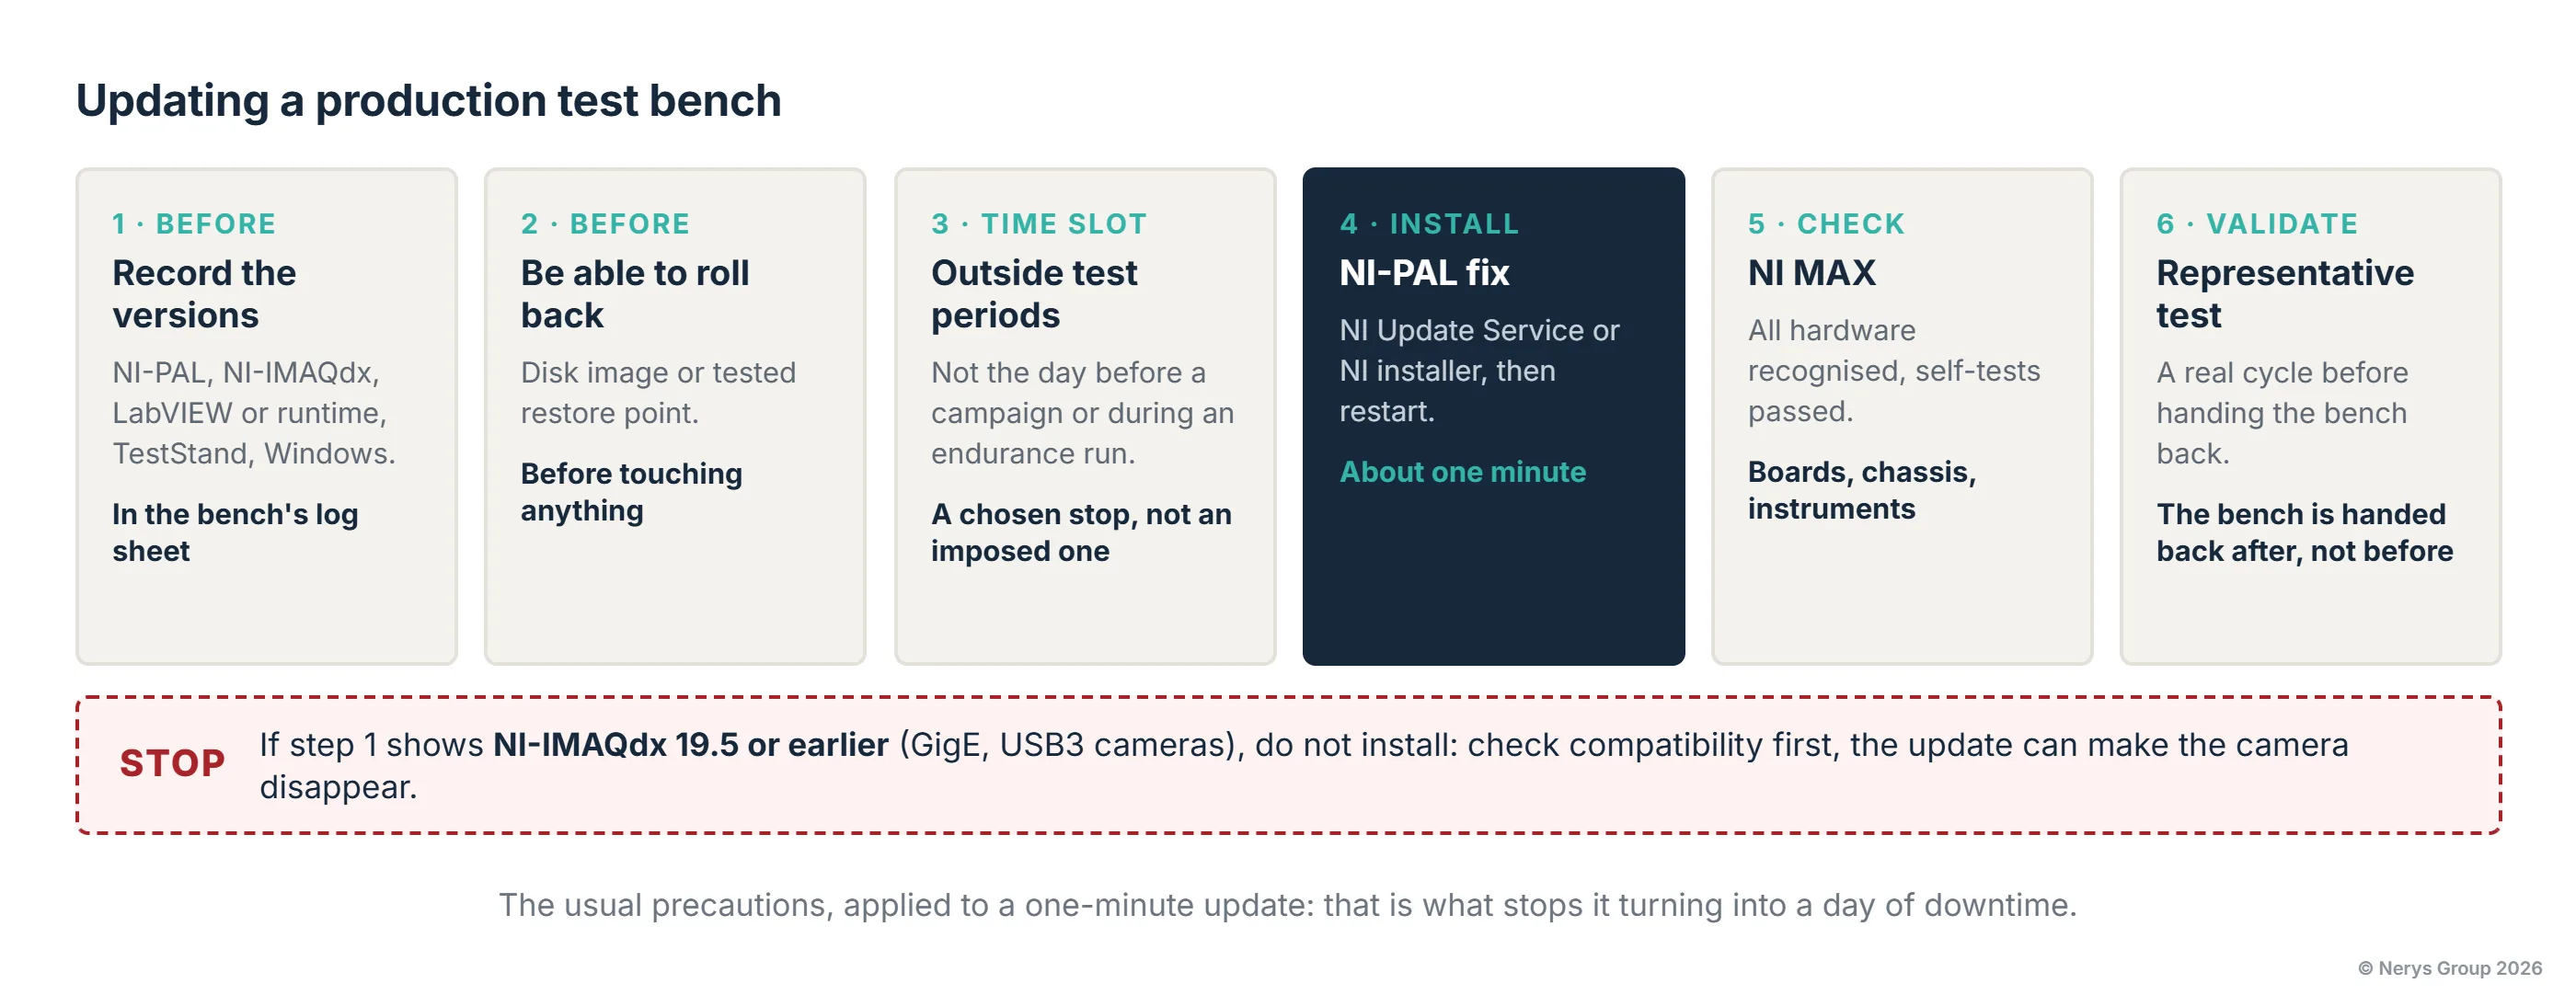
The good news is that NI delivers a fix for NI-PAL alone, not a full driver update. In compatible configurations, you do not need to change your version of LabVIEW, TestStand or DAQmx, nor touch the application code. NI states backward compatibility down to NI-PAL 17.0. Installation takes around one minute and requires a restart; it is done through NI Update Service or with the installer downloaded from the NI website.
On an office PC, it takes as long as a coffee. On a production test bench, we apply the same rule as for any change to the software environment: record the installed versions beforehand, have a way to roll back (disk image or restore point), work outside test periods, restart, check that all hardware is recognised in NI MAX, then run a representative test before handing the bench back. This is not paranoia; it is what ensures that a one-minute update stays a one-minute update, and not a day of downtime.
Updating a production test bench: six steps and one stop.
The camera trap
There is one exception, and it concerns benches we know well. NI has identified an incompatibility between NI-PAL 2026 Q3 and older versions of NI-IMAQdx, 19.5 and earlier. On a visual inspection bench that relies on a GigE or USB3 camera and a 2019 IMAQdx, applying the fix without prior analysis can make the camera disappear instead of the board. This is nothing exotic: a PC still on LabVIEW 2019 is very likely to have drivers of the same generation. It is the typical case where the "compatible" update is not, and where you need to look at the whole installation before clicking.
More generally, every older bench has one or two of these dependencies you need to know about before touching it: a third-party board driver, a Windows version frozen for a long-forgotten reason, a communication component with no recent equivalent. Listing them once, and keeping the list up to date, is what we call knowing your test bench.
Key takeaways
A test bench is more than its application and its boards. Between the two sits a stack of technical components, inconspicuous but essential, which also need maintaining. NI-PAL is an ordinary example: a security fix, a Windows blocklist, and a date. Three minutes of checking per PC tell you who is affected, and a one-minute update, surrounded by the usual precautions, settles the matter, except on benches with older cameras, where you need to analyse before acting.
Nothing revolutionary. But we would rather write it now than take the call on Monday 16 November.
If you would like an inventory of your affected PCs, or a hand planning the update on a production test bench: web@nerysgroup.com.
Not sure how many of your PCs are affected? We can carry out the inventory with you, then plan and validate the update bench by bench.
Thirty minutes, six industrial cases and a single question: how do you go from a measurement to a decision? At Mesures Solutions Expo, the stopwatch forced Luc Desruelle and Amaury Laurent to skim. Here is the long version, with the figures, the curves and the videos they had at hand, and what they chose not to show.
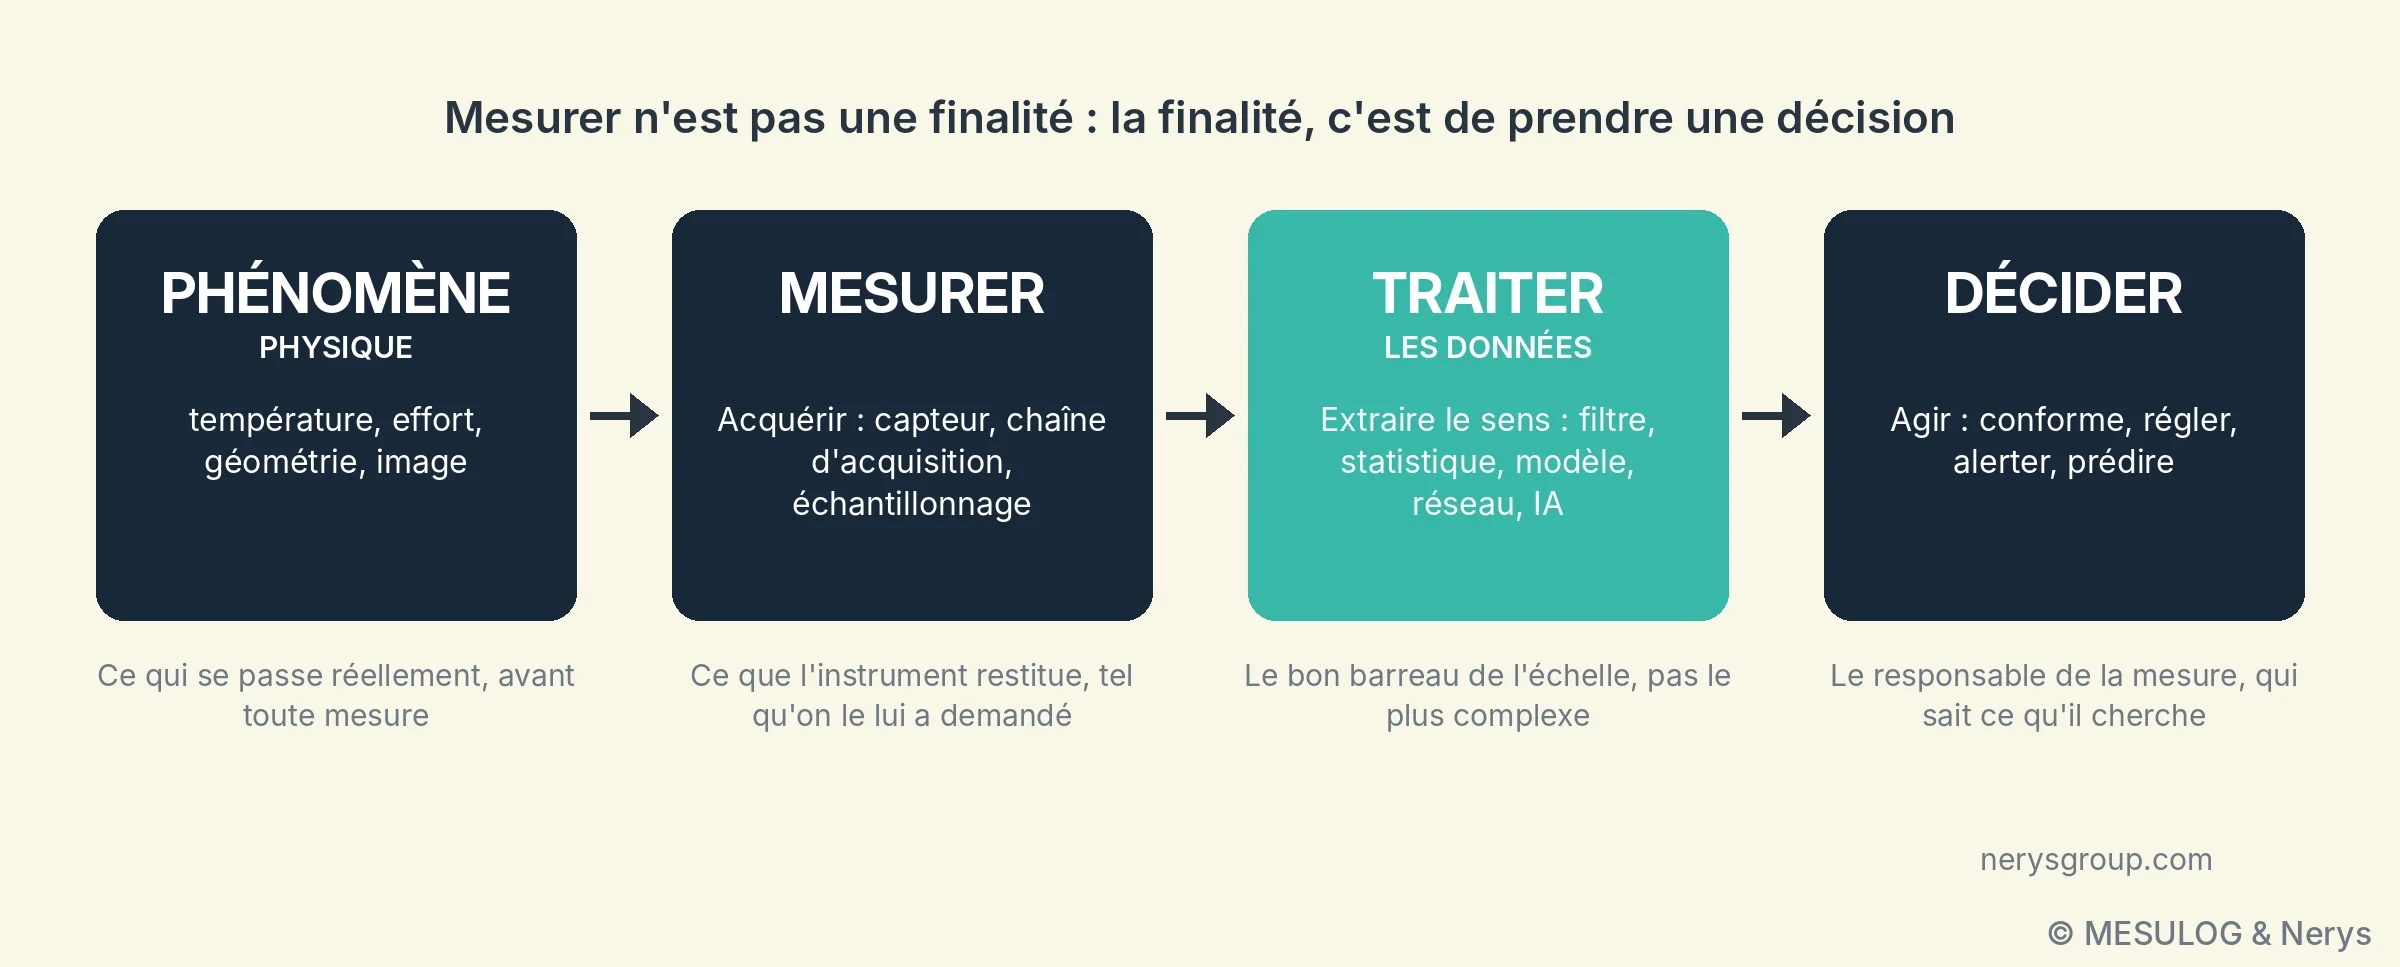
Measuring is not an end in itself. Nobody pays for a test bench to get numbers; they pay to decide: compliant or not, adjust or leave alone, alert or wait, and more and more often, predict. Between the physical quantity and that decision there is processing. That processing is what gives the measurement its value, and it is most often chosen out of habit.
On 15 October, in Lyon, Luc Desruelle, chairman of Mesulog and Nerys, and Amaury Laurent, head of embedded systems and R&D at Nerys, walked through six examples drawn from their projects, from the simplest to the most advanced: a moving average, a process capability, a linear regression on a point cloud, a neural-network camera, an embedded estimator on FPGA designed with Schneider Electric, and a generative AI handed a file of measurements. The common thread fitted in one sentence, repeated after each example: "it worked because we knew what we were looking for". The end of the workshop showed what happens when that is not the case.
Physical phenomenon, measurement, processing, decision. The choice of processing depends on the decision to be made, not on the fashionable tool.
1. A temperature: which value to keep?
The simplest case there is, built for the occasion in LabVIEW: the temperature of the Mesures Solutions Expo room, stable around 18 °C. A real measurement is never perfectly stable. It carries noise, and from time to time a frankly aberrant value: interference on the link, a contact that moves, an electromagnetic disturbance when a nearby motor starts.
The workshop's LabVIEW demonstration: raw measurement, smoothing by moving average, effect of the spikes, then moving median. Silent video, 70 s.
Mean or median: two hypotheses about the noise
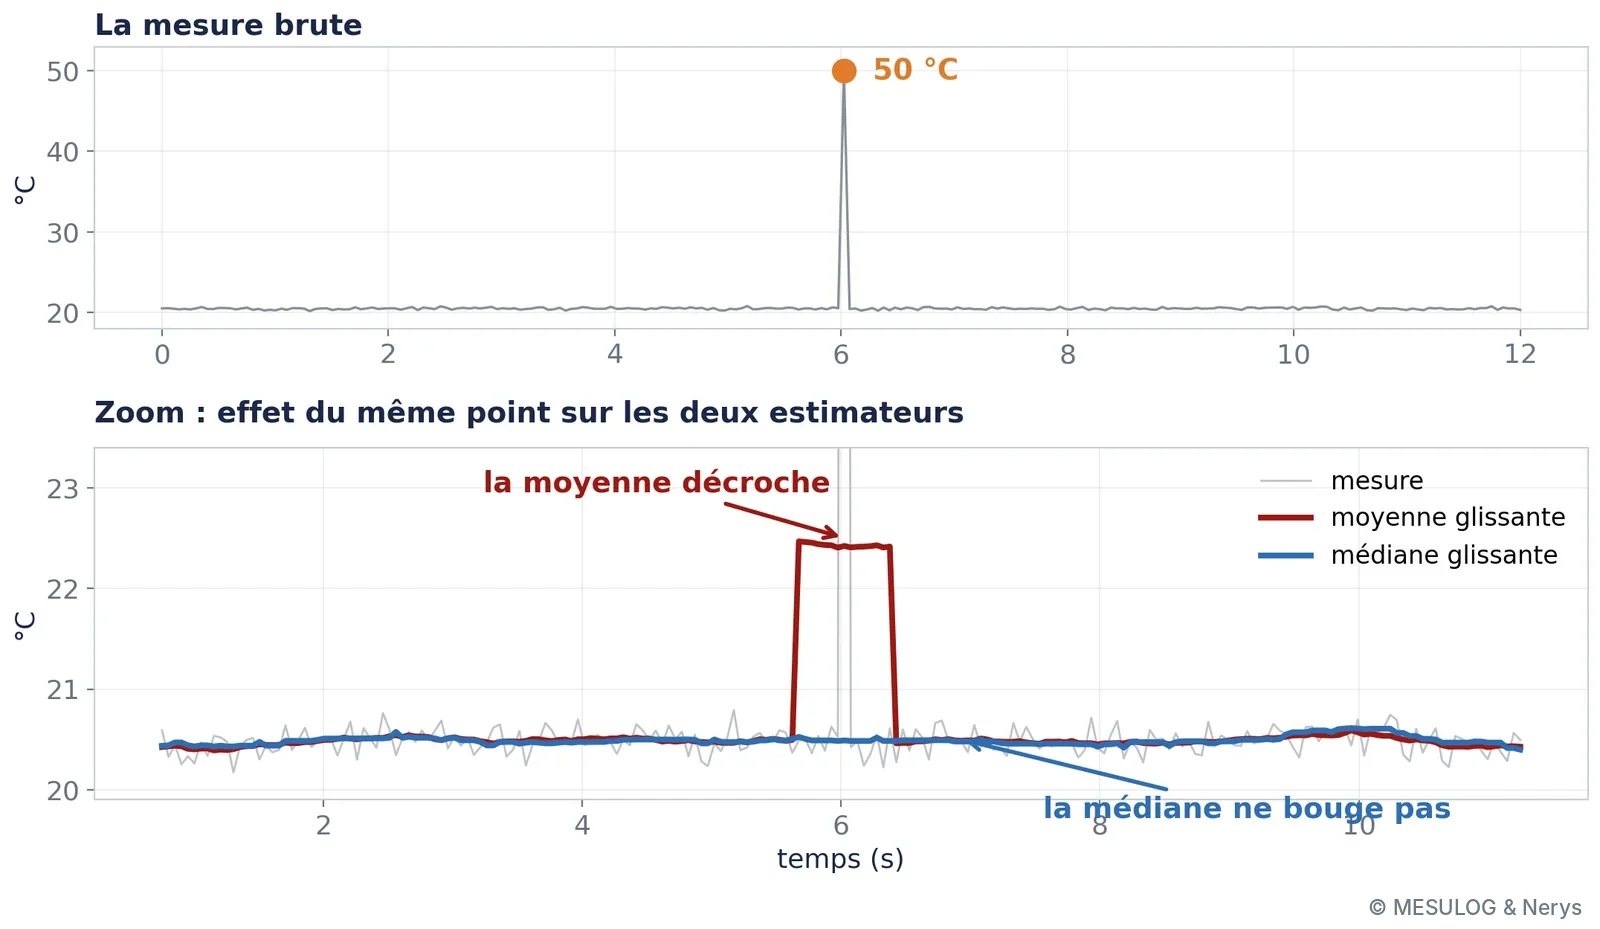
First reflex: smooth with a moving average. In the demonstration, the display goes from a raw measurement of 18.2 °C ± 3.7 °C to a processed value of 18.7 °C ± 0.4 °C: the noise is divided by nine, but the spikes have shifted the displayed value by half a degree. The mean smooths noise very well, but a single aberrant value pulls it towards itself. With a 25-point window, an isolated spike at 50 °C shifts the mean by about 1.3 °C, and it keeps shifting it for as long as it remains in the window, i.e. 25 samples. On the curve, the mean "steps away" at each spike.
The moving median, calculated over the same window, does not move: one aberrant point in 25 is sorted to the end of the list and has no influence on the central value. It remains correct as long as the majority of the points in the window are sound, that is, as long as the aberrant values remain a minority and isolated.
The same aberrant point throws the moving average off; the moving median does not move.
It is not that one is better than the other. They are two different hypotheses about the nature of the noise: the mean assumes symmetrical noise without extreme values, the median assumes that extreme values are rare and meaningless. Choosing one already means deciding something about the phenomenon and about the measurement chain.
The price of smoothing: delay
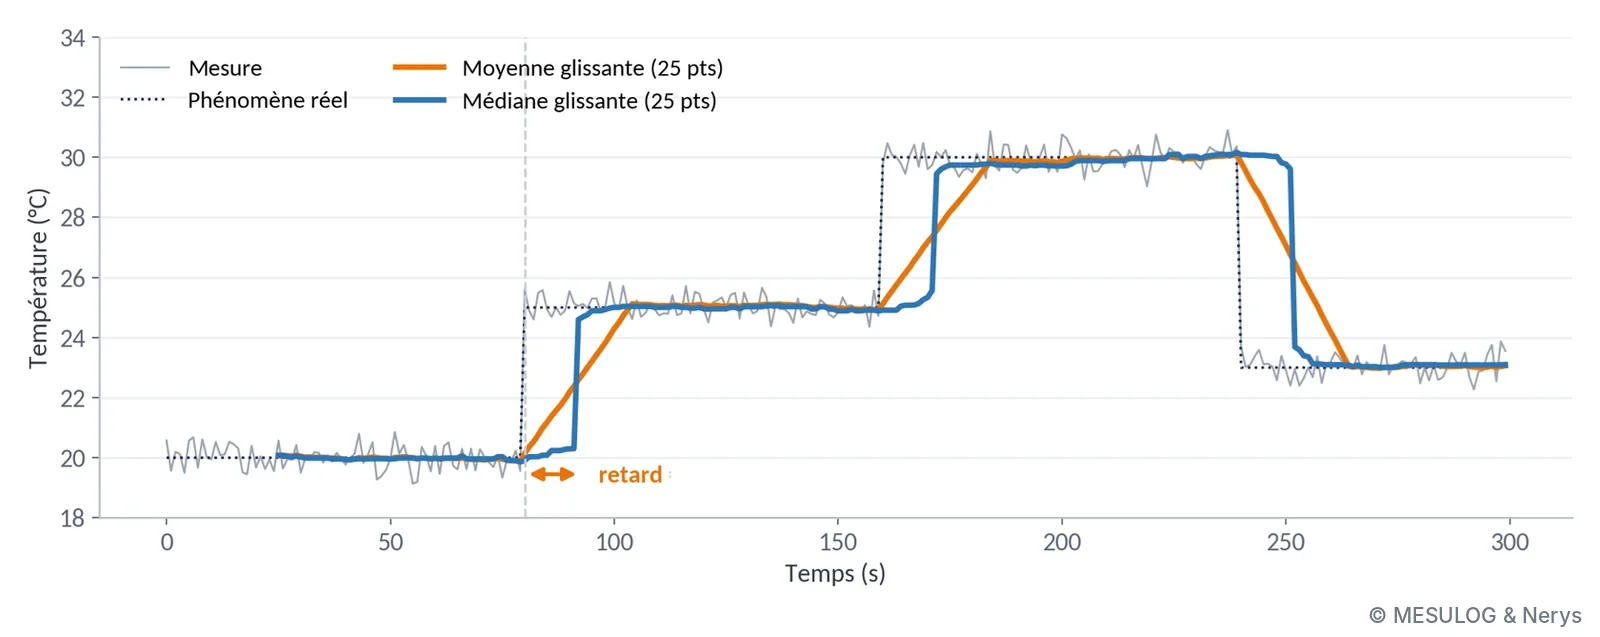
Then the physical phenomenon really changes: the temperature rises from 20 to 25 °C, then to 30 °C. The filter that protected against noise then becomes a handicap. A 25-point mean or median only follows a step after a dozen samples, half the window, and the mean follows it as a ramp while the median switches abruptly once the majority of the window has changed. The more you smooth, the later you react.
Two real temperature steps: both 25-point filters follow with a delay, each in its own way.
This is the basic trade-off of all processing, and it is not settled by technique. It is settled by answering a business question: how much time do we have to react, and how many false alarms are we prepared to accept? An endurance bench recording an oil temperature over three weeks and a safety loop that must trip within one second do not call for the same filter, even with the same sensor.
NB: the mean itself requires knowing what you are handling. The arithmetic mean of 350° and 10° is 180°, exactly the opposite of reality, whereas both directions are 10° from north. The calculation is right, the tool is right, and the result is wrong, because an angle is a circular quantity. The right method averages the sines and cosines, then recomposes the angle with a two-argument arctangent: you get 0°. The same precaution applies to a phase, a time of day or an encoder's angular position.
2. A spike or a break?
Same signal, one point stands out. Should it be removed or kept? If it is interference, remove it. If it is the first point of a new regime, or the beginning of a break, removing it means masking exactly what you were looking for. On a single sample, the two cases look identical. What happens afterwards is what distinguishes them, and that is what statistics allows you to decide cleanly.
The Gaussian law as a decision rule
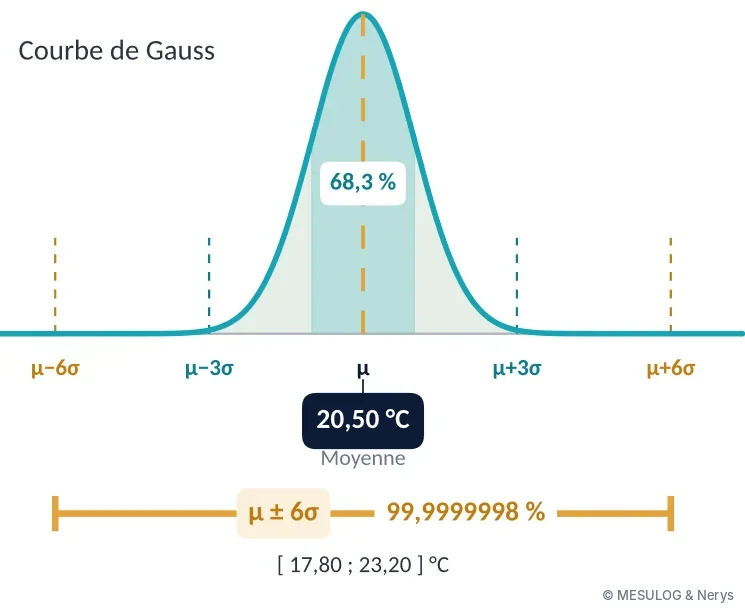
If the measurement noise results from many small independent effects, which is the case for thermal noise, quantisation noise and most disturbances in a well-designed chain, its distribution is Gaussian. Two numbers describe it entirely: the mean μ and the standard deviation σ. In the example presented, μ = 20.50 °C and σ = 0.45 °C.
μ ± 3σ covers 99.73% of measurements; μ ± 6σ covers 99.9999998%, here the window from 17.80 to 23.20 °C.
The μ ± 3σ window contains 99.73% of the measurements of a stable regime: one point in 370 falls outside, far too often to trigger a decision. The μ ± 6σ window contains 99.9999998%: about one point in 500 million. At one measurement per second, that is one false alarm every sixteen years. A point outside this window therefore has two plausible explanations: the system has changed, or the measurement is corrupted. In both cases, something must be done.
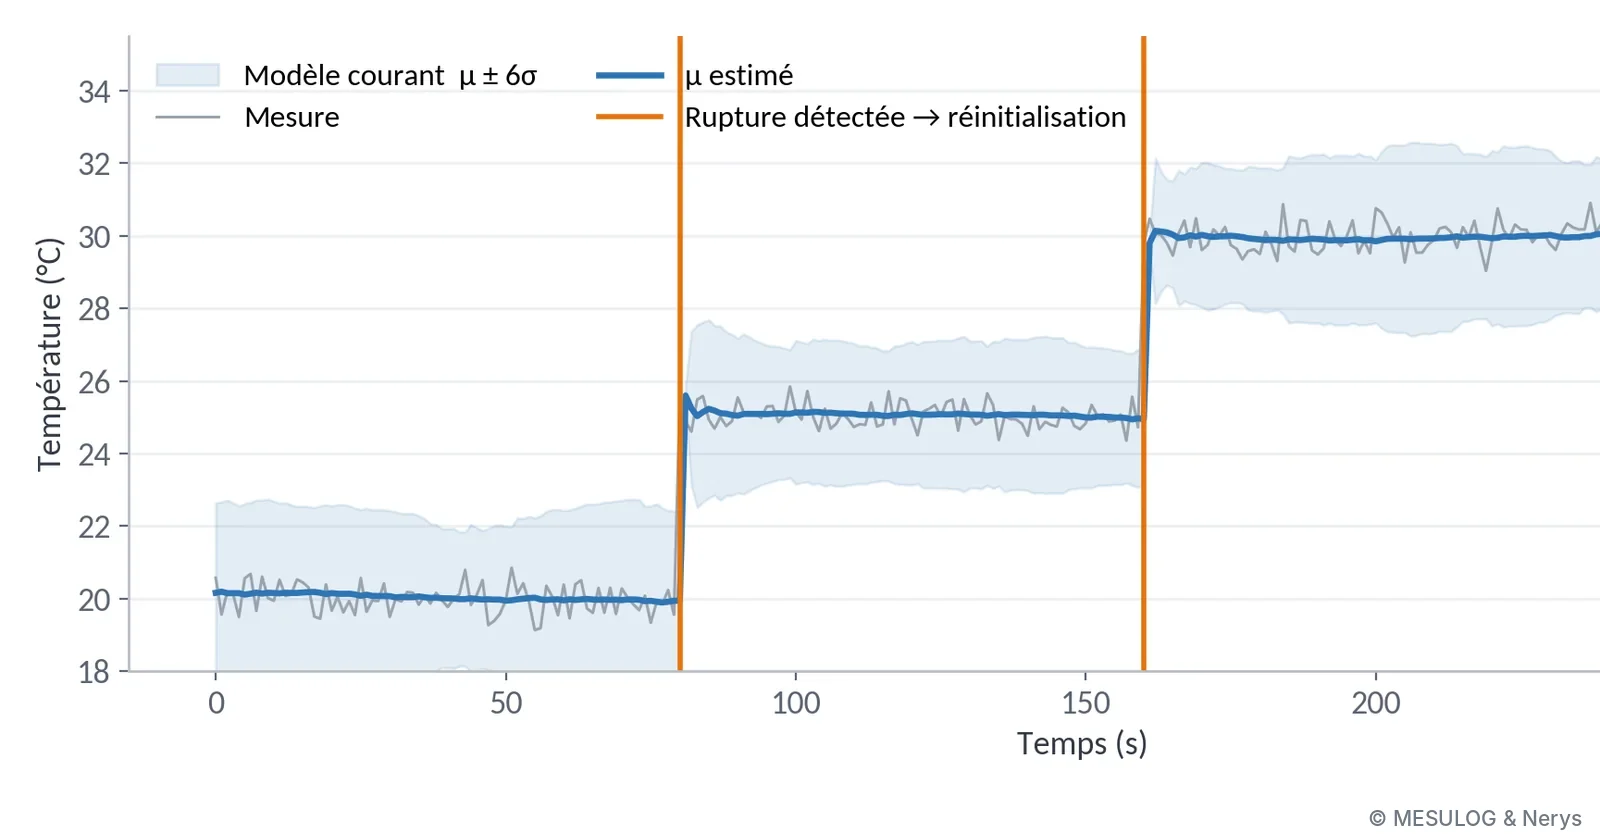
In the demonstration, the μ ± 6σ window runs from 17.80 to 23.20 °C. A point arrives at 25.5 °C, then a second, then a third: the break is detected, the filter is reset on the new regime instead of smoothing it for 25 samples, and the decision immediately follows the phenomenon.
At each change of regime, the |x − μ| > 6σ test detects the break and resets the model: neither delay nor smoothing of a real change.
A word of caution: a deviation greater than 6σ does not prove a break. It signals an observation incompatible with the chosen noise model, provided the assumptions of that model hold. If the noise is not Gaussian, if it contains regular impulses or a slow drift, the rule is worthless, and it is the analysis of the measurement chain that must say which noise model to use. We come back to the same sentence: it works because we know what we are looking for.
The same tools to drive the quality of a production line
These tools are used for more than filtering: they measure the quality of a process. On the production benches that Mesulog and Nerys develop with a TestStand test sequencer, each test step is a measurement, with its limits, its verdict and its context (serial number, station, operator). The WATS platform collects these results without re-entry: a reporter connected to TestStand sends each part's report at the end of the test to a centralised database, in the cloud or on the customer's servers. From there, the whole team analyses the same data, from the very first part.
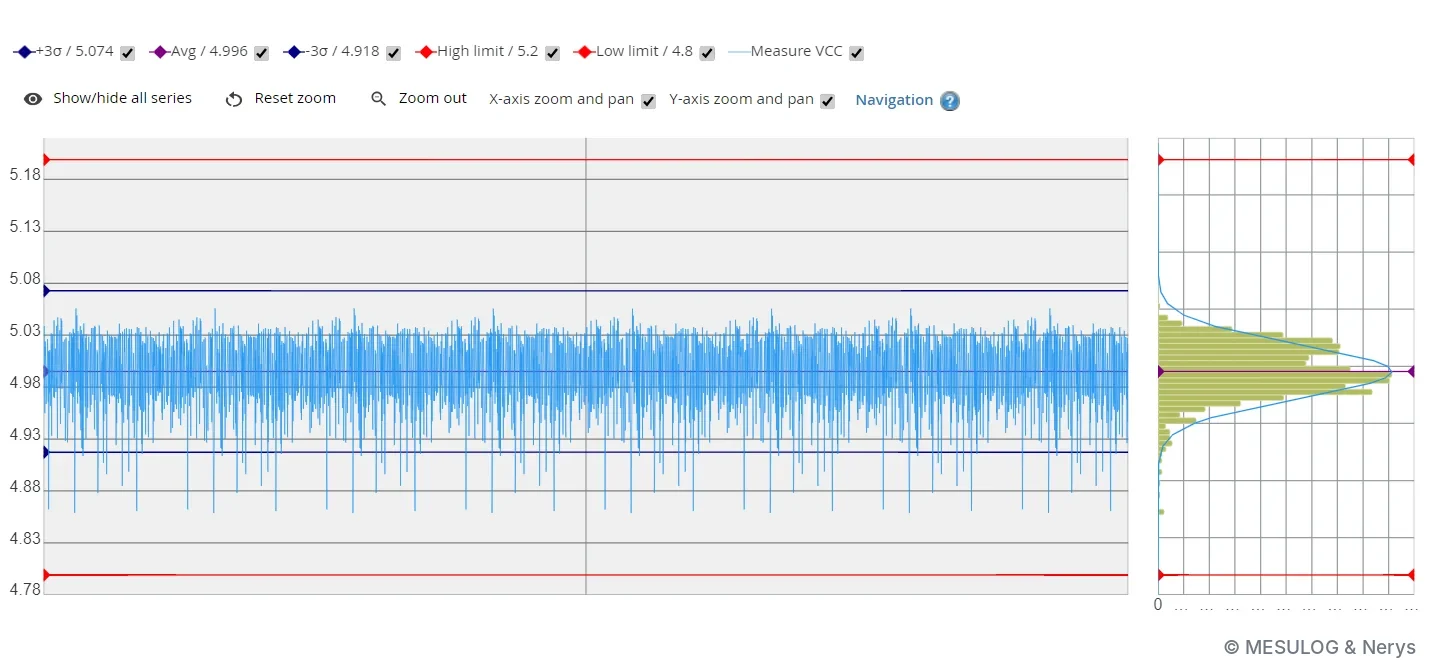
The example presented comes from a real bench: the "Measure VCC" test step, a nominal 5 V supply, with 9,862 measurements collected. The mean is 4.996 V: the process is centred. The standard deviation is about 0.026 V: the μ ± 3σ spread runs from 4.918 to 5.074 V, far from the specification limits set at 4.8 and 5.2 V.
9,862 measurements of a 5 V supply: trend, histogram and fitted Gaussian, 4.8 / 5.2 V limits, μ ± 3σ bounds.
"Far from the limits" is a feeling. Process capability turns it into a figure comparable from one bench to another: Cpk = min[(USL − μ) / 3σ ; (μ − LSL) / 3σ], where USL and LSL are the upper and lower limits. Here, (5.2 − 4.996) / 0.078 ≈ 2.6 on the high side and (4.996 − 4.8) / 0.078 ≈ 2.5 on the low side: the Cpk is about 2.5, where the usual target in production is 1.33. A Cpk below 1 means that part of the production will fall outside the limits even if the process does not drift; a Cpk of 2.5 leaves a comfortable margin, and allows, for example, a discussion about reducing inspection.
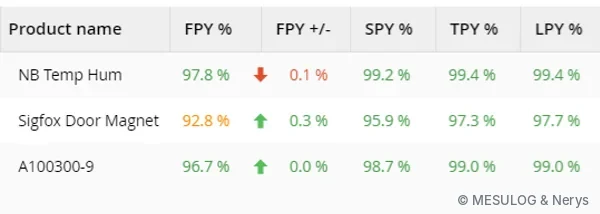
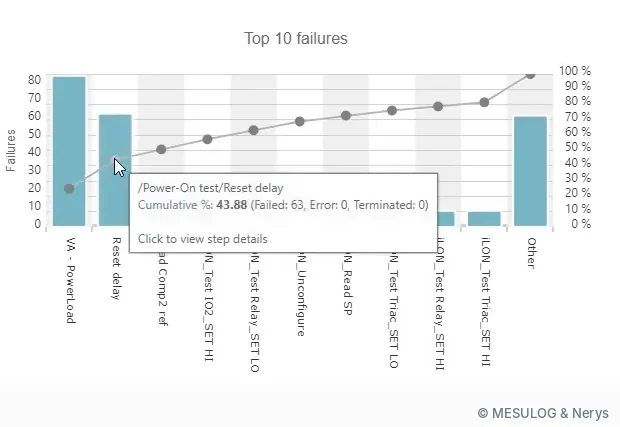
Yield indicators complete the picture. FPY (first pass yield) is the rate of compliant products on the first pass; SPY, TPY and LPY track the second, third and last passes. The gap between FPY and LPY measures what retests cost. The Pareto of the ten most frequently failing test steps says where the defects are concentrated, that of the ten lowest Cpks says where to act first, and a CUSUM chart, which accumulates deviations from the target, signals a slow drift before the first failure.
Yields per product: FPY, SPY, TPY, LPY.The ten most frequently failing test steps, as a Pareto.
WATS has recently offered two extensions that fall under AI: an integrated assistant that suggests groupings and root causes (by operator, by batch), and an MCP connector that lets an assistant such as Claude or ChatGPT query the test database directly in natural language: "what made the FPY drop last week?", "which stations generate the most retests?". The question is still asked by someone who knows what an FPY is and why it dropped; the tool simply searches faster.
3. The thickness of a slab: linear regression
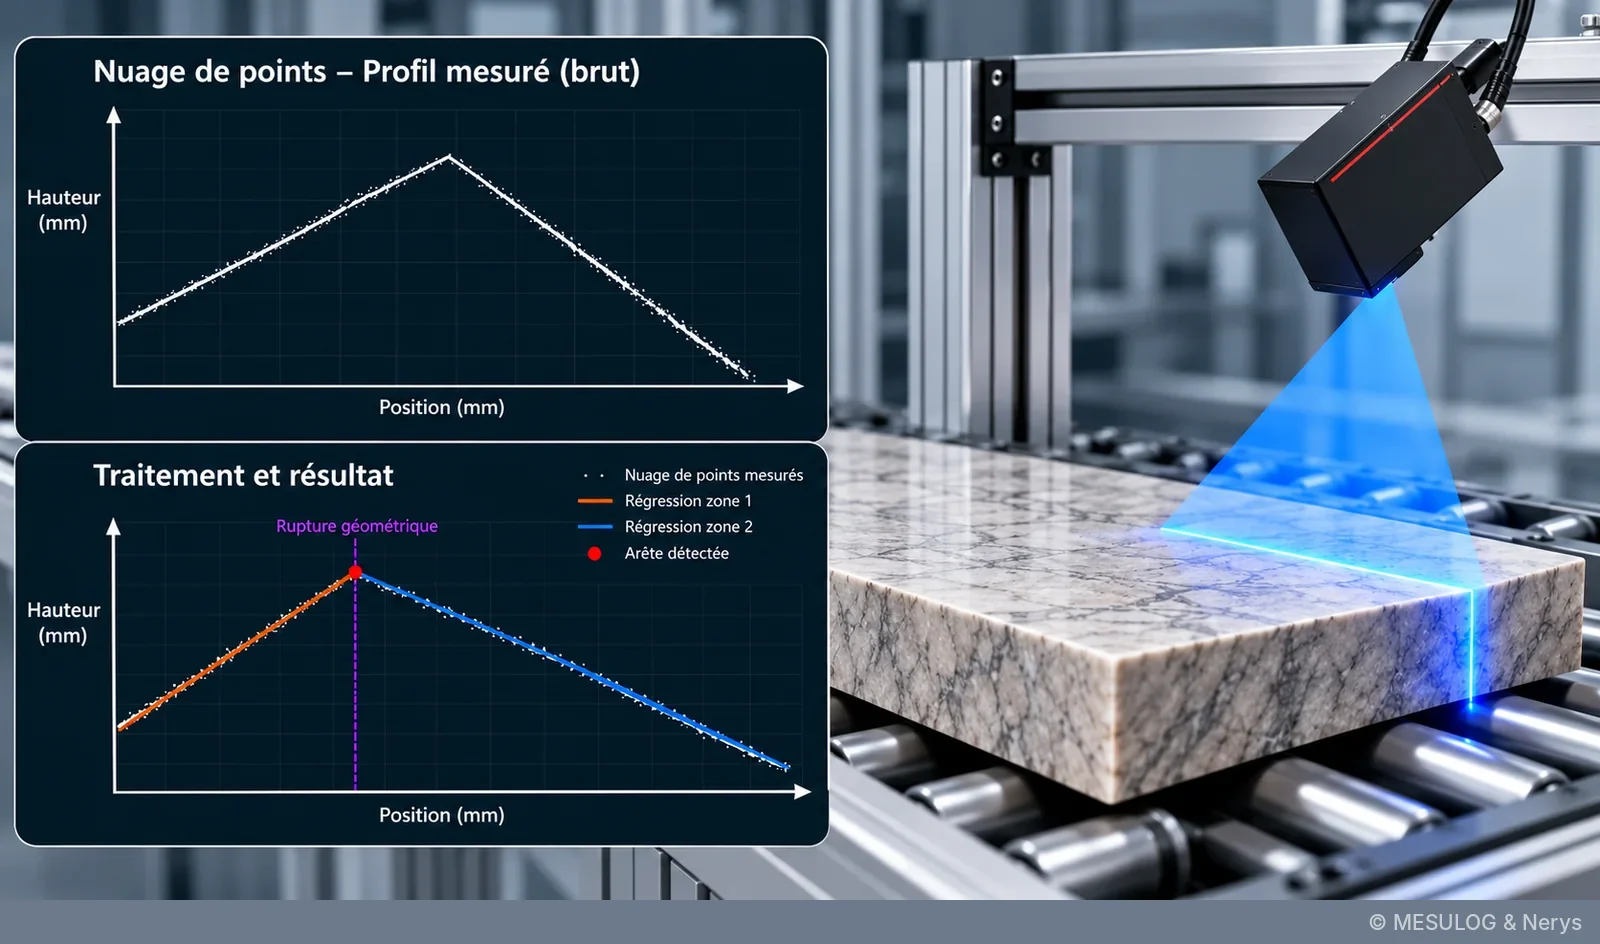
Third example, a dimensional measurement: the thickness of a marble slab on a conveyor, with a nominal dimension of 20.0 mm. A 2D laser profilometer (a Keyence, in the real set-up) projects a laser line onto the edge of the slab and returns, for each profile, a point cloud of height versus position. A thickness, with its uncertainty, has to be extracted from it.
Simplified illustration, not representative of the real set-up: the raw profile, then the split into upper zone and side zone.
The cloud is imperfect: measurement noise, missing points on shiny or steeply inclined surfaces, a rounded edge that does not give a sharp corner. Taking the highest point and the lowest point does not give a thickness, but the height of the most prominent grain.
The method, in three steps
First step, split the profile into zones: the upper zone, almost horizontal, and the side zone, almost vertical. The boundary is found by looking for the geometric break, the place where the local slope changes abruptly. Second step, model the upper surface by a straight line, fitted by the least-squares method: the line that minimises the sum of the squared vertical deviations between the points and the model. With a few hundred points, the noise of each point averages out, and the line is far more accurate than any isolated point. Third step, calculate the thickness by orthogonal projection of the extreme point of the side face onto this line. The spread of the fit residuals gives, in passing, an estimate of the measurement uncertainty.
The principle, animated (55 s).
Nothing revolutionary: the least-squares method was published by Legendre in 1805. It works because the geometry of the part is known: the upper surface is flat, the edge is roughly perpendicular. On a curved part, the same line would give a wrong result, with larger residuals but a reassuring-looking uncertainty if nobody looks at their shape. Here again, it is knowledge of the measured object that chooses the model.
A linear regression is a neuron
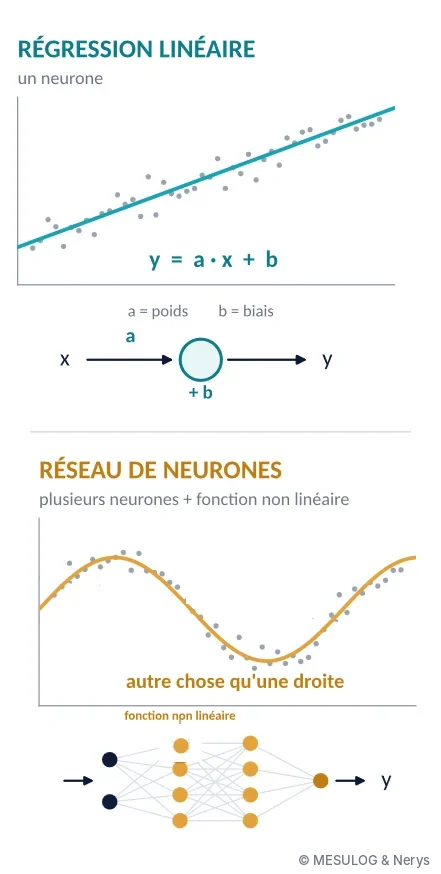
This example also served as a bridge to what followed. A linear regression, y = a·x + b, is a neuron: the coefficient a is the weight, the intercept b is the bias, and the least-squares fit is its training. Everyone in the room had been doing it for years without knowing.
A neuron: one weight, one bias. A network: many neurons and a non-linear function.
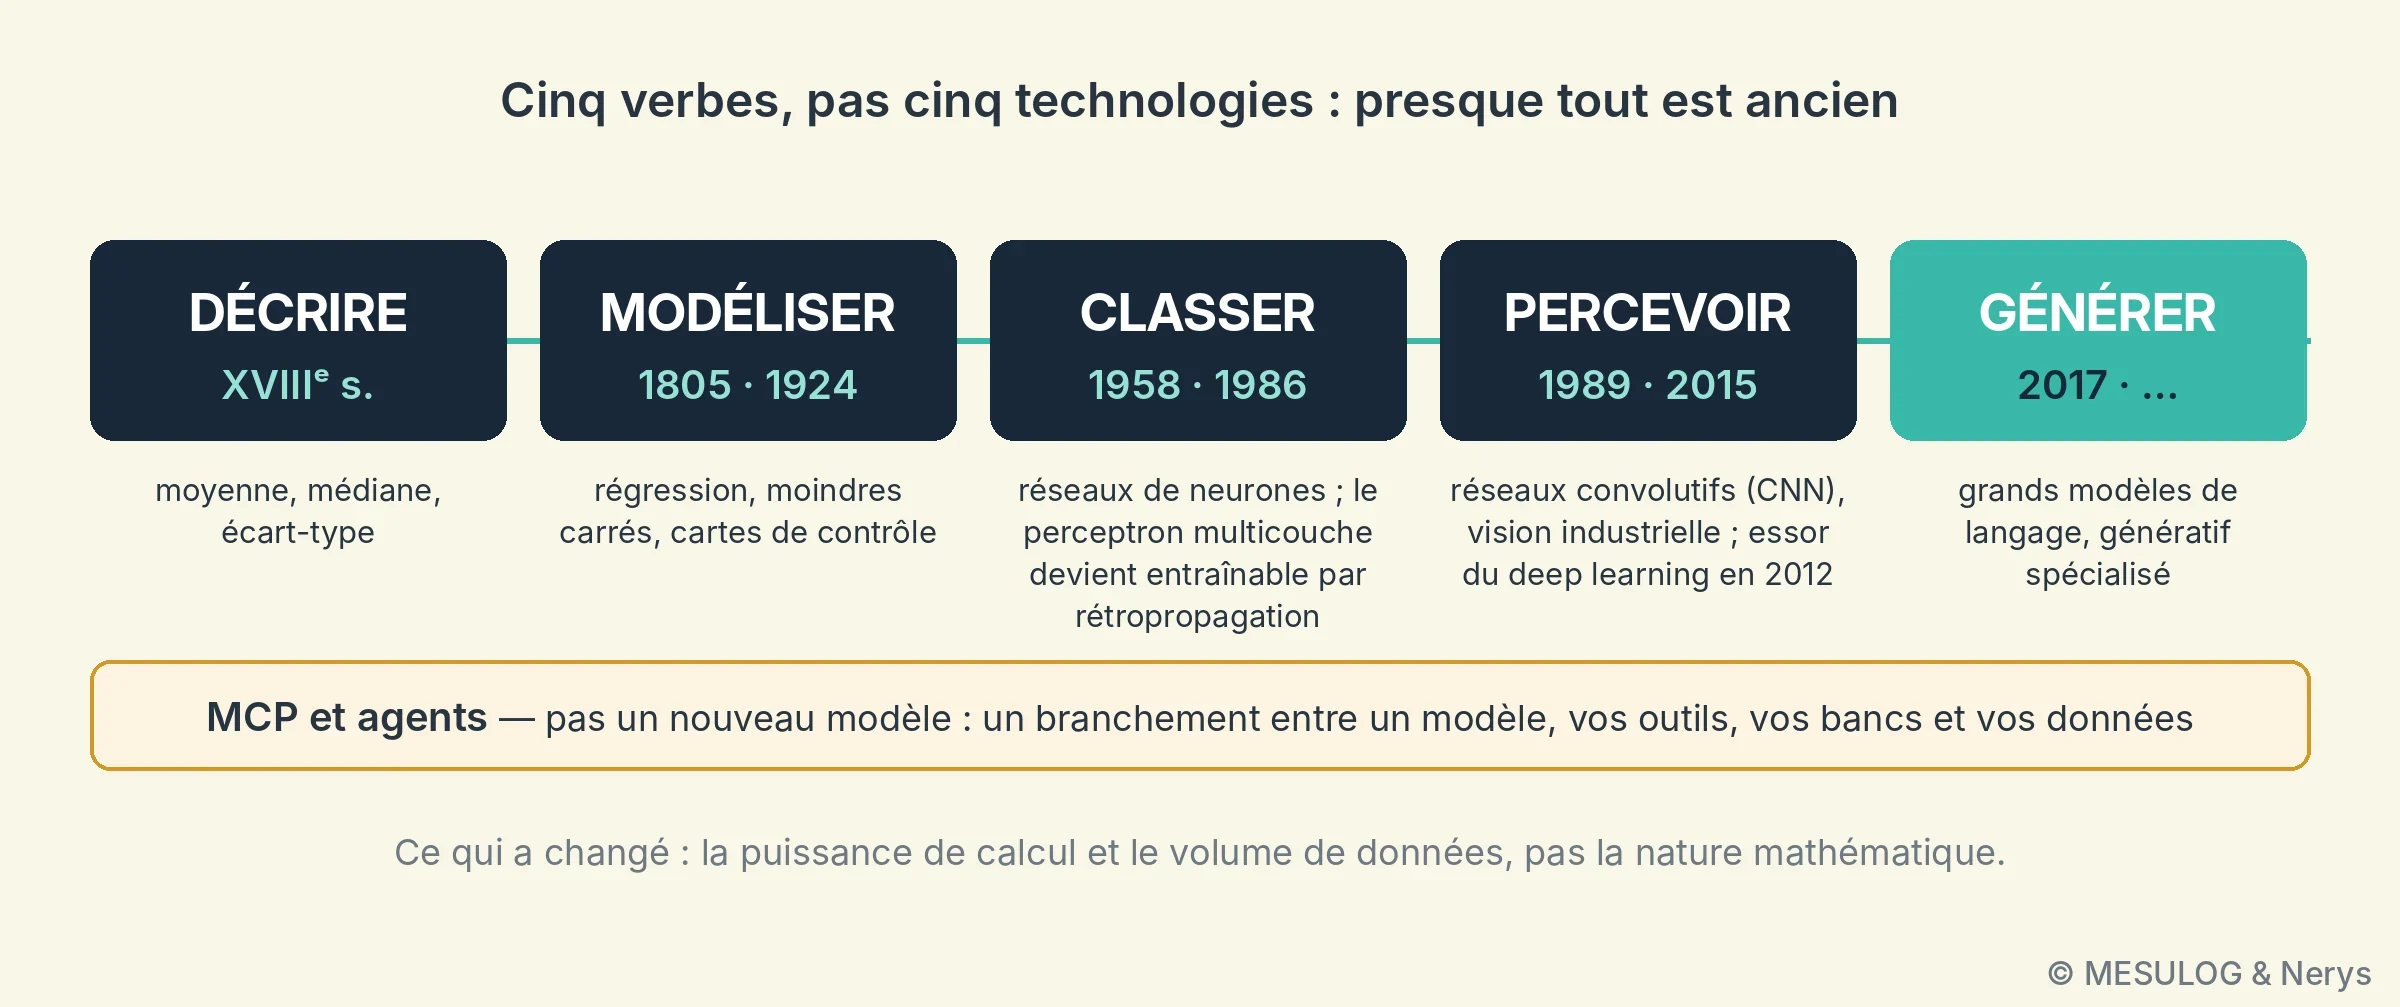
A neural network combines many of these elements, and inserts between them a non-linear function that allows it to represent something other than a straight line. Almost all the methods we now call artificial intelligence are old: regression dates from 1805, control charts from 1924, the perceptron from 1958, backpropagation, which makes multilayer networks trainable, from 1986, convolutional networks from 1989. What has changed is computing power and the volume of available data, not the mathematical nature of the tools.
Five verbs that describe what the engineer wants to do, not what the tool is.
The speakers presented this evolution as five verbs rather than five technologies: describe, model, classify, perceive, generate. Classifying is what decides good or bad at the end of the bench; it has been running at most manufacturers for twenty years, and nobody called it AI. The boundary is fairly arbitrary. As for MCP (Model Context Protocol), it is not a family of models but a connection protocol between a model and your tools, your benches and your data: a plug, not an extra brain.
4. Recognising dice: industrial vision with a neural network
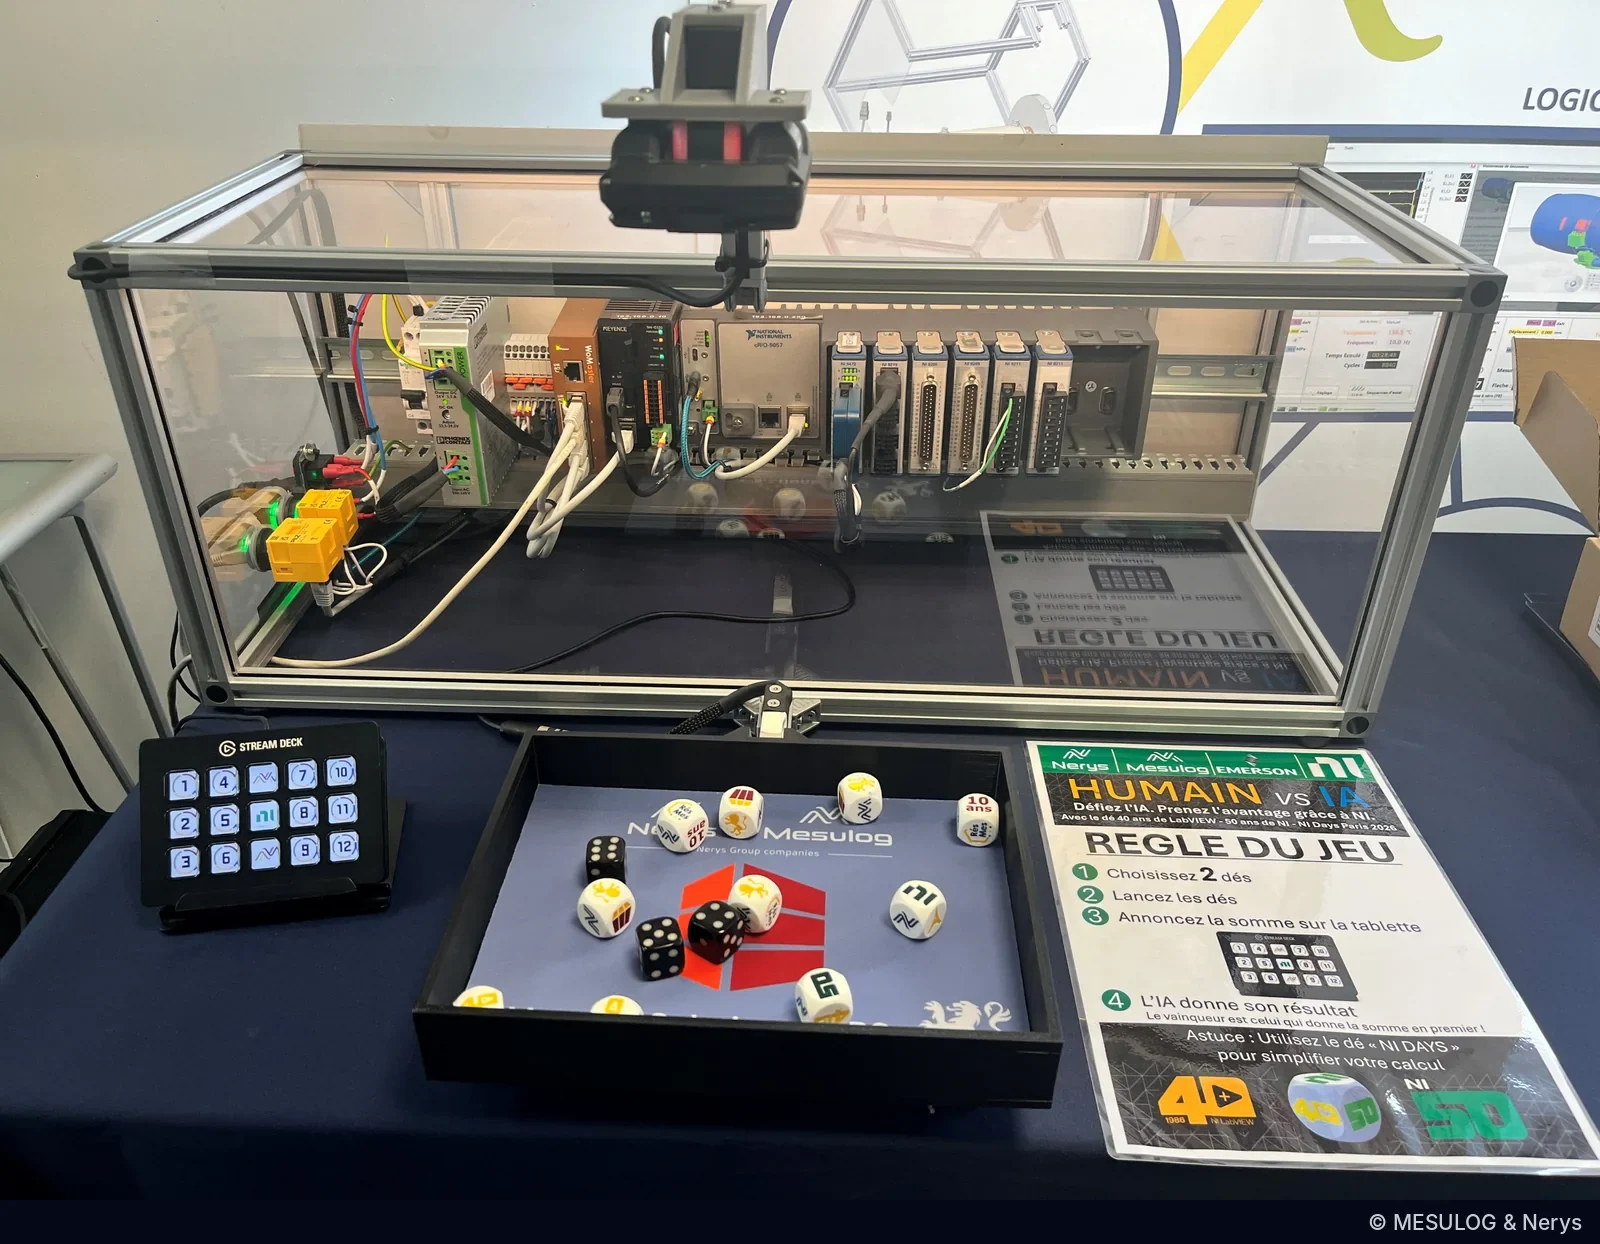
On stand B53, Nerys and Mesulog had set up a game: Human vs AI. The visitor throws two dice into a tray, adds up the visible faces and types the sum on a keyboard; meanwhile, a smart camera identifies the faces, calculates the sum and gives its verdict. The faster of the two wins. The game runs in Vasco, the bench control software published by Nerys: it triggers the camera, retrieves its result, times both players and displays the score. To complicate the task, the tray also contained illustrated white dice, a souvenir of the show's tenth anniversary, which count for zero points.
The game on stand B53: camera above the tray, keyboard for the human, and the rules of the game.A game in Vasco: the game screen, the view of the tray and the camera's verdict (29 s).
One image, thirteen decisions
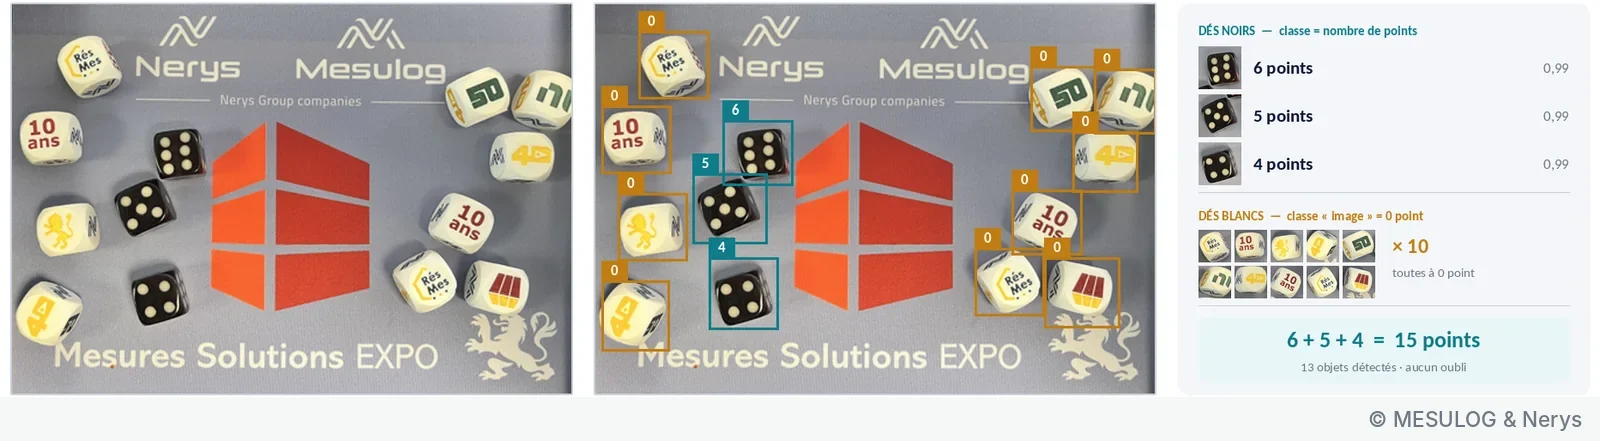
Behind the game, an object detection network from the convolutional network (CNN) family, the principle of YOLO-type detectors: from a single image, it locates each object, frames it and classifies it. In the image below, thirteen objects are detected: three black dice, classified "4 points", "5 points" and "6 points" with a confidence of 0.99, and ten white dice classified "image", worth zero. The sum, 15, is not calculated by the network.
What the camera sees, what the network detects and classifies, then the decision built by the software.
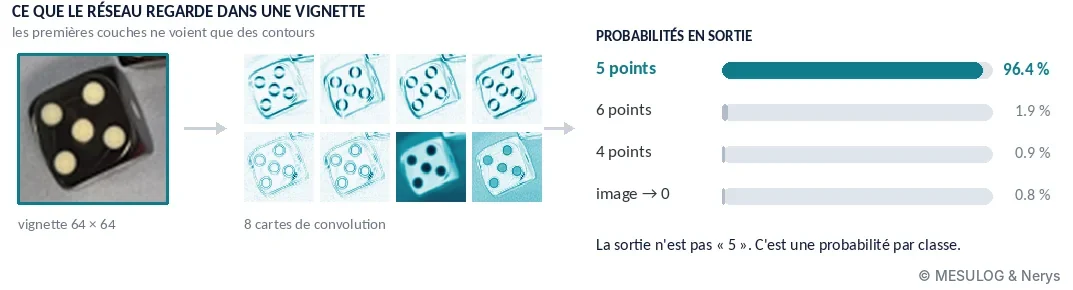
Inside the network, the first layers only see contours: on a 64 × 64 pixel thumbnail around a die, eight convolution maps bring out the edges and the dots. The following layers combine these patterns, and the output is not "5" but a probability per class: 96.4% for "5 points", 1.9% for "6 points", 0.9% for "4 points", 0.8% for "image".
The network's output is a probability distribution, not an answer.
This point has a direct consequence: the AI recognises the objects, it is the software that applies the rules of the game and makes the decision. It checks that there are indeed two countable dice, adds, compares and times; the confidence thresholds, for their part, are set and traced like program parameters. This division applies to any end-of-line visual inspection: the network perceives, the software decides, and the software is verified, versioned and accepted like any other.
What we did not have to do
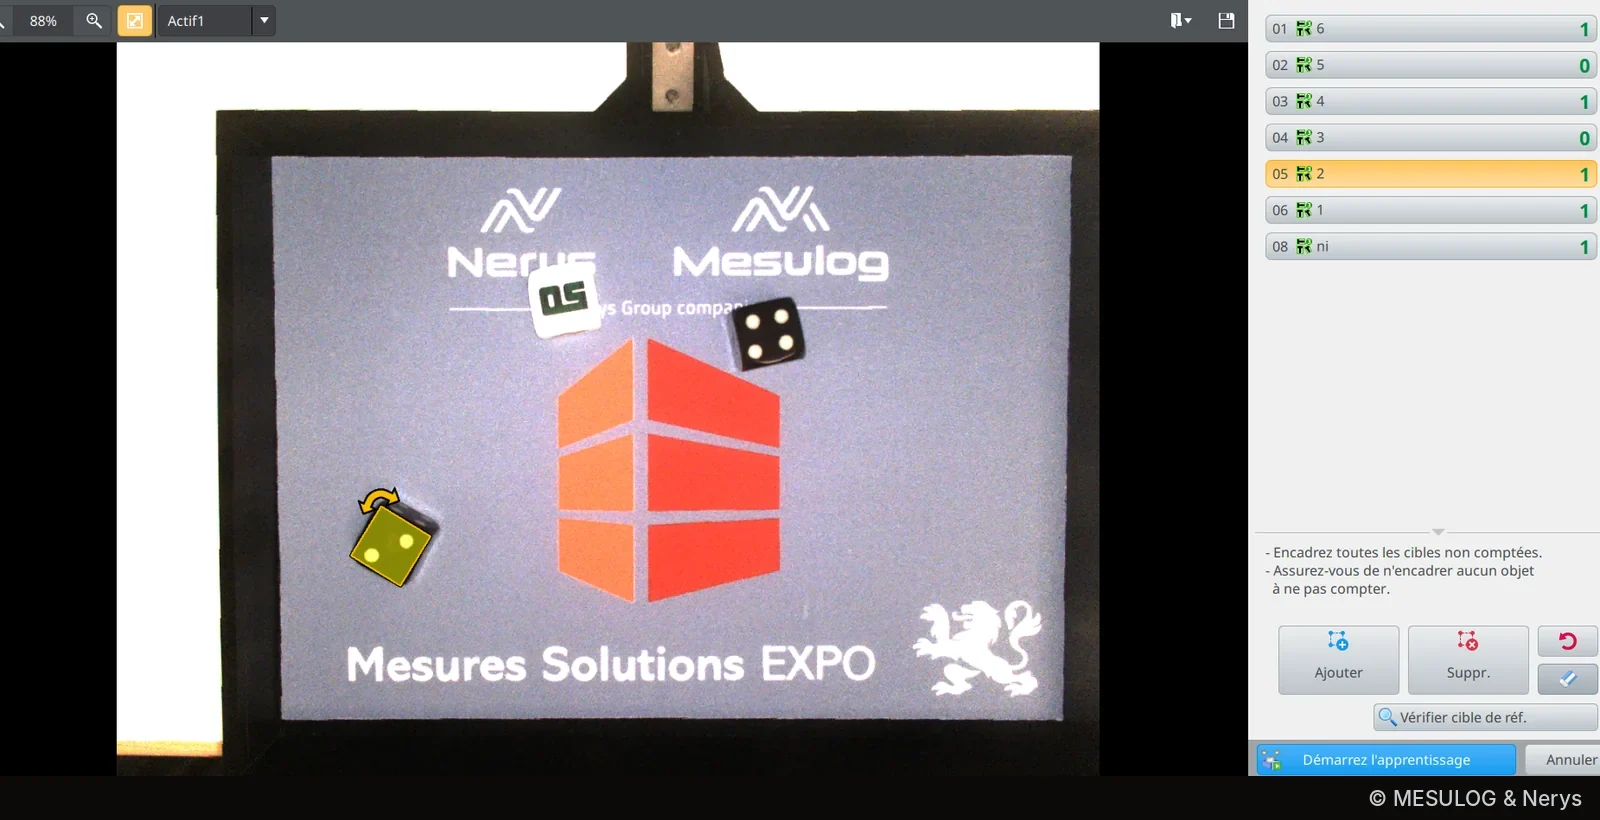
On the stand, recognition ran in a Keyence IV4 camera, which embeds its own training: no dedicated PC, no code. Configuration is done in four guided steps: optimise the image (triggering, lighting), record a reference image, set up the tools, assign the outputs. The team had defined eight tools: one per die face, one for the total, one for the logo. The complete inspection cycle takes about one second, and the verdict, the count and the match rate come out on I/O and over Ethernet, which Vasco uses directly.
What is surprising is what we did not do: write the network, or program face recognition rules ("count the black spots on a white background…"). You define the objects to recognise, provide annotated images of each face, and the network learns to separate them. When a target is missed in production, the operator frames it on the image, gives it its label and restarts training, in a few seconds.
A missed die: frame it, label it, restart training.
A word of caution, valid for all cameras of this type: retraining is a modification of the inspection program. Who retrained what, when, and on which images, must be traced like a software version. A camera that "learns" without a record is an instrument you can no longer say what it measures.
5. Predicting the zero crossing of a short-circuit current, with Schneider Electric
This is the example Amaury Laurent had to skim over the most, and the one that deserves the most space. It answers a question that sounds absurd put like this: can you act before the signal is there?
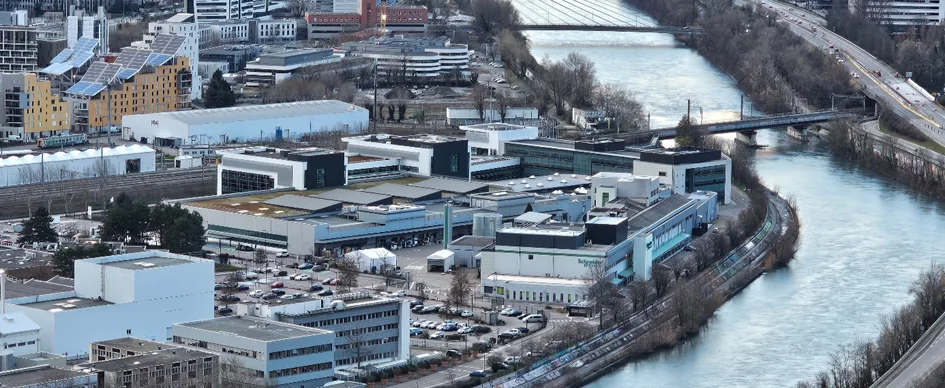
A century of testing in Grenoble. To understand the need, a word about the place. Schneider Electric was born in 1836 in Le Creusot under the name Schneider et Cie; the group now has more than 150,000 employees in more than 100 countries, with €40 billion in revenue in 2025. Its Grenoble roots come from Merlin Gerin, founded in 1920 by two Arts et Métiers engineers, Paul-Louis Merlin and Gaston Gerin, around medium- and high-voltage oil-bath circuit breakers. As early as 1921, the company set up a test laboratory, the Volta laboratory, to test its devices at high voltage; it would reach 800 kV in the 1930s. In 1946, Merlin Gerin presented its first circuit breaker able to interrupt a 10,000 A short circuit at 15,000 V, and in the 1960s Grenoble housed one of the largest dielectric test laboratories in Europe. Acquired by Schneider in 1992, the company is now fully integrated into Schneider Electric, which has kept the brand. The Technopole site, in the former Merlin Gerin premises, remains the group's Grenoble heart for switchgear: 1,200 employees, its laboratories and its support functions.
The Technopole site in Grenoble, in the former Merlin Gerin premises. Photo: Schneider Electric
F-Lab and the LEMT. Two main laboratories coexist there. F-Lab is Schneider Electric's test and certification laboratory in France: two platforms in the metropolitan area, Volta in Grenoble and Amplitude in Eybens, 14,000 m² of low- and medium-voltage testing, around a hundred engineers and technicians, COFRAC accreditation to ISO/IEC 17025, and tests carried out under the eye of third-party bodies such as ASEFA or LCIE for product certification. For high-power tests, it has three test generators, two of 600 MVA and one of 2,500 MVA, able to deliver in the order of 300 kA for one second at low voltage; it is this kind of machine that produces the short-circuit currents of this story. Next door, the LEMT, the medium-voltage test laboratory, handles specific tests and developments on switchgear. It is with its teams that Nerys and Mesulog worked.
What these laboratories know how to do, and what they asked for. The site's expertise fits in three words: switchgear, arc physics, test standards. Interrupting a short-circuit current means controlling an electric arc that forms between two opening contacts, with its pre-arc phenomena, and the certification standards precisely describe the conditions under which the interruption must succeed.
Switchgear, what these laboratories test. Photo: Schneider Electric
Some of these tests require fast switches to be commanded at a precise instant relative to the current zero crossing, to ensure the transition between high-power sources while limiting the arc energy in the object under test should an arc strike. The commands must be issued several hundred microseconds before the zero, to absorb the latencies of the switching chain, with an accuracy in the order of ten microseconds. The anticipation corrections must be finely and independently adjustable for each action and each phase, including on sequences of closely spaced actions, and some actions must be issued on the microsecond scale when a quantity is exceeded. And all this on a waveform whose frequency and amplitude are both unstable. That is the need as it was put to Nerys and Mesulog.
What the signal imposes. Before any method, the team looked at the laboratory's recordings, acquired at 1 MHz on the short-circuit bench: twelve reference recordings, thirteen usable current channels, peaks of several tens of kiloamperes. No simulation replaces a test campaign, and everything that follows is constrained by what these recordings contain. They impose four constraints.
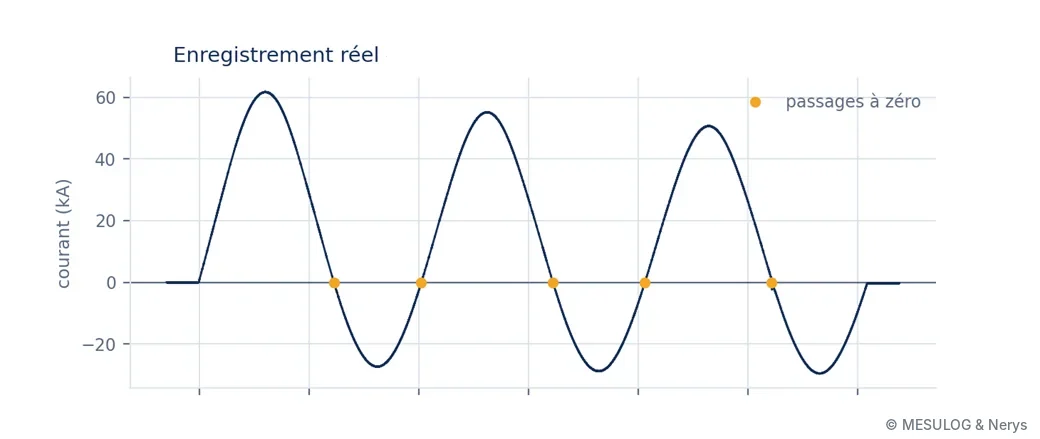
A real recording: the waveform is offset by the aperiodic component, the zero crossings are not evenly spaced.
First, an aperiodic component: the circuit is inductive, and the fault current is a sinusoid offset by a decaying exponential whose time constant is around twenty milliseconds. In the test above, the waveform rises to +62 kA on one side and falls to −28 kA on the other; the zeros are therefore not 10 ms apart. Next, the frequency is not 50 Hz: the bench generator slows down under the short-circuit torque, and the team measured from 50.7 to 48.7 Hz depending on the channel. At a 2.6% deviation, a prediction issued 1 ms before the zero assuming 50 Hz is already 26 µs out. In these recordings, the fault lasts only 50 to 65 ms, i.e. three periods: you see the beginning of the slowdown, not its settling. Third constraint, the noise rules out any local method: with a standard deviation of about 48 A before the fault and a slope at the zero going down to 5.9 A/µs, a threshold detection jitters by 16 µs, for a budget of 10. Estimating the frequency on a single half-cycle gives anything between 42 and 60 Hz, because the offset shifts the zeros; over a full period, the asymmetry cancels out and you find 50.1 Hz. You need a model that explicitly separates the offset from the sinusoid. Finally, you must be ready to control 5 ms after the current is established, i.e. a quarter of a period: the estimator is not allowed to converge slowly.
The method, in broad terms. Everything starts from an analytical model of the fault current, which is nothing secret since it is the physics of a short-circuited inductive circuit:
I(t) = a·sin(ωt) + b·cos(ωt) + C + d·e−t/τ
The sine and cosine terms carry the amplitude and phase of the fundamental, C is a residual DC offset, and the exponential term is the aperiodic component, with its time constant τ. The angular frequency ω is not fixed at 50 Hz: it is one of the unknowns.
The principle is then to identify these parameters continuously, by least squares, on the samples already acquired. At each new sample, the difference between the measurement and what the model predicts, the innovation, is used to correct the estimate recursively, with progressive forgetting of old samples to follow the evolution of the signal. It is the linear regression of example 3, updated a million times per second. In parallel, a frequency-locked loop corrects the angular frequency: the frequency is tracked, not assumed. Once the parameters are known, the instant of the next zero crossing is derived from the model by a closed-form formula: no search, no iteration. This is what makes the computational cost constant per sample, and therefore compatible with an FPGA processing one sample per microsecond on three simultaneous current channels. In fixed point, the way the recursion is written is not trivial: some classical formulations drift numerically until the estimate diverges, and the team chose one that remains stable. The details of these mechanisms, the weightings and the settings remain between Nerys, Mesulog and Schneider.
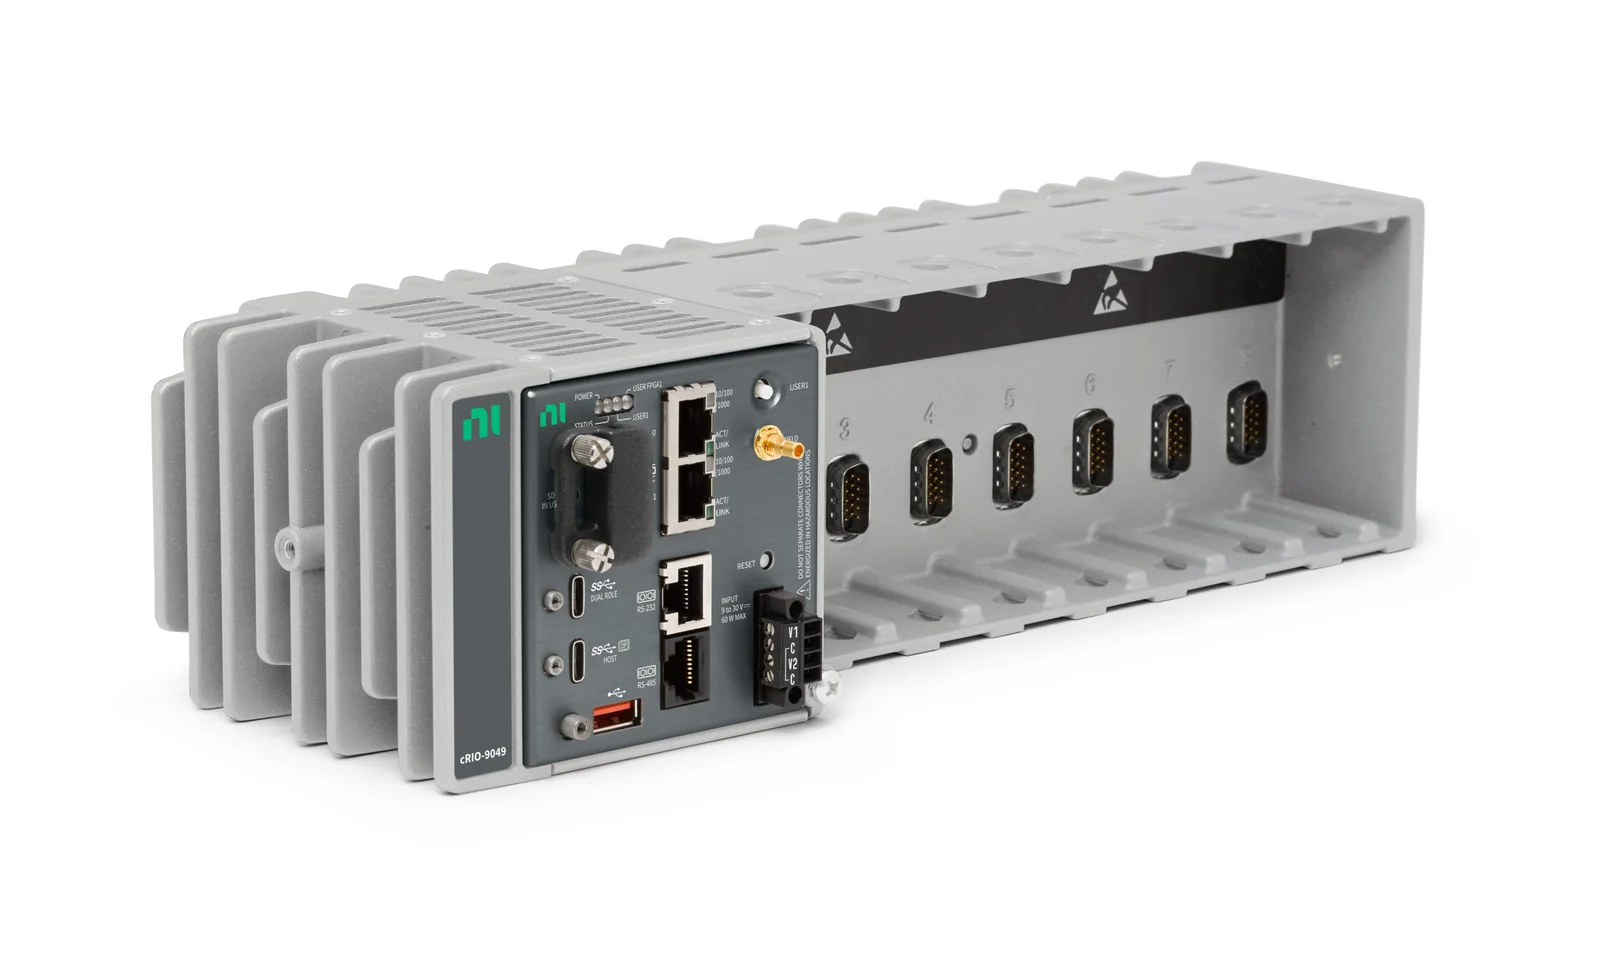
The target: a CompactRIO 9049 (NI, Emerson group), whose Kintex-7 FPGA processes the three current channels at 1 MHz. Photo: NI (Emerson group)
The video below replays a real recording from the laboratory. At the top, the measurement and the estimated model, superimposed from the first milliseconds; at the bottom, the distance to the next zero crossing calculated every microsecond. Triggering is requested 100 µs before the predicted zero; the gap between the actual zero and the target instant is displayed at each crossing.
Prediction of the next zero crossing on a real short-circuit current, sampled at 1 MHz (60 s).Zoom on a zero crossing: the command is issued 100 µs in advance, the actual zero arrives within a few microseconds of the target instant (13 s).
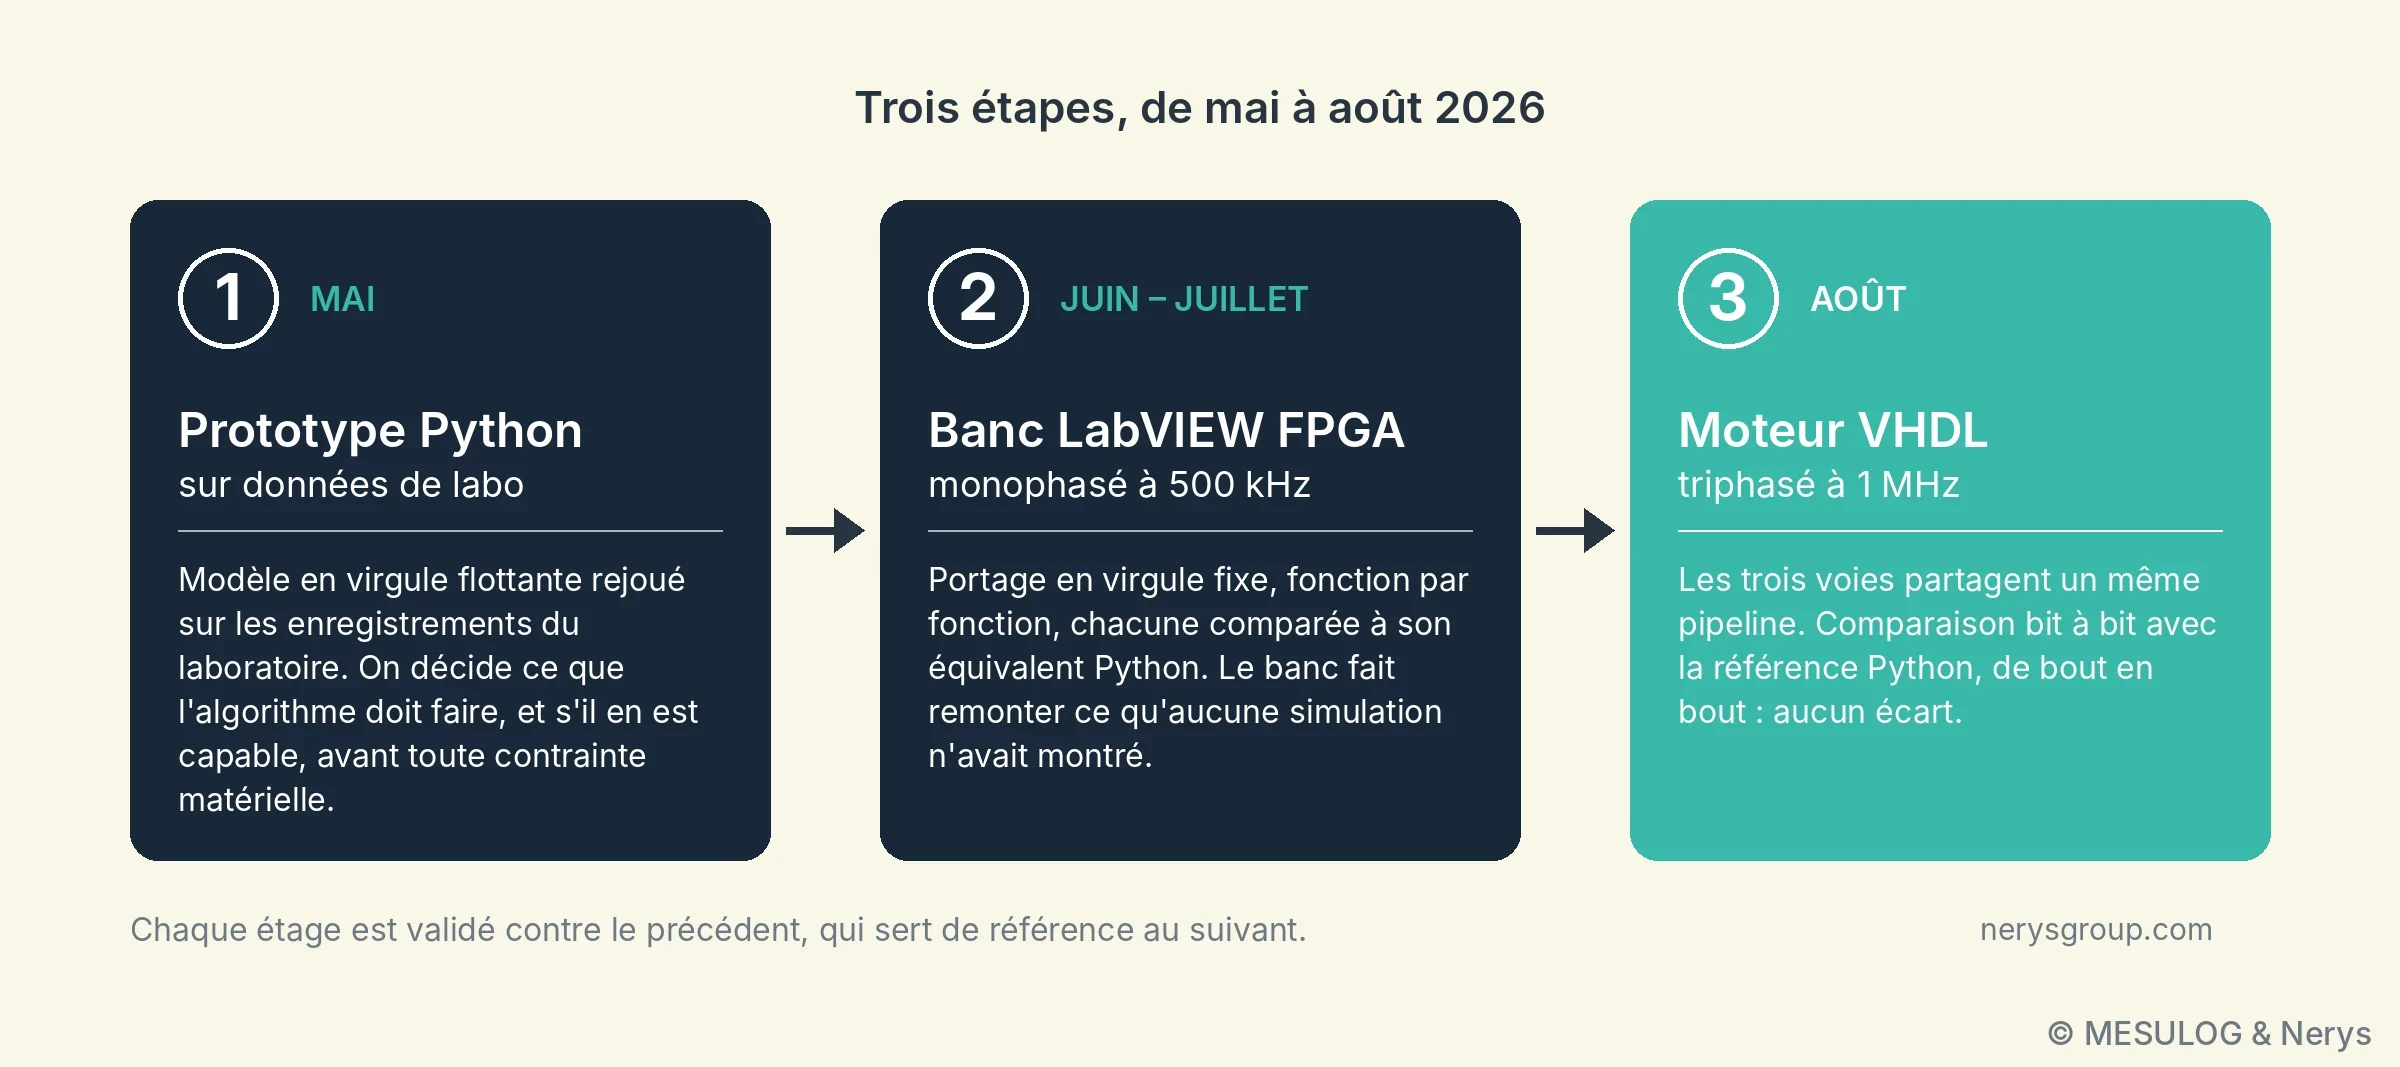
Three stages, from May to August 2026. The integration constraints, FPGA, 1 MHz, fixed point, offer no flexibility for designing an algorithm. The engineers therefore separated the problems. In May, a floating-point Python prototype, replayed on the laboratory's reference recordings: this is where you decide what the algorithm must do and whether it is capable of it, before any hardware constraint. In June and July, a single-phase LabVIEW FPGA bench at 500 kHz: porting to fixed point, function by function, each compared with its Python equivalent on the same vectors. In August, a three-phase VHDL engine at 1 MHz, the three channels sharing a single pipeline, compared bit for bit against the Python reference from end to end: no deviation.
The important word in stage 2 is "bench". Tests on real data brought up what no simulation had shown: detection bounces near the zero, due to converter noise, and fixed-point formats that were too short on some accumulators. This is information that can only come from hardware, and the Schneider team's feedback on real behaviour near the zero redirected several implementation and parameter choices. And the zero bit-for-bit deviation of stage 3 is not a formality: it is what allows us to say that the VHDL does exactly what the prototype does, no more, no less.
Three stages, from May to August 2026: each stage is validated against the previous one, which serves as the reference for the next.
How generative AI was used. This is the part that most surprised the room, and the one that must be described precisely so as not to oversell it. The AI did not design the algorithm. It ported an algorithm designed and validated in floating point to fixed point, LabVIEW then VHDL, wrote the test benches and their vectors at the same time as the code, and kept the documentation up to date. What made this possible comes down to three ideas.
The first: the deviation comes back as a number. A harness compares each implementation with the reference, sample by sample, in microseconds and in bits. The feedback is never "it doesn't work", but "at sample 1247, this state diverges by 3 LSB". The harness produces a deviation, not an opinion, and the correction that follows is targeted. The second: what has been understood once is written down. Every pitfall found, an index shift in a recursion, a format that is too short, goes into a file re-read at each session; you do not pay for it twice. The third: the plan comes before the code. The big batches, such as sharing the three channels on a single engine, are specified in a document validated before the first line. You do not correct a direction after 2,000 lines.
The condition for everything else, and what cost the most to build: a bit-exact Python model of the fixed-point arithmetic. Without it, the loop has no sensor, and no iteration is verifiable. The image given by Amaury Laurent is that of a control loop: "the AI produces, the human measures the deviation and feeds it back". What makes the loop stable is that the deviation is a measurement and not an assessment, and that human expertise sets the gain. A loop that does not lock, you stop it, and you start again from a fresh plan rather than piling up fixes.
What remained human. The know-how. The specification and the acceptance criterion. The physical reading of a result, converter noise or real bug. The architecture trade-offs, and the abandonment of leads that did not hold. The bench, the data, and what goes to the customer. In three months, in the order of ten thousand lines of VHDL, three times as much Python model and harness, more than twenty thousand lines of documentation and more than two hundred versioned iterations. The limiting factor was never the speed of writing code, but that of verification; that is where the tool was useful. Each modification was compared with the reference in a few minutes, where a conventional port is verified by simulation campaigns.
Where the accuracy stands. The estimate refines continuously: the later the prediction is issued, the more accurate it is. On the nine channels of the three-phase tests, the median error on the instant of the zero is about 50 µs when the prediction is issued 1 ms before the zero, 15 µs at 0.5 ms, 5 µs at 100 µs and 2 µs at 10 µs. The trade-off is therefore negotiated against the response time of the switching device: the slower it is, the earlier you have to decide, and the larger the error.
1 ms before50 µs
0.5 ms before15 µs
0.1 ms before5 µs
10 µs before2 µs
Prediction error on the instant of the zero as a function of anticipation: median over the 9 channels of the three-phase tests.
With the current settings, the target of less than 10 µs is reached at the closest range on three channels out of nine, and five others lie between 12 and 40 µs. These figures are not final, and the speakers preferred to say so as it is rather than present as settled a result that is not. On the resources side, the three-phase VHDL engine remains bit-for-bit identical to the Python reference, occupies 29% of the Kintex-7 FPGA's DSP blocks and consumes 22 of the 40 clock cycles available for each sample: there is margin left for what comes next.
6. A file of measurements and a generative AI: what works, and what does not
The workshop had started with a show of hands: "who has already asked an AI for something without really knowing what they were looking for?" Hands went up, with laughter. The last example answered that.
The most everyday of the six: a CSV file of measurements as input, a generative AI, and a deliberately vague request, "analyse this for me". The demonstration file contains 200 parts run on an electronic test bench: timestamp, serial number, bench, operator, 3.3 V and 5 V voltages, quiescent current, clock frequency (25 MHz nominal), temperature, RMS noise, test duration, verdict and list of out-of-limit measurements.
The analysis of the CSV by a generative AI, from the request to the results workbook (40 s).
The result is impressive. In a few minutes: statistics per column, histograms, breakdown of failures by operator and by bench, correlations, and a formatted Excel workbook with its charts. This is where the Mesulog and Nerys teams save the most time today, without a six-month project: analysing an error log, formatting a report, the first rough pass over a file you are discovering.
But did we get the information that allows a decision? Not necessarily. A starting point, yes; a business analysis goal, no. "This time, it didn't really work, because we didn't know what we were looking for," the speakers admitted. A system asked to find something will always find something: a correlation between an operator and the RMS noise, for example, or a trend that follows the temperature of the day. Just because there are 250 firefighters at a fire does not mean that every event where you see 250 firefighters is a fire. The correlation is real, the explanation is not in the file, and it is the person who knows the bench who knows whether it makes sense.
The difference with example 2 lies there. Asking WATS about last week's FPY drop is asking a precise question of structured data; asking "analyse this for me" is delegating the question itself. The tool is the same, the result is not.
The twist: a stable signal, who signs off?
The workshop ended with a measurement. A signal acquired every day on a bench, flat, clean, repeatable from one day to the next. Question to the room, by show of hands: "this signal is stable, who signs off?" Hands went up.
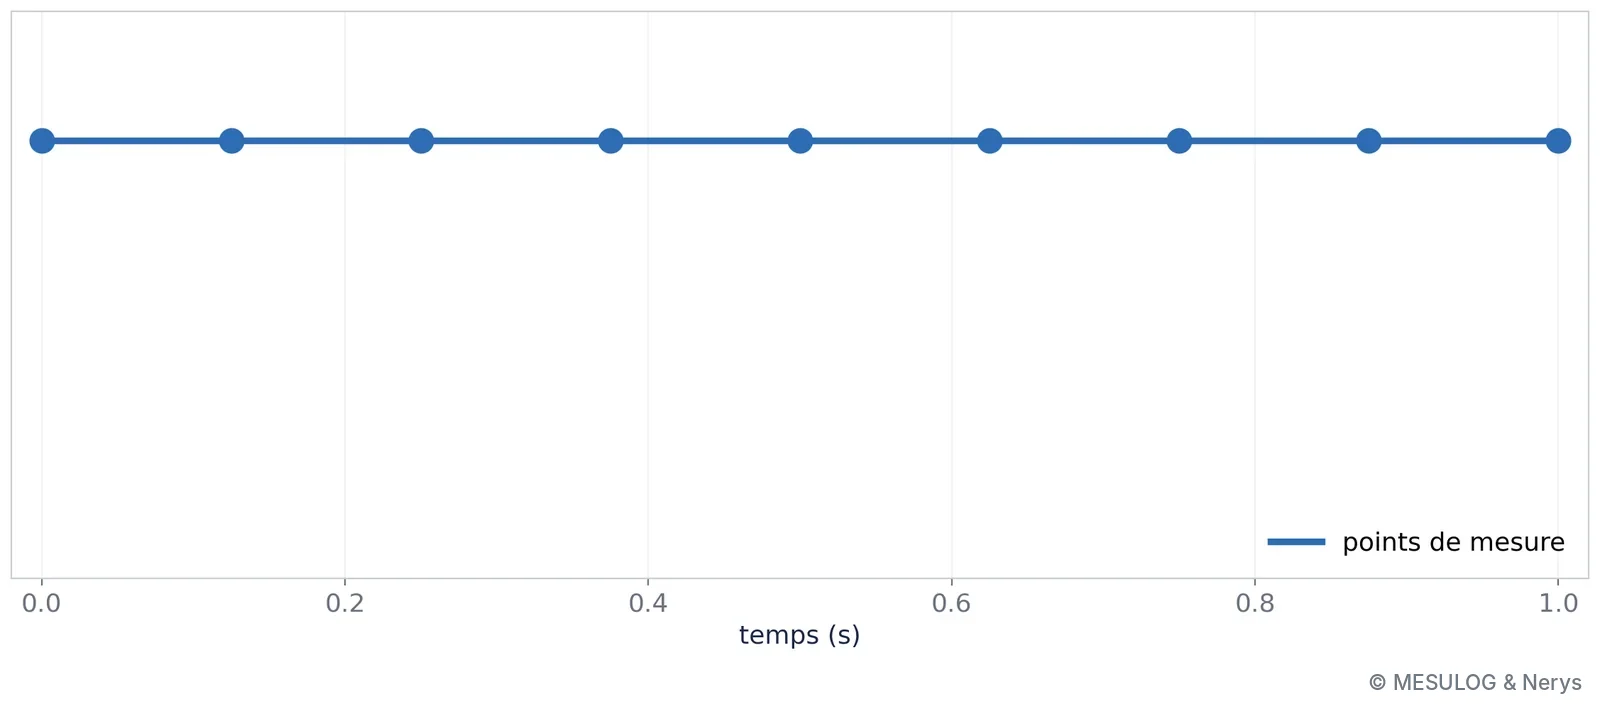
The signal shown to the room: perfectly stable.
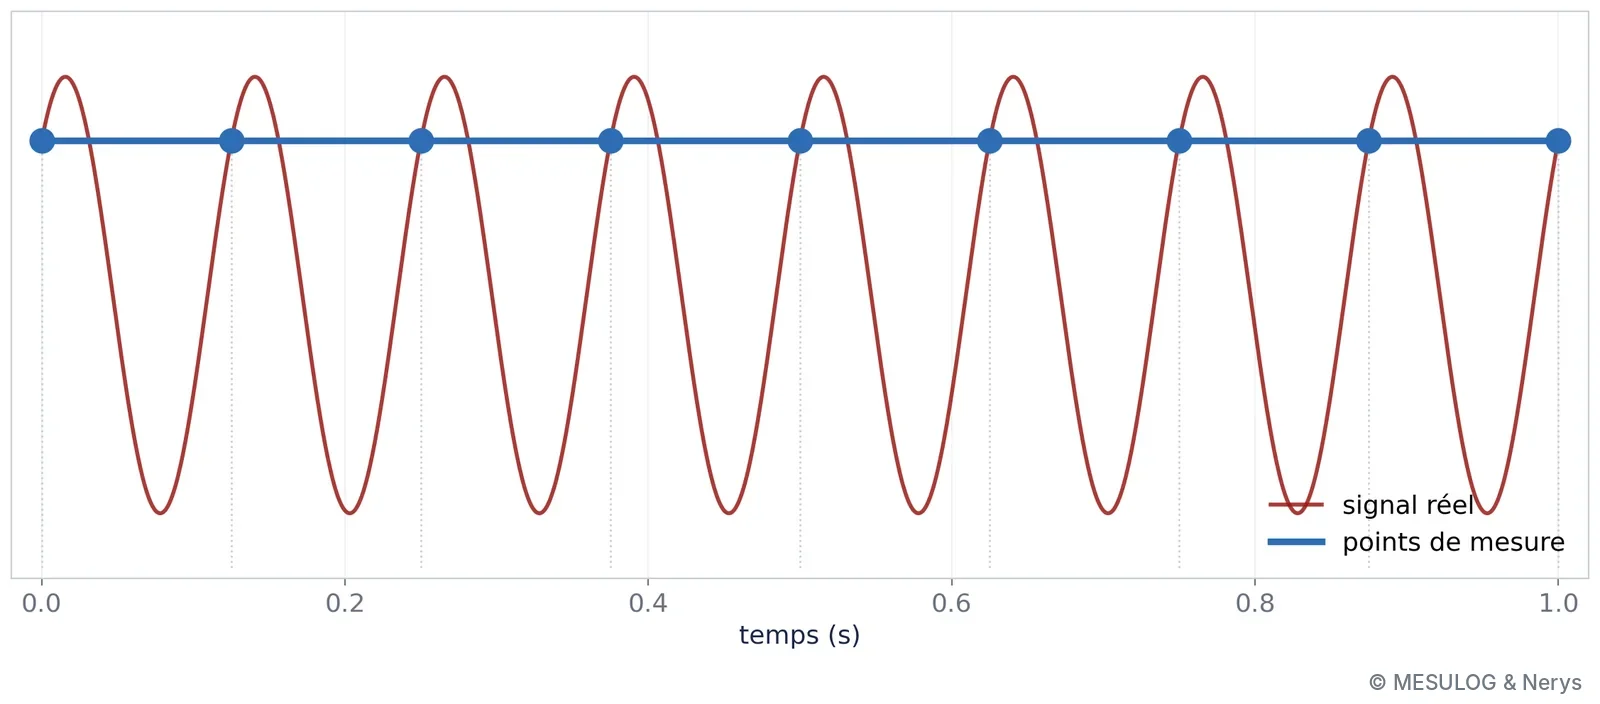
Then the real signal: a clear oscillation, sampled at an unfortunate frequency. The measurement points had not moved. Each sample fell at the same place in the period, so that the whole oscillation disappeared behind a straight line.
The real signal. The measurement points are the same; the oscillation passes between them.
This is not a measurement error: the instrument did exactly what it was asked. It is aliasing. The sampling theorem has said so since Nyquist and Shannon: to represent a signal, you must sample at more than twice its highest frequency. Below that, a fast oscillation folds into a lower frequency, and in the extreme case of synchronous sampling, into a constant. No downstream processing recovers it: not statistics, since the standard deviation is zero, not a convolutional network, not a language model. The remedy is upstream: know the frequency band of the phenomenon, choose the sampling rate accordingly, and place an anti-aliasing filter before the converter. Only knowledge of the physical phenomenon made it possible to see the trap, before the measurement, not after.
Who decides?
The conclusion of the workshop fitted in one diagram: at the centre, the person responsible for the measurement; around them, the consoles — statistics, classification, vision, generative — and the protocols that connect a model to your benches and your data. The engineer is no longer the one who builds the tools: AI has simplified their use so much that anyone can use them. They become the one who manages their power, and they drive it all the better for understanding it. AI is a tool, extraordinarily powerful, but a tool.
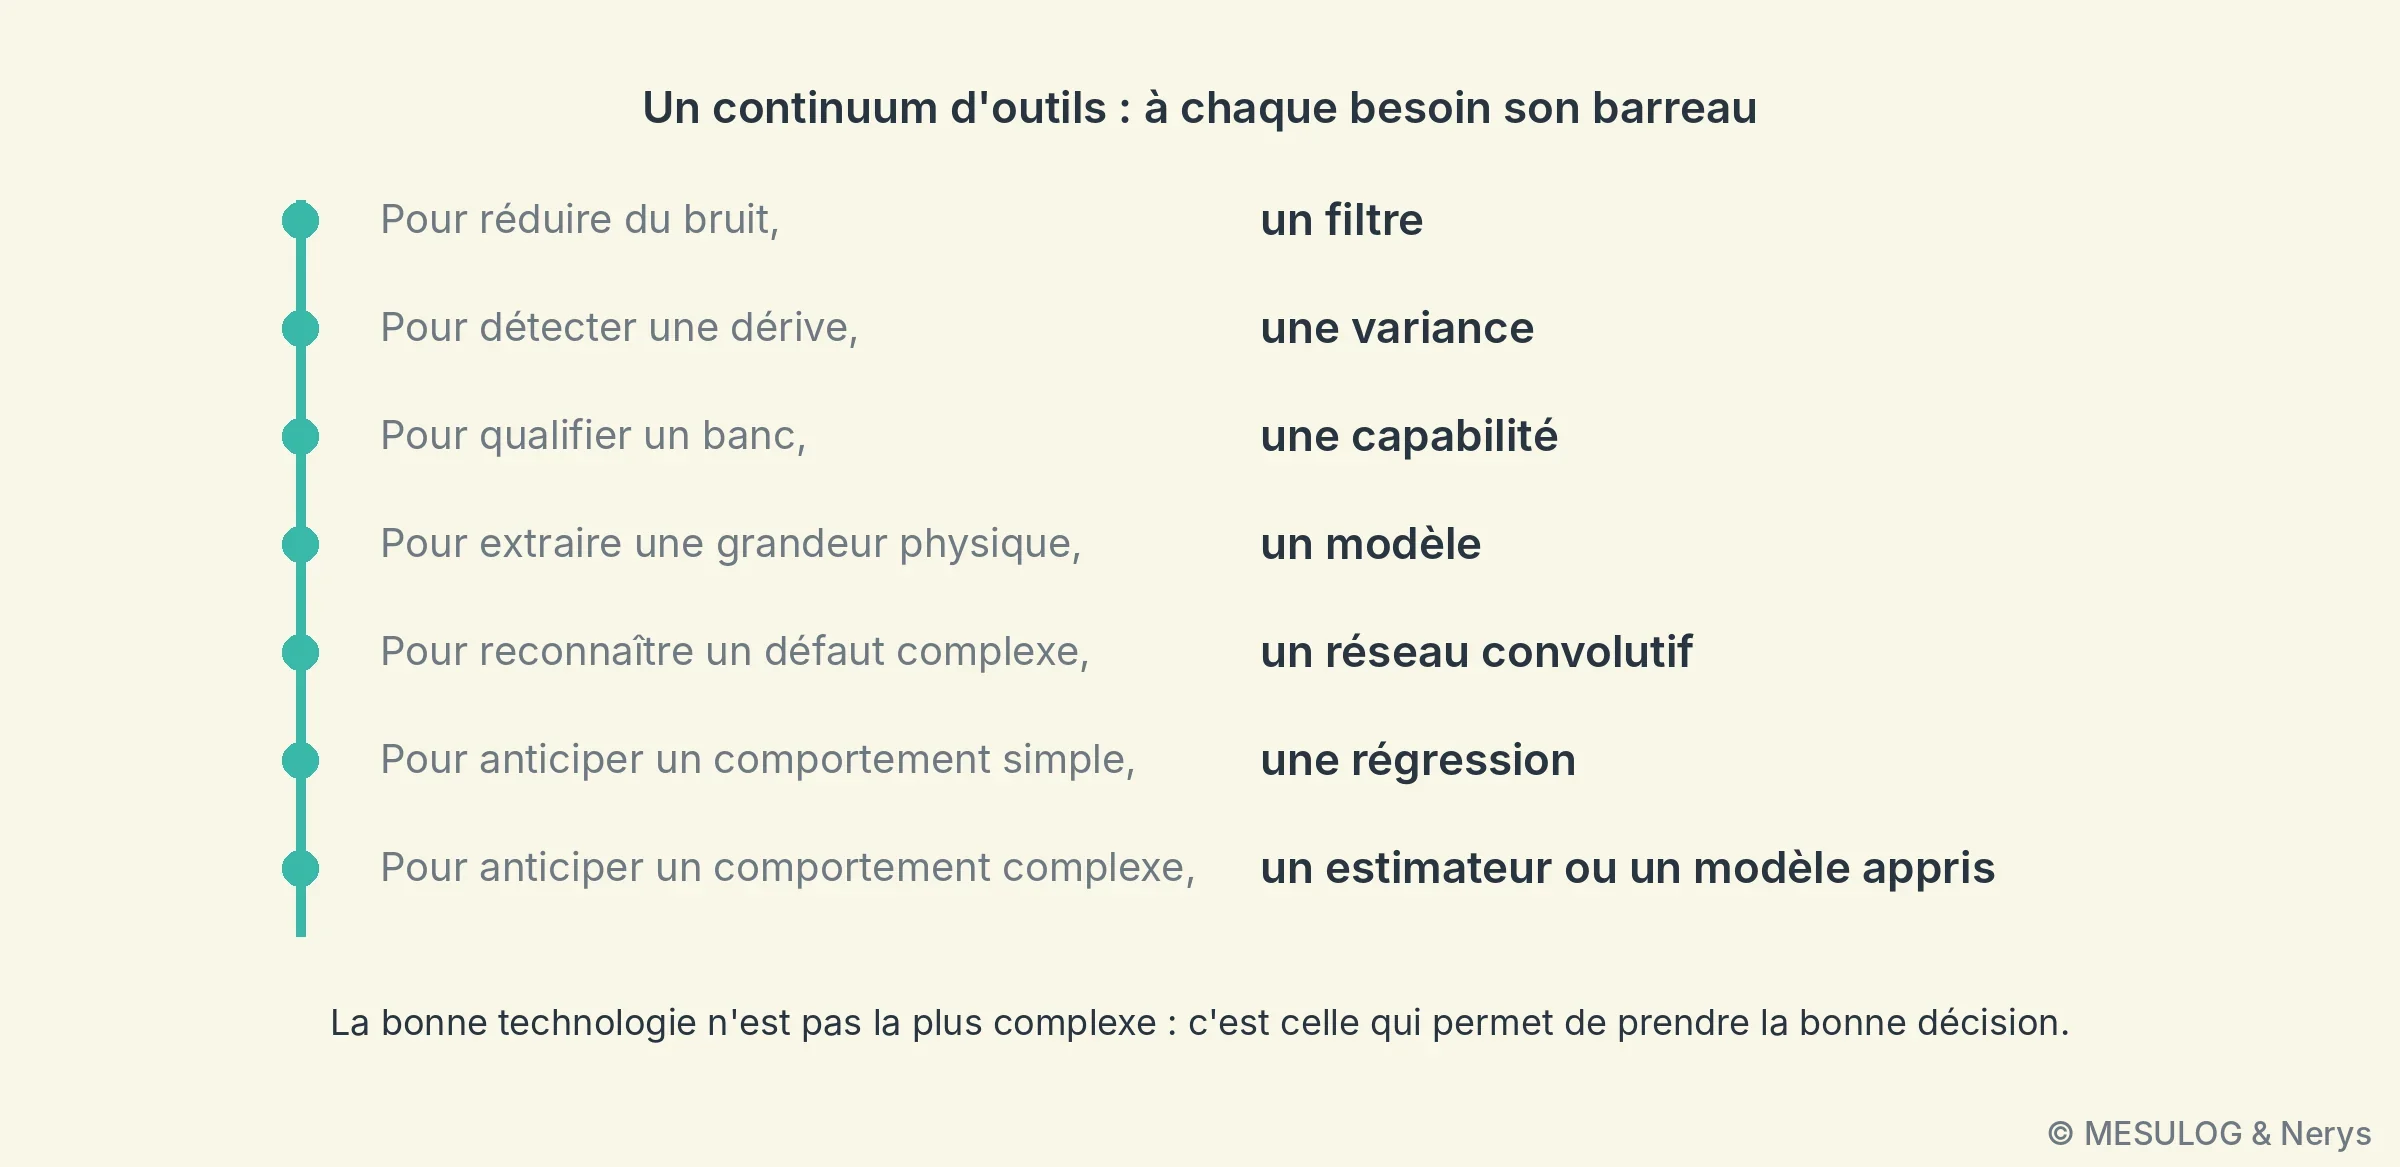
There is not statistics on one side and AI on the other. There is a continuum of tools, and an engineer who chooses the right rung of the ladder.
A continuum of tools: each need has its rung.
To reduce noise, a filter, mean or median depending on the nature of the noise. To detect a drift, a variance or a CUSUM chart. To qualify a bench, a capability. To extract a physical quantity from a point cloud, a geometric model. To recognise a complex defect, a convolutional network. To anticipate a simple behaviour, a regression; a complex behaviour, an estimator or a learned model. The right technology is not the most complex. It is the one that allows the right decision to be made.
A measurement you don't know what to make of, a signal to anticipate rather than endure? The Nerys and Mesulog teams are happy to talk about it: web@nerysgroup.com.
On 2 June, the Nerys teams took part in NI Days France 2026 in Paris, the annual gathering of test, measurement and industrial automation professionals. This edition marked two emblematic anniversaries: 50 years of NI and 40 years of LabVIEW, a technology that has profoundly transformed the way test and measurement systems are designed in industry.
A look back at our talk
On this occasion, our experts led the session: "LabVIEW Debugging – Architects' secrets, developers' best practices"
On the agenda: debugging methods, software quality and lessons learned from industrial projects.
The talk covered several concrete topics:
Best practices to limit the appearance of bugs from the design phases;
Diagnostic tools of the NI environment such as VI Analyzer, InstrumentStudio and DETT;
The contributions of Nigel™, the new artificial intelligence developed by NI to facilitate the diagnosis of instrument communications;
The use of generative AI for event log analysis and the identification of the causes of malfunctions.
The many exchanges with participants showed the growing interest in topics related to artificial intelligence, cybersecurity and the robustness of industrial software architectures.
On our stand, visitors were also able to discover a demonstration designed by our electrical engineering department.
From the design of the enclosure to its final integration, this achievement illustrated our approach: turning a technical need into an operational solution. A great opportunity to discuss NI technologies and our areas of expertise:
The celebrations of 50 years of NI and 40 years of LabVIEW recalled the considerable impact of these technologies on the world of engineering. The arrival of Nigel™ opens a new stage in this evolution by integrating artificial intelligence directly into the tools used by engineers.
For more than 25 years, Nerys Group has been supporting its customers in the design, development and industrialisation of test and measurement solutions: test benches, PXI and CompactRIO systems, LabVIEW and TestStand development, acquisition and exploitation of industrial data. An expertise built at the pace of the technological developments driven by NI, and which we continue to develop alongside our customers.
We thank the NI teams for organising this event, as well as all the visitors who came to attend our talk and talk with our experts.
"Projects like this one, you do one, maybe two in a career!" stresses Amaury Laurent, embedded systems and R&D project manager at Nerys. This exceptional adventure, in which he is so proud to have taken part, is the Tyrex-2 project, named after a machine unique in the world, designed and used at the Institut Laue-Langevin (ILL) in Grenoble. Tyrex-2 produces polarised helium-3, a gas intended to increase the sharpness of the neutron beams used to study the electromagnetic properties of matter, in major experiments in fundamental research as well as in R&D. The standard Vasco software, developed by Nerys to control test installations, was chosen by the ILL to control Tyrex-2. One year after the machine was commissioned, the software, which runs continuously 24 hours a day with nearly 2,700 lines of scenarios, has demonstrated its reliability and its ability to control a highly complex special machine.
The ILL, one of the most intense neutron sources in the world
Contributing to the Tyrex-2 project means adding a modest stone to the edifice of world research that the ILL represents. Created in 1967 to seal Franco-German friendship and cooperation in research, the ILL provides scientists from all over the world with neutron beams generated by nuclear reactions.
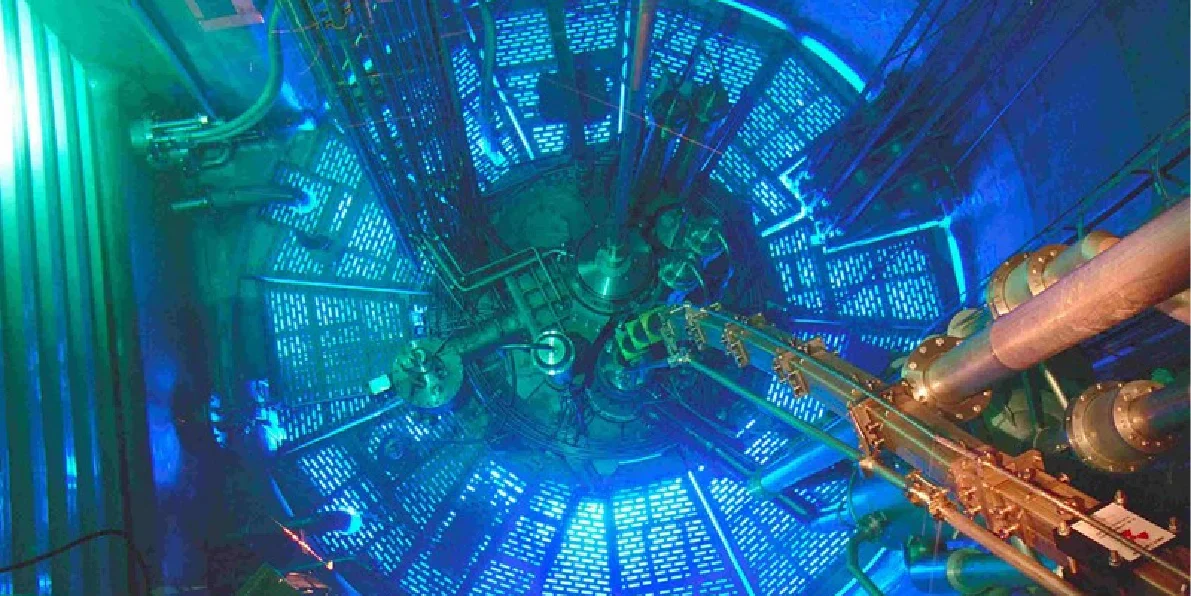
View of the ILL reactor, blue light produced by the Cherenkov effect.
Why produce neutrons? As electrically neutral components of atoms, neutrons make it possible to see the properties of matter with very fine resolution, particularly in metals.
Polarised helium-3 enhances this ability. Polarised by the gas, neutrons make it possible to measure magnetic properties precisely.
Every year, around 1,400 researchers from more than 40 countries come to the ILL to carry out some 1,000 experiments, selected by a committee of experts. These experiments advance fundamental research in fields as varied as biology, chemistry, nuclear physics and materials science. The ILL also works closely with the R&D departments of many industrial companies.
Tyrex-2: an installation for polarising helium-3
Some experiments carried out at the ILL require polarised helium-3. The neutron optics department is in charge of producing it. David Jullien has worked there for more than 20 years. "There are very few traces of helium-3 in its natural state on Earth. Existing stocks come from nuclear industry waste and the decomposition of warheads. This gas is present in significant quantities in the lunar atmosphere," he explains.
To develop the use of polarised helium-3 for neutron experiments, the ILL set up a dedicated team and in 2000 designed a machine, named Tyrex, to polarise the gas and package it in experimental cells. The installation also recovers the polarised helium-3 used in experiments and purifies it before reuse.
"Commissioning Tyrex was strategic. It limited helium-3 losses and allowed the ILL to recycle and polarise an average of 200 litres of gas per year," stresses David Jullien. "The machine showed its first signs of ageing in 2017. We then set about building a new one," explains the expert, who programmed the machine. He adds: "We took advantage of the reactor shutdown for maintenance, over two years, to build it. We designed a larger, more reliable machine to increase production rates. We also made it more autonomous and easier to use," the technician explains.
How Tyrex-2 works
Built from granite, titanium and other non-magnetic materials, fitted with a three-metre-long compressor, glass piping made and welded by a master glassblower (Meilleur Ouvrier de France), lasers and custom optical systems, Tyrex-2 stands out as much for its polished aesthetics and technical sophistication as for the complexity of the helium-3 polarisation process.
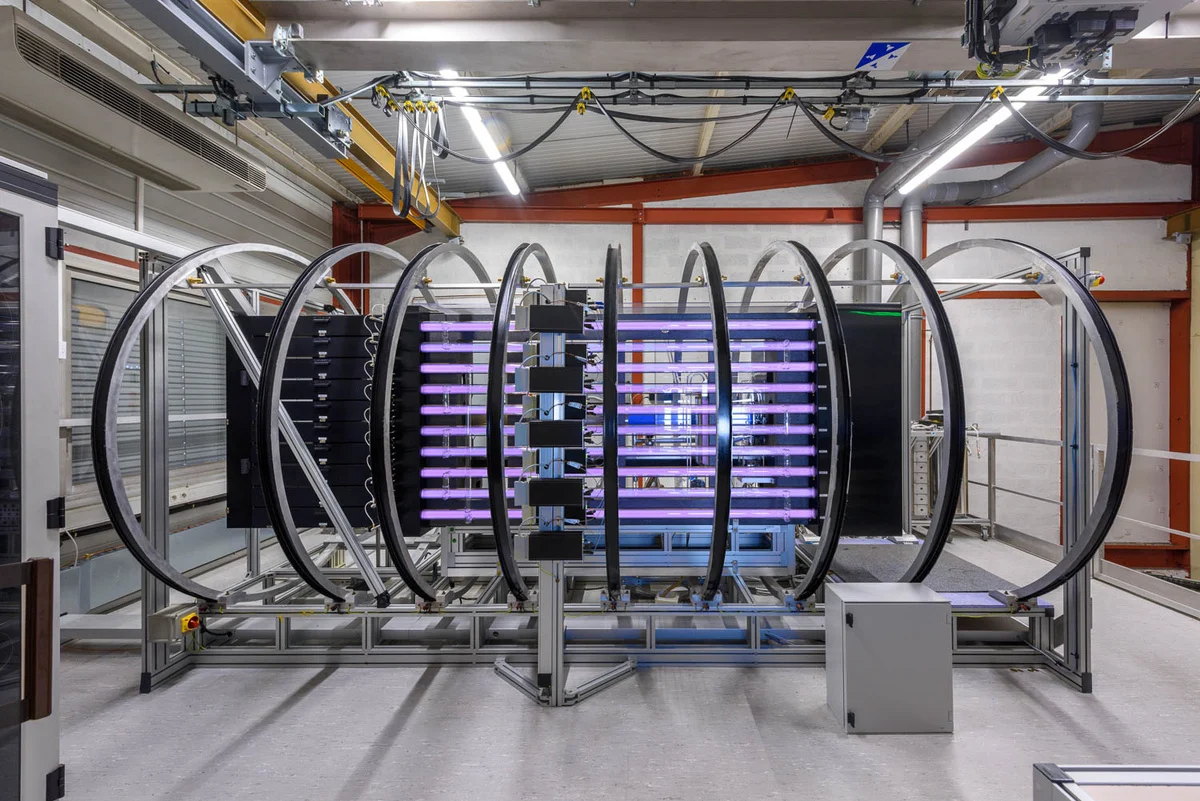
The Tyrex-2 machine designed by the ILL neutron optics department. It polarises and "recycles" helium-3.
Helium-3 under pressure
To be polarised, helium-3 must be kept at low pressure (1 mbar). Conversely, polarising a neutron beam requires the helium to be at high pressure (2 or 3 bar). Tyrex-2 solves this problem through a complex helium-3 transfer process that preserves its polarisation while compressing it to the right pressure, right up to delivery to the experiment sites.
Polarising helium-3
To avoid contaminating the gas, Tyrex-2 is equipped with multiple purification systems. A first step consists in bringing the helium contained in a tank down to a pressure of 1 mbar. This helium is injected into glass tubes subjected to an electric field and a high-power polarised infrared laser beam. Polarisation is obtained by optical pumping of an excited state of helium-3 generated by the combined action of the electric field and the laser beam. This is how the helium is polarised. This technique, called MEOP (Metastability Exchange Optical Pumping), only works at low pressure (here 1 mbar) to obtain high polarisation rates.
Preserving polarisation
The polarisation of helium-3 is a fragile state that can easily be "broken". For the helium to remain polarised, it must not be subjected to significant variations in magnetic field. Tyrex-2 is fitted with 9 coils generating an extremely homogeneous magnetic field and is built entirely from non-magnetic materials. Using a special device developed by the ILL, the polarisation of the gas is measured at this stage; it must reach a level of around 80%.
Bringing the gas up to pressure
Through a "play" of valve openings, and under the action of a 3-metre-long linear compressor driven by a hydraulic cylinder, the gas contained in the glass tubes at very low pressure is transferred, via several compression sequences, into a glass tank (a buffer). When this buffer reaches the nominal pressure of 300 mbar, the gas is transferred into the experimental cells via the same compressor. The operation is then repeated until the desired pressure is reached in the experimental cells. The gas is transferred in a single pass for small cells, and up to ten times for the largest. Filling the cells, made of glass or silicon, can take up to four hours. Tyrex-2 also processes the "dirty" helium returning from experiments via a "separate circuit" marked out by various filters.
The helium-3 polarisation and recycling installation was designed to be more autonomous than the first one. The whole point of using a solution such as Vasco was to optimise, as far as possible, the machine's various compression cycle times and to avoid losses of the precious gas.
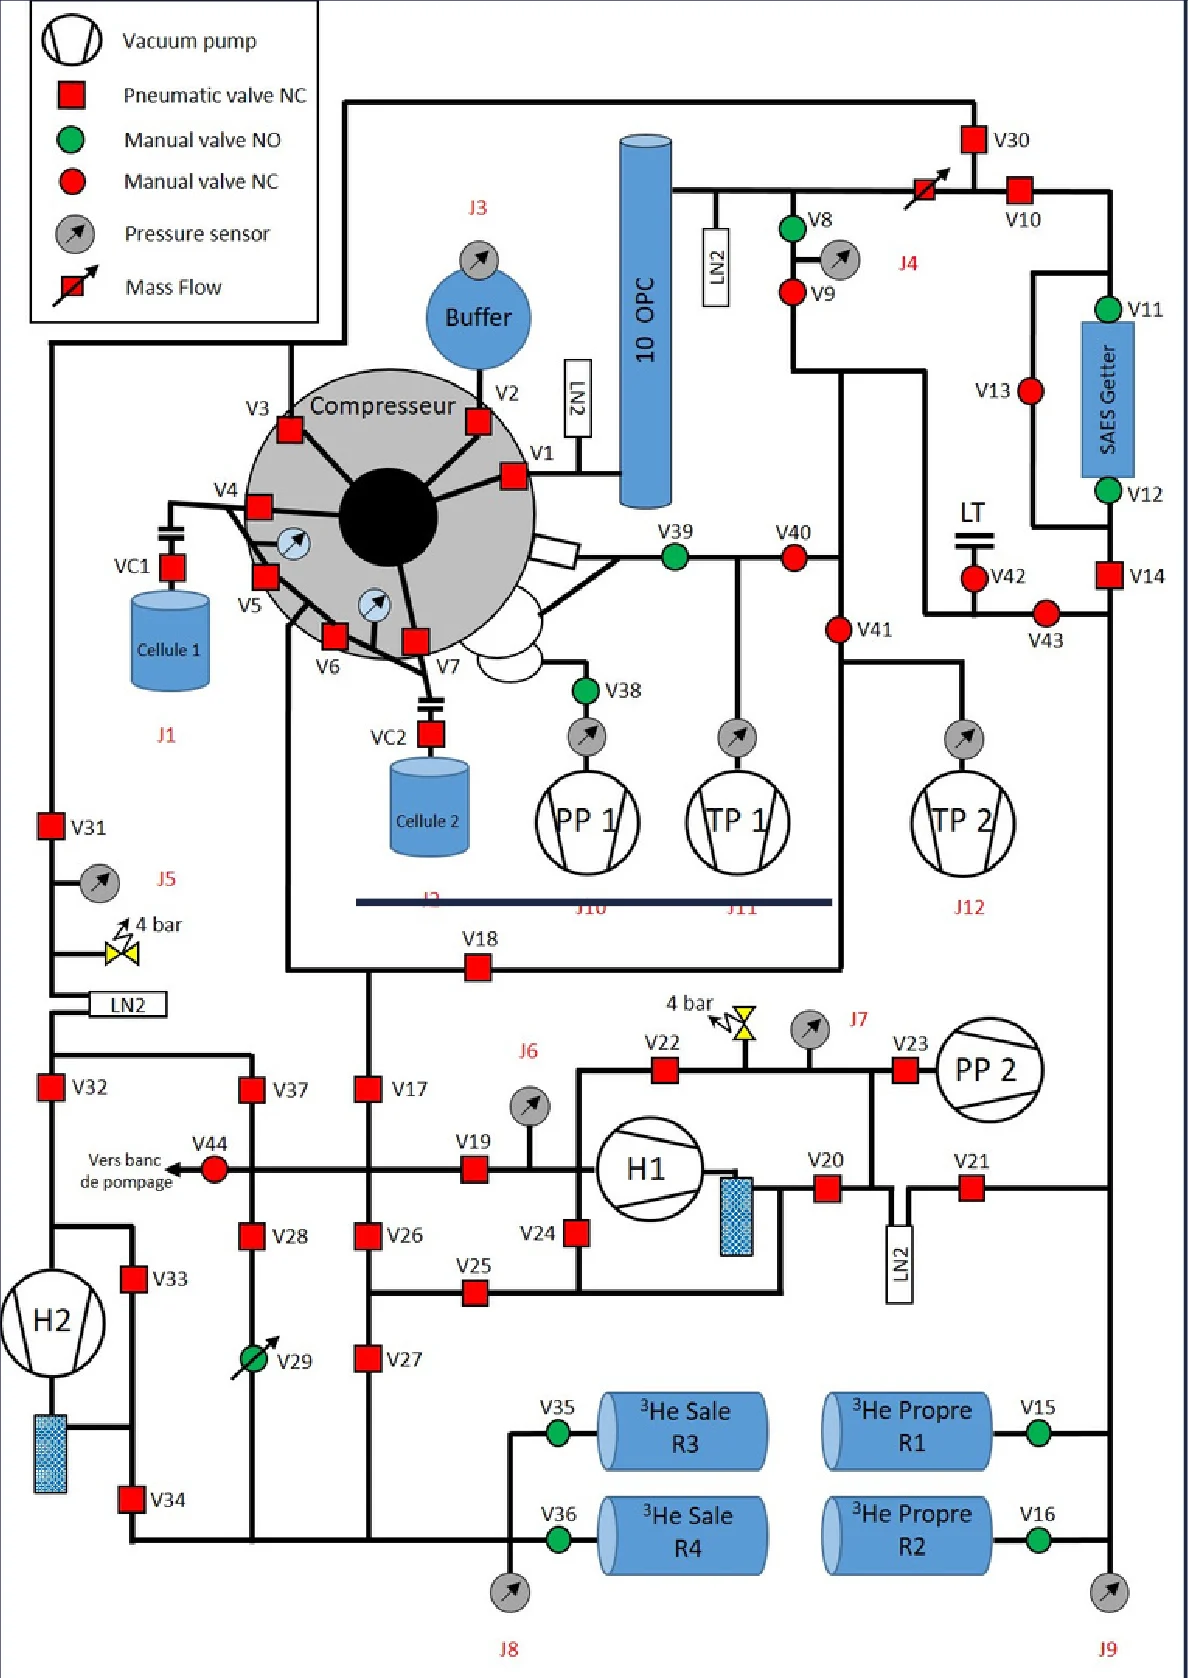
Tyrex-2 synoptic.
A successful collaboration
"Despite real in-house skills, once the machine had been built we decided to get support in choosing and implementing control software for the machine," says David Jullien.
"We issued a call for tenders. Among the solutions proposed, Nerys' stood out in several respects. The company had strong expertise in LabVIEW development. I also knew the good reputation of Mesulog, which had joined it within Nerys Group. Finally, I immediately noticed the possibilities offered by Vasco," explains David Jullien.
On the Nerys Group side, led by the duo Amaury Laurent and Benjamin Lerch, developer, there was plenty of enthusiasm for working on such a project. "The machine is magnificent and technically incredible," stresses Amaury Laurent, admiring the exceptional know-how at the ILL. "The sensor able to measure the polarisation of the helium, as well as the silicon experimental cells, among other things, were built in-house!"
"Technically, this type of project inevitably makes you progress," acknowledges Amaury Laurent.
He adds: "We encountered significant issues linked to the complexity of the machine. In particular, we had to be able to handle several actions taking place at the same time while the machine is running (simultaneous handling of two filling cells, opening and closing of valves…). We were able to provide solutions that further enrich Vasco, such as a mechanism for executing instructions remotely and exclusion locks that prevent unwanted states when two identical scenarios run simultaneously."
"The exchanges with David Jullien were very constructive. He has extremely detailed knowledge of the machine and had a very precise idea of what he wanted. He provided us with functional flowcharts, as well as mathematical formulas to work out trigger thresholds, setpoint pressure calculations, etc., which we integrated directly into Vasco," explains Amaury Laurent.
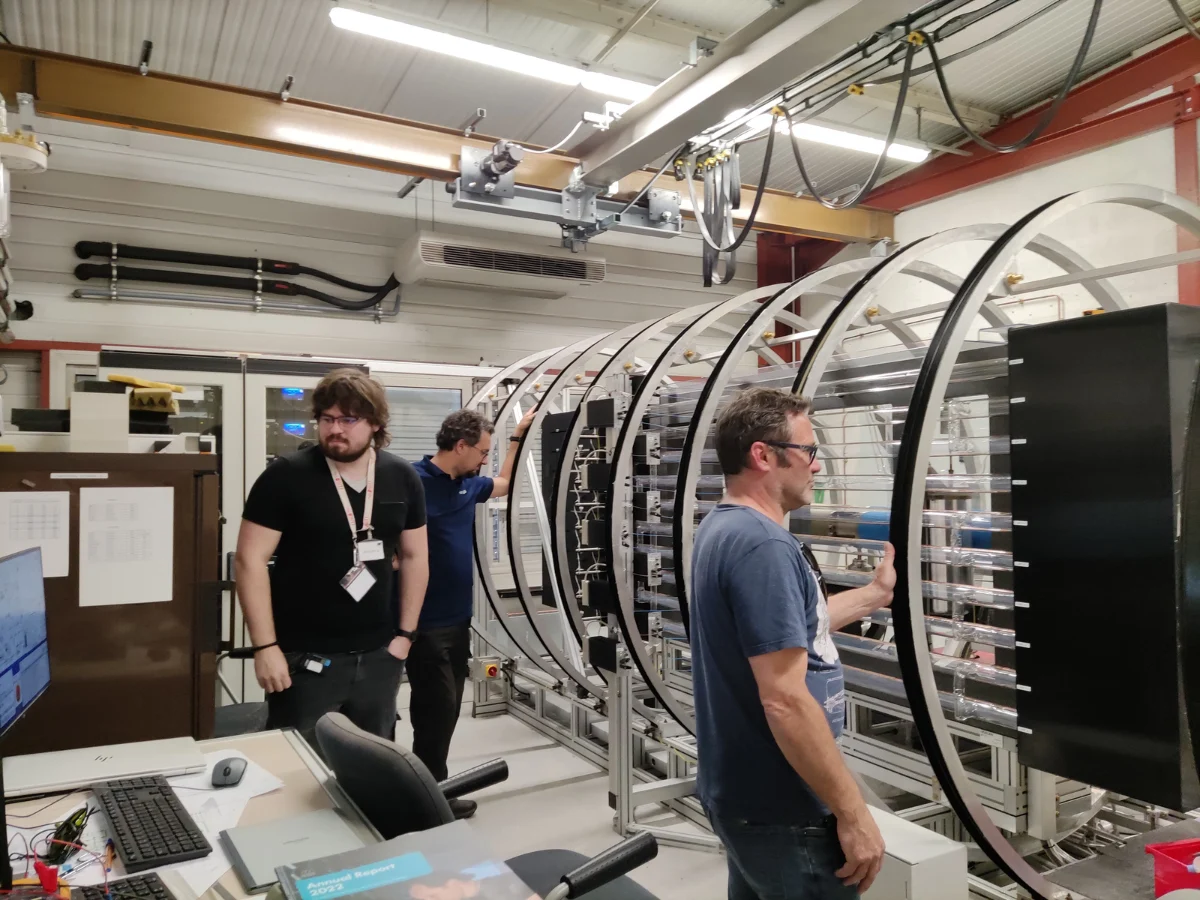
From the foreground, David Jullien, Benjamin Lerch and Amaury Laurent in front of Tyrex-2.
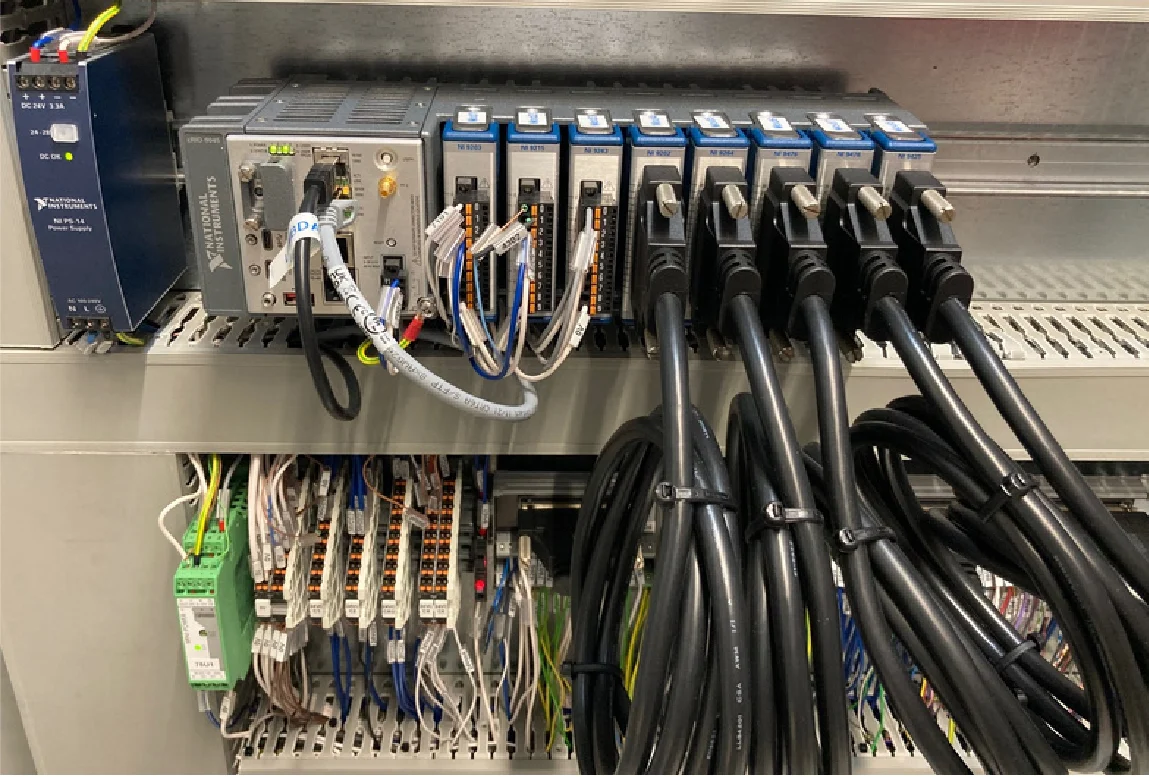
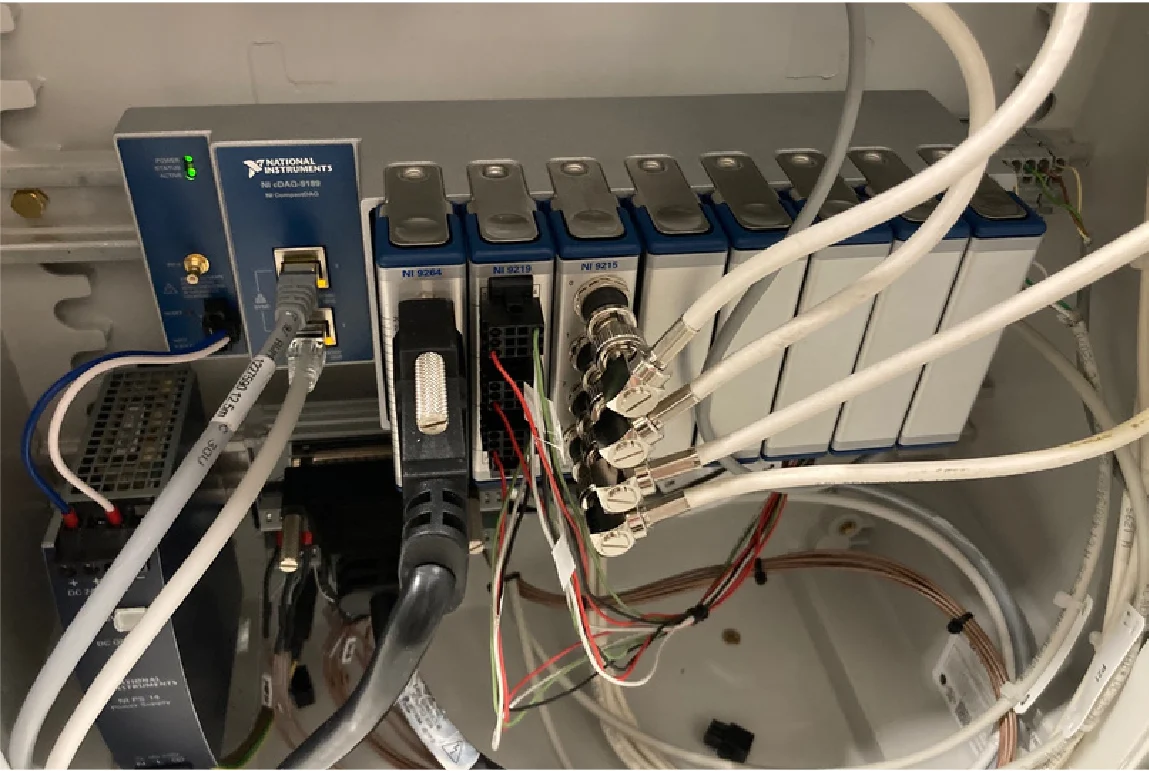
As for the acquisition hardware associated with the machine, the following organisation was set up:
A Windows PC runs Vasco and displays the control interface.
A CompactRIO runs Vasco RT (real-time). It handles the general control of the machine, the valves and the lasers. It also acquires the pressures. It also includes a distance counter and an hour counter for the cylinder.
A CompactDAQ, located remotely by the glass tubes, collects other measurements, in particular electric fields and those related to polarisation.
The two measurement devices are synchronised using TSN (Time-Sensitive Networking).
NI (Emerson) CompactRIO (photo 1) and CompactDAQ (photo 2) acquisition hardware used on Tyrex-2.
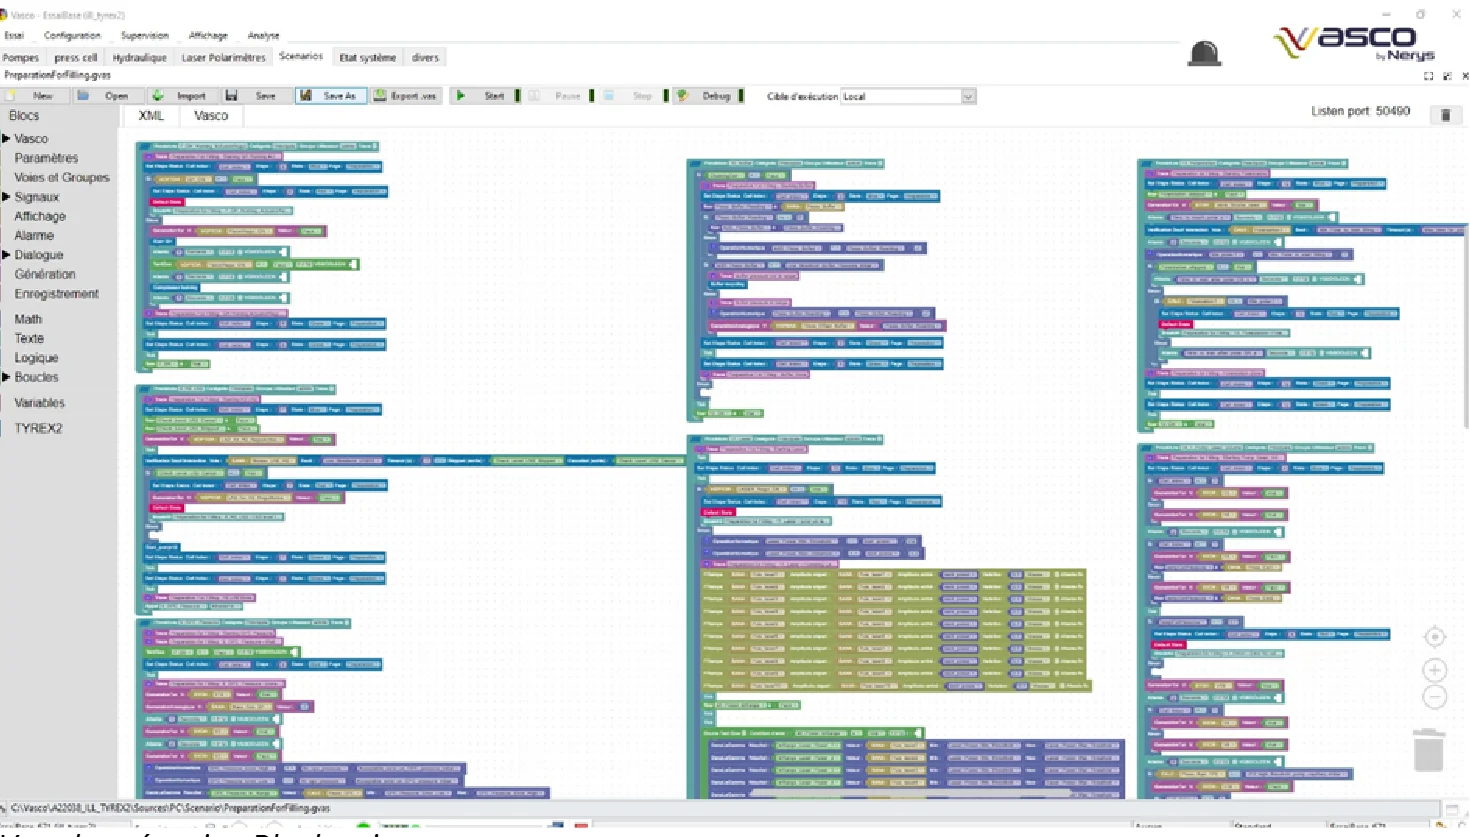
The two developers also highlight the strong added value brought to the scenarios. Nearly 2,700 lines of application scenarios were generated using Vasco's Blockscript module!
View of Blockscript scenarios.
Finally, they are also particularly proud of the look of the Tyrex-2 display and control interface, which is ergonomic, attractive and practical all at once.
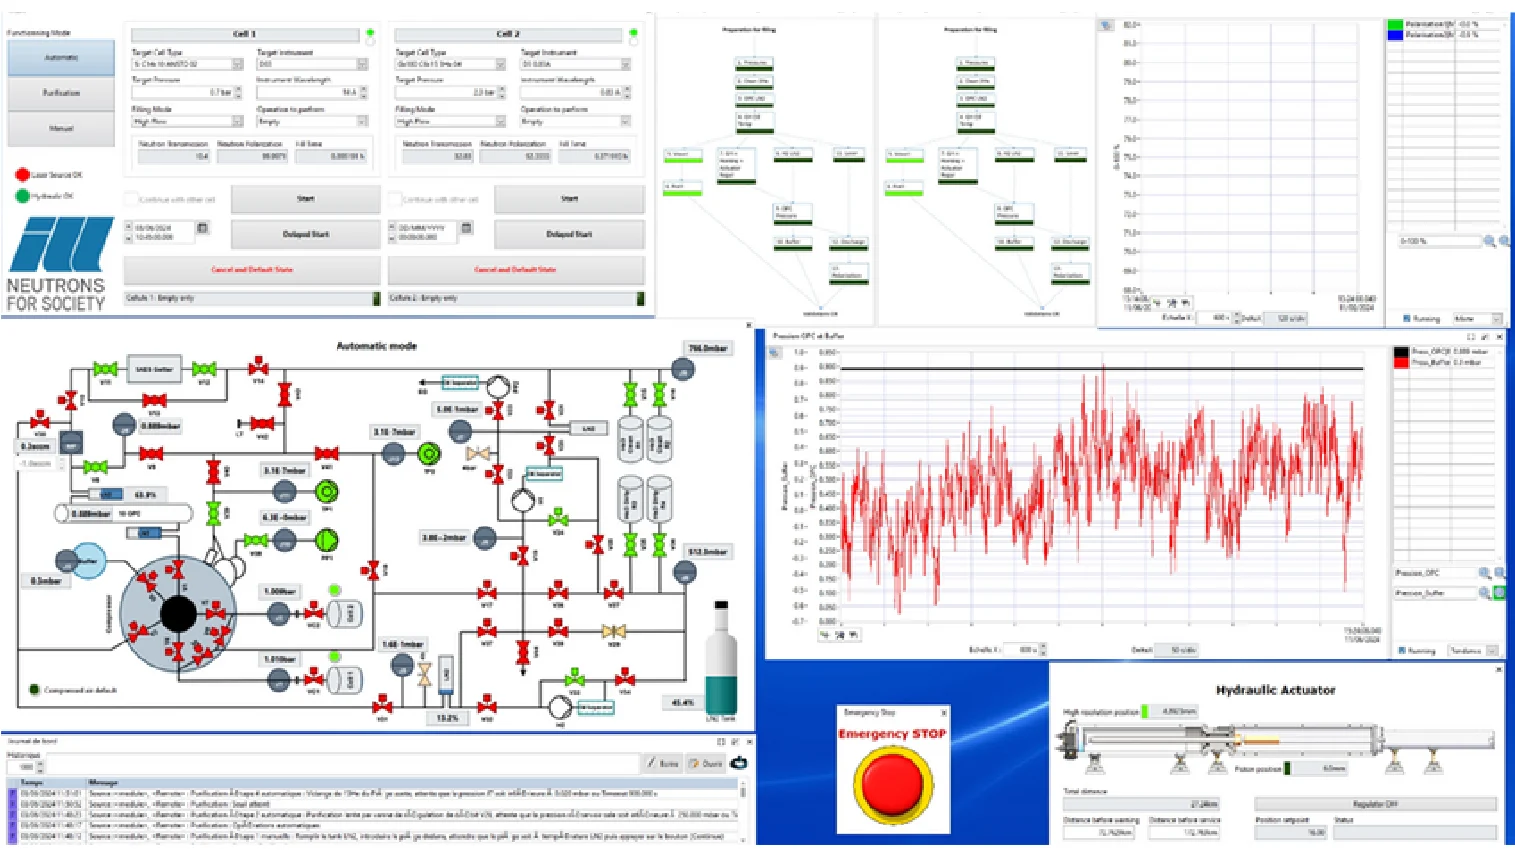
The interface shows the state of the machine in real time. The main dashboard displays two filling stations (two cells) fed by a database listing all the cells in the machine's stock. This database holds nearly 400 application parameters such as valve opening trigger thresholds, pressure setpoints, travel speed, calculation constants…
Specific interfaces were developed, in particular one for displaying and controlling the optical section, and another for supervising the hydraulic unit. A display also offers a realistic visualisation of the filling of the glass tubes.
View of the Tyrex-2 machine interfaces.
"We worked closely with David Jullien. He produced some of the visuals directly in LabVIEW and we integrated them into Vasco. The result is really very nice," says Amaury.
David Jullien is also delighted with the quality of the collaboration with Nerys. "Amaury, who was my contact throughout the project, has a very good understanding of things. He is very versatile, which is invaluable for understanding the workings and subtleties of a machine like Tyrex-2. He and Benjamin were responsive and very available, enabling us to complete the machine within the expected timeframe," stresses David Jullien. "Vasco also lived up to all its promises. I particularly appreciated programming scenarios with Blockscript, which saved me an enormous amount of time while commissioning the machine," he adds.
Most of the developments carried out for Tyrex-2 required no specific code, which shows that Vasco is a highly adaptable solution. Above all, although it was designed to supervise test benches, Vasco demonstrates its ability to control complex special machines. A machine similar to Tyrex-2 has been ordered by a Swedish centre that will also produce neutron beams. Vasco will be installed on this machine. What better recognition?
Interviews conducted and written by Khady Bathily. Thanks to David Jullien and Amaury Laurent for their testimonials. Photo credits: ILL - All rights reserved.
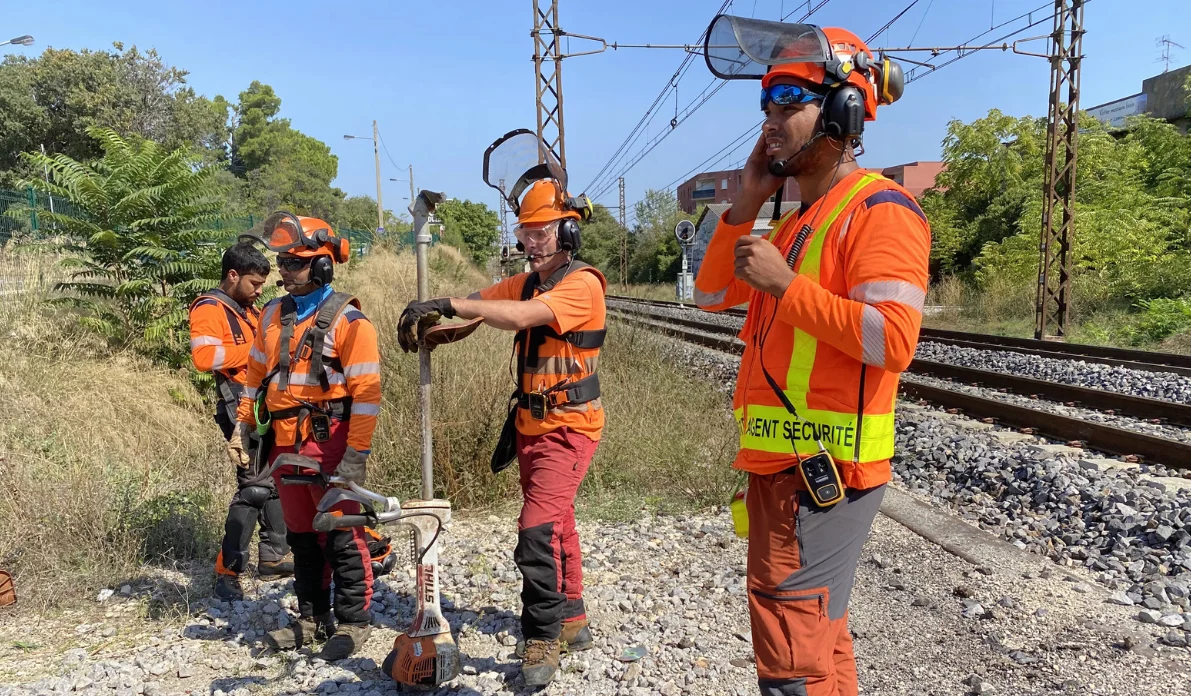
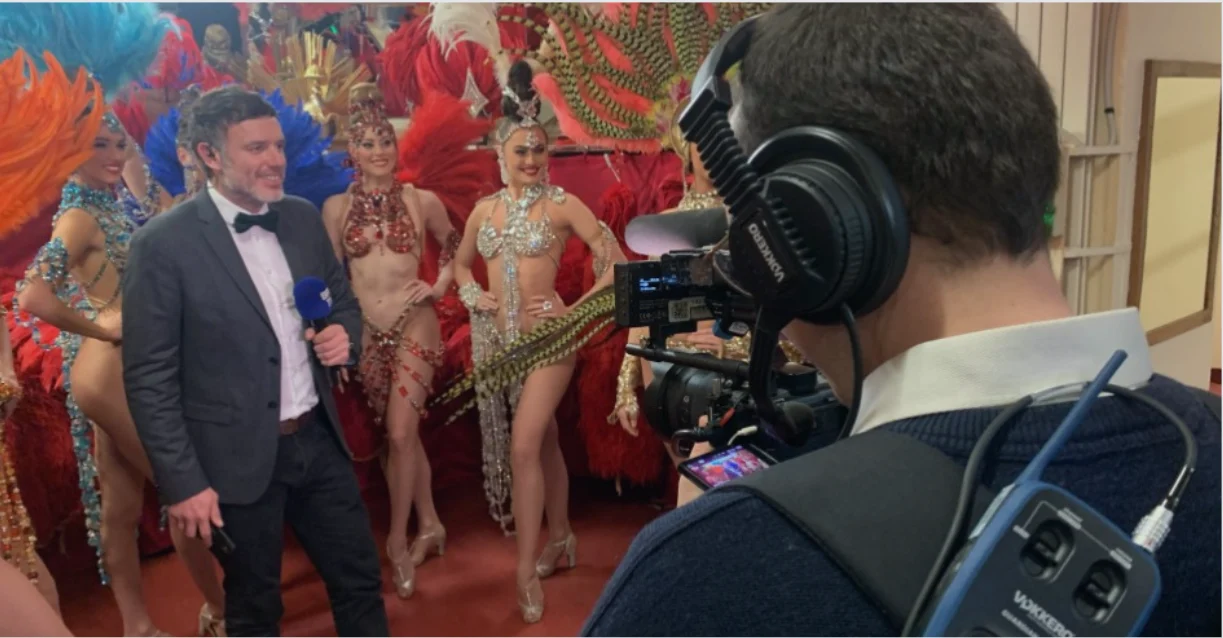
If you are a football or rugby fan, you have certainly seen referees equipped with an audio system from VOGO. The company, which specialises in the development of audio communication systems and live & replay video broadcasting, offers in particular VOKKERO radio systems, designed and developed for sports professionals (referees, doctors, coaches, video analysts), for field teams in industry (in particular construction, noisy industries, transport, energy and security) and for broadcasting.
The signature of these systems? They feature a patented noise filter that makes communication and work possible in very noisy environments such as stadiums, factories, construction sites and show/filming venues.
To guarantee impeccable reliability, these products are systematically subjected to rigorous testing. MESULOG, which specialises in the development of test and measurement software for industry, supported VOGO in rolling out automated test procedures, using NI TestStand, for an entire ecosystem of products.
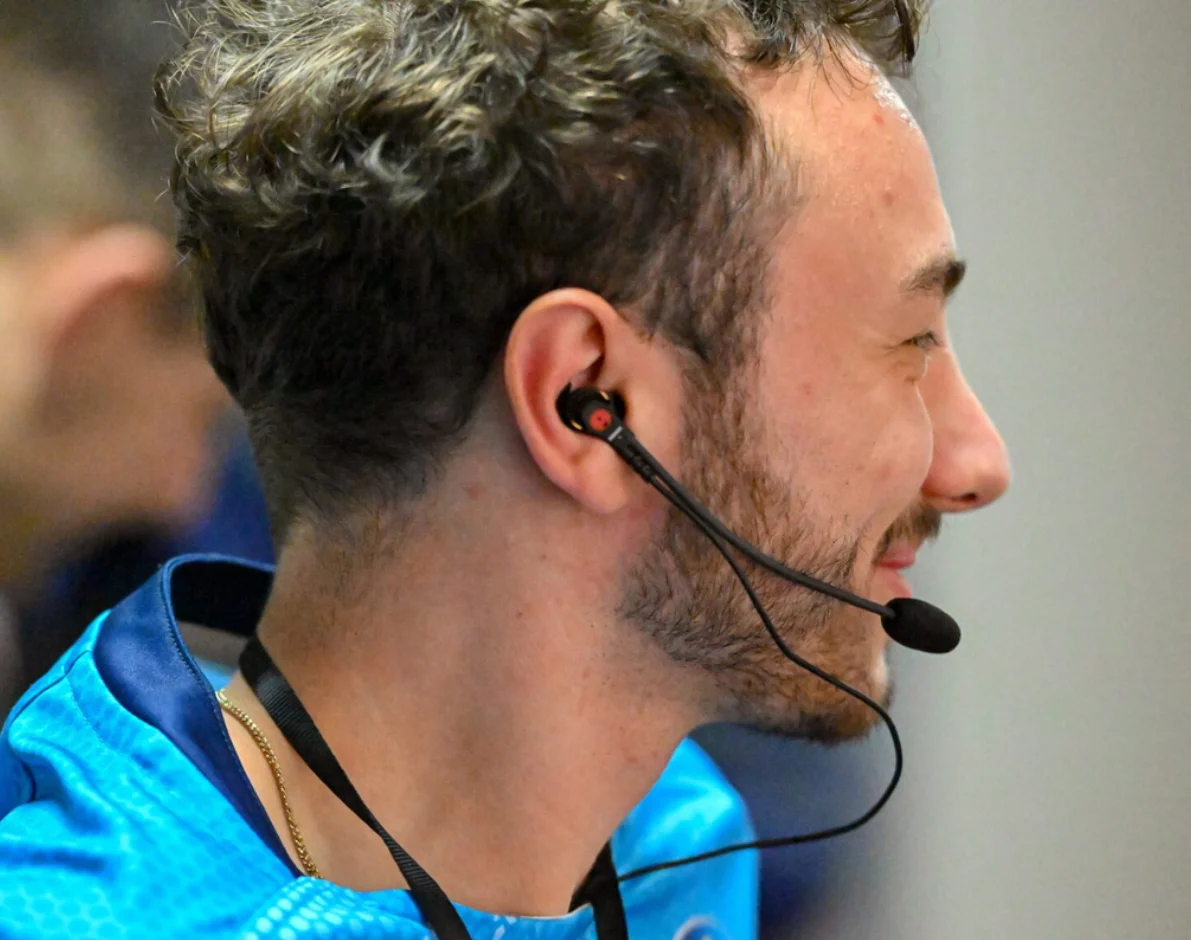
VOKKERO radio systems make it possible to communicate in very noisy environments.
A single piece of software to test the production of three product categories
"NI TestStand is a ready-to-use test sequencer used to automate validation and production tests. It offers the possibility of testing products one by one (sequential mode), in parallel or in batches. Whatever the mode used, each product gets a test report, which guarantees traceability of all operations," explains Damien Lamy, NI TestStand architect lead at MESULOG.
"Originally, we had developed a test engine in NI TestStand for ADEUNIS, which developed the VOKKERO systems before their acquisition by VOGO in 2019. This test engine was intended for ADEUNIS's IoT products. Fabien de Barros, technical manager at VOGO, saw an interest for the company, which wanted to automate its test procedures as much as possible for various products," says Damien Lamy. "We adapted the test engine accordingly, in particular to deploy a multi-product test part. We also developed a single piece of software to test the entire production of bare electronic boards, assembled products and configurator-chargers for the VOKKERO ELITE and VOKKERO GUARDIAN ranges," stresses the NI TestStand architect.
VOGO is the world leader in referee audio equipment.
Optimising single-product test sequences
"To understand our requirements in terms of product reliability and traceability, you have to consider how our products are used, particularly in sport. The television stakes are considerable. We are the world leader in referee audio equipment. We cannot accept our systems failing during a match!" explains Fabien de Barros. "Before our collaboration with MESULOG, we already had a bench to test bare electronic boards and assembled products, but we had no access to essential information such as tracking of quantities tested, failure rates... This feedback was all the more difficult as our manufacturer at the time was based in Malaysia. We have since brought production back to France," says Fabien de Barros.
Today, all bare electronic boards and assembled products are tested on two different platforms (or fixtures). The operator, who previously had to follow an instruction file, now simply selects the reference of the product to be tested via an operator interface. This interface also starts the test and displays the results. Some test sequences require manual actions by the operators. They are indicated by video, photo or audio media that MESULOG has integrated into the interface. "It is a real improvement from an ergonomic and operational point of view. It offers greater working comfort and peace of mind to our operators, who no longer fear making mistakes," notes Fabien de Barros.
The company has also subscribed to the WATS solution, developed by VIRINCO, for which MESULOG is the French partner. Using it with NI TestStand requires no additional development: "You just tick a box," explains Damien Lamy. "We use WATS a lot for supplier production monitoring. It lets us see the quantities of products tested, failure rates, scrap rates, the nature of the main failures, etc. We hold regular meetings with suppliers and ask them, for example, to take action when a defect recurs. This tool also allows us, remotely, to know much more easily what is happening, to upgrade the bench and to check that there are no problems with the test sequences. We are much more relaxed about any non-conformities raised by customers, because we have the full history of the products," illustrates Fabien de Barros.
Fully automated multi-product tests
"The major contribution of our partnership with MESULOG was the implementation of a multi-product end-of-line test bench and the development of tools for configuring systems at the end of the line," recalls Fabien de Barros. After testing the PCBs and assembled products, VOGO also checks the configurators used to charge the radio communication systems. They are also used to configure the terminals.
This device testing and configuration work was carried out, product by product, by an operator who consulted a file to find out which software (firmware) to load into each product. "You should know that our customers order kits made up of devices with different options. It was slow and, above all, a source of errors for operators. We replaced this manual work with pure automation. What is remarkable is that this major innovation in our process did not require the development of specific tools. MESULOG was able to adapt exactly to what our products do. We did not need to add any hardware other than our own. This is a real strength, because the product ecosystem remains the one we know, including for testing," stresses the technical manager.
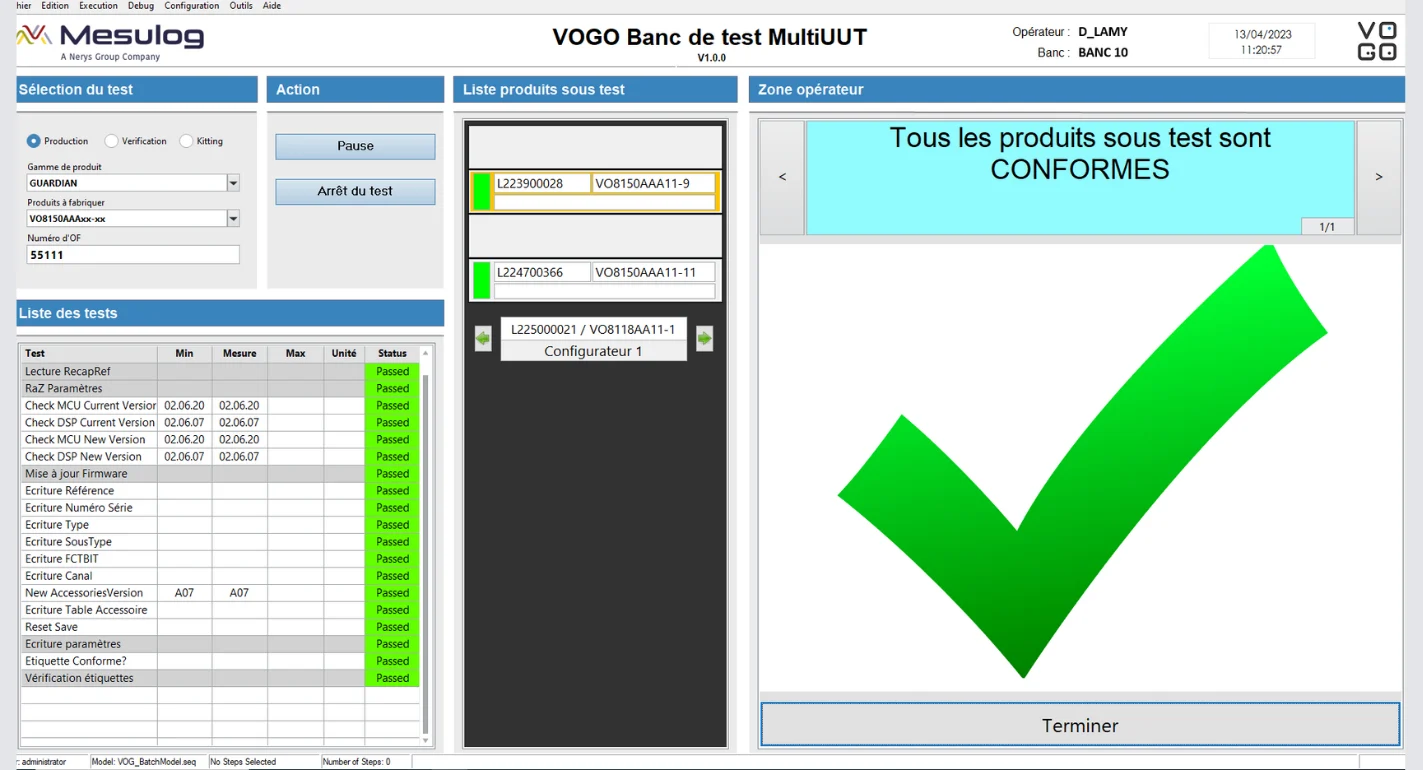
Configuring and testing a whole batch of products is possible simply by plugging the configurators in via a USB cable connected to the PC. As many configurators as the PC has USB ports can be put under test, and up to 12 products can be placed on each configurator. The operator only has to start the tests and launch the configuration of the products. Each configurator addresses each product independently. An operator interface shows the status of all products under test.
The company estimates the programming time for each product at around three minutes. For fifty products configured in parallel on five configurators, the operation takes half an hour compared with two and a half hours previously. Time during which the operator can carry out other tasks in parallel, whereas previously regular interventions were required, in particular checking and restarting programming between each configurator. "We can process a large number of devices at the same time! It is hidden time and productivity gains," says a delighted Fabien de Barros.
A view of the operator interface of the multi-product test bench developed for VOGO.
As simple as filling in an Excel file
MESULOG was also able to meet the specific features of VOGO's extremely diversified offering. "We offer a fairly varied ecosystem of products, because every customer request can be unique. Built around standard products, our systems are customised, which very regularly leads us to create new product references. This particularity could have been a real difficulty for our test procedures, on top of the R&D work, if adding new references had required the intervention of Damien or one of his MESULOG colleagues. Adding a product reference to the test simply requires updating an Excel file. It is a tool that is easy to read and maintain. This method gives us appreciable freedom. Ultimately, we can manage powerful test tools without having to get into the heart of the system."
"In the same spirit, MESULOG developed a multi-device hardware abstraction layer (HAL), which means the whole system is not affected. When we replace hardware and instruments, we just select the new driver. Beyond the technical expertise provided by MESULOG, I greatly appreciated their desire to foster our autonomy and Damien's availability," says Fabien de Barros.
VOGO, which is also known for its video replay broadcasting solutions, is considering a new collaboration with MESULOG in the short term. "We are going to call on them to deploy an automated test solution for audio headsets. It is the last element of the VOGO offering that is still tested manually at our premises. It represents a volume of 8,000 units per year. The tests are difficult for our operators to carry out and we encounter the same pitfalls inherent in manual operations. It is a real technical challenge, because advanced signal processing tools will have to be built into the development," challenges Fabien de Barros.
VOGO is also known for its video replay broadcasting solutions.
Written by: Khady Bathily. Thanks to Fabien de Barros and Damien Lamy for their testimonials. Photo credits: VOGO - All rights reserved.
Caroline Couvert, co-founder of NERYS, handed over the reins of the company and of NERYS GROUP on the occasion of her retirement on 2 February.
This transition marks the 100% takeover of NERYS GROUP by the employees of NERYS and MESULOG and the arrival at the head of the group of Sylvain Bistagne and Luc Desruelle.
An expert in management and change management, Sylvain Bistagne supported NERYS for many years in its structuring and already leads the development of NERYS GROUP's consulting, services and training activities. He will manage NERYS and NERYS GROUP.
Luc Desruelle, managing director of MESULOG, will chair NERYS GROUP, thus ensuring technical and strategic continuity within the group. His technical expertise, in particular in software development (NI LabVIEW), is a reference in the test and measurement sector.
For Sylvain Bistagne and Luc Desruelle:
"We firmly believe that this handover to the employees was the best way forward. We are proud that the team shares this vision and unanimously supports this evolution. With their enthusiasm, commitment and skills, we are ready to take on tomorrow's technological challenges and continue to innovate alongside our customers and partners."
"In 2007, when we founded NERYS with my partners Marcel Auboiroux, Jean-Philippe Roth and Thierry Pugliesi, our goal was to build an innovative company, but we also wanted to create a human-sized company to guarantee closeness to our team and our partners. This handover to the employees is full of meaning. They work with customers every day and are their preferred contacts. Partners appreciate the takeover and continuity of activities by the team," stresses Caroline Couvert.
Caroline Couvert guided NERYS towards gradual growth, carrying out large-scale projects for demanding sectors such as defence, aerospace, space, nuclear and automotive. The company reached a decisive turning point in 2022 with the creation of NERYS GROUP, following the strategic acquisition of MESULOG.
Among her many achievements, Caroline Couvert initiated a virtuous business model built around values of participative governance. As she passes the torch to Sylvain Bistagne and Luc Desruelle, she hands over a solid organisation, focused on the future and ready to meet the most demanding expectations and challenges of NERYS GROUP's partners.
The whole NERYS GROUP team expresses its deepest gratitude and thanks for her leadership, passion, commitment and kindness over these 18 years.
On 16 and 17 October, Nerys Group is at the Mesures Solutions Expo trade show at the Lyon Convention Centre. You can find our team on stand B41. We also had the pleasure of giving, on the first day of the event, a technical talk on the theme "Measurement system performance: is it possible to transmit signals without 'noise'?" Many thanks to the many participants, to Réseau Mesure, the show's organiser, for this opportunity, and to our pair of experts, Amaury Laurent and Frédéric Bernard, for their brilliant, lively presentation.
On a machine, in a laboratory or in a factory, taking a quality measurement is a challenge. Our two experts, with years of professional experience and backgrounds in instrumentation and applied physics, tell the wild story of an analogue signal in a hostile world of noise and interference.
Objectives of this presentation
Understand and deal with noise in the various elements of the measurement system.
Is it possible to transmit signals without noise?
Performance depends on your application: performance = subjective
Understand what is at stake to avoid the pitfalls
Our presentation is not a course – it is our vision – our expertise.
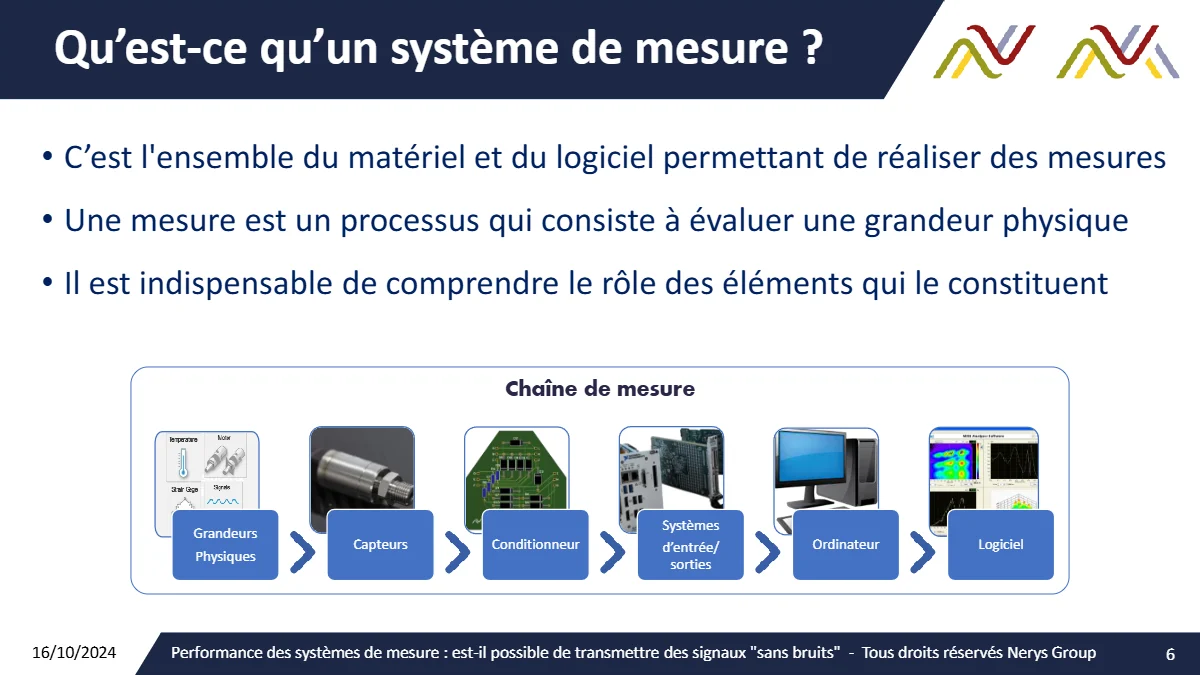
What is a measurement system?
It is all the hardware and software used to take measurements
A measurement is a process that consists in evaluating a physical quantity
It is essential to understand the role of the elements that make it up
The measurement chain: physical quantities, sensors, signal conditioner, input/output systems (acquisition and output), computer, software.
From theory to practice
Just connect the elements and it measures. Sometimes in the laboratory… but rarely in real life. Why? Because there is noise on the measurement…
Measurement noise: definition
Noise is the set of parasitic signals superimposed on a piece of information.
In our case, they are induced by sources external or internal to the measurement system
Various origins:
Mechanical: vibrations, expansion…
Electrical: switch-mode power supply, poor-quality earth…
Environment: temperature, radiation…
Wiring: interference between signals
The signal-to-noise ratio is generally quantified in dB
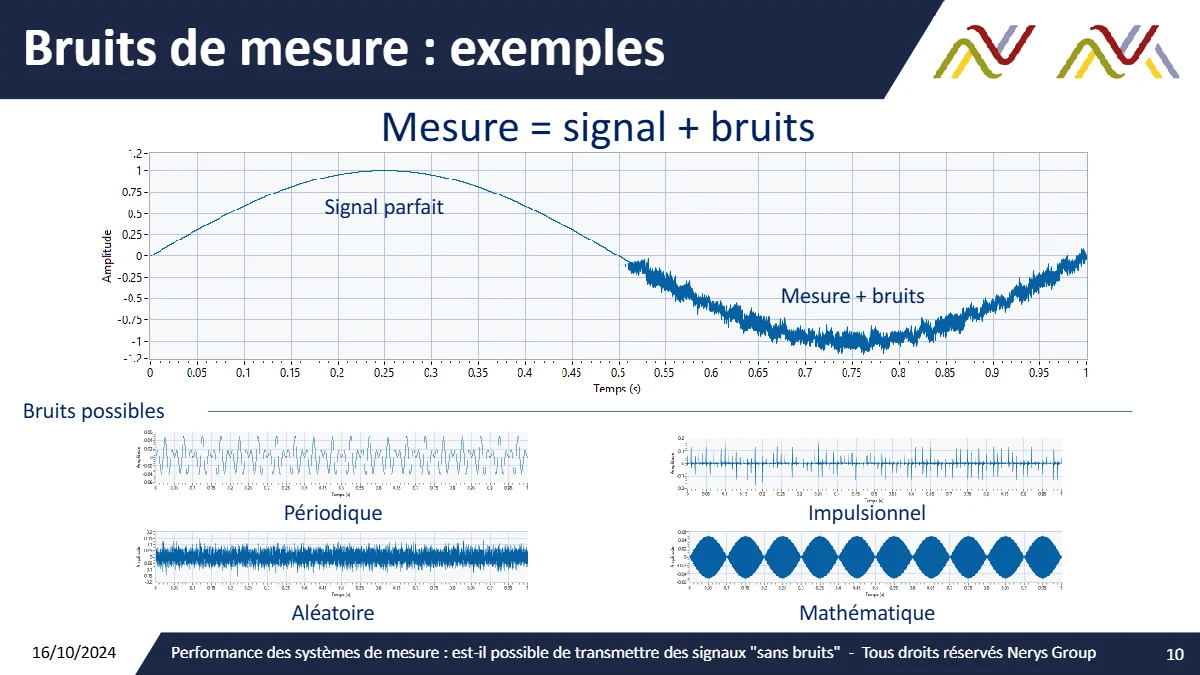
Measurement = signal + noise. Possible types of noise: periodic, impulsive, random, mathematical.
The story begins with the sensor…
It is the origin of the measurement.
Transducer: converts a physical signal into an electrical signal
The sensor is where "the noise" begins
A few examples of characteristics for selecting a sensor: accuracy, range – full scale…
… to reach digitisation…
Digitisation converts the electrical signal into usable information
Many criteria must be taken into account
Compromises often have to be made: signal types, number of input/output channels, amplitude, sampling rate, resolution, bandwidth, price…
The electrical quantity supplied by the sensor may be a voltage, a resistance, a frequency or any other electrical attribute.
Condition the signal: adapt the type of electrical quantity
Amplify: adapt the dynamic range of the signal
Isolate: adapt the electrical reference of the signal
The sensor is rarely compatible with the digitisation system. It needs to be adapted.
In addition to adapting the sensor, the conditioner can strengthen the signal to reduce the influence of noise:
Amplify because too weak (100 µV → 10 V)
Filter because noisy (50 Hz notch filter)
Galvanically isolate (reference adaptation)
The conditioner must be as close as possible to the sensor to avoid propagating noise.
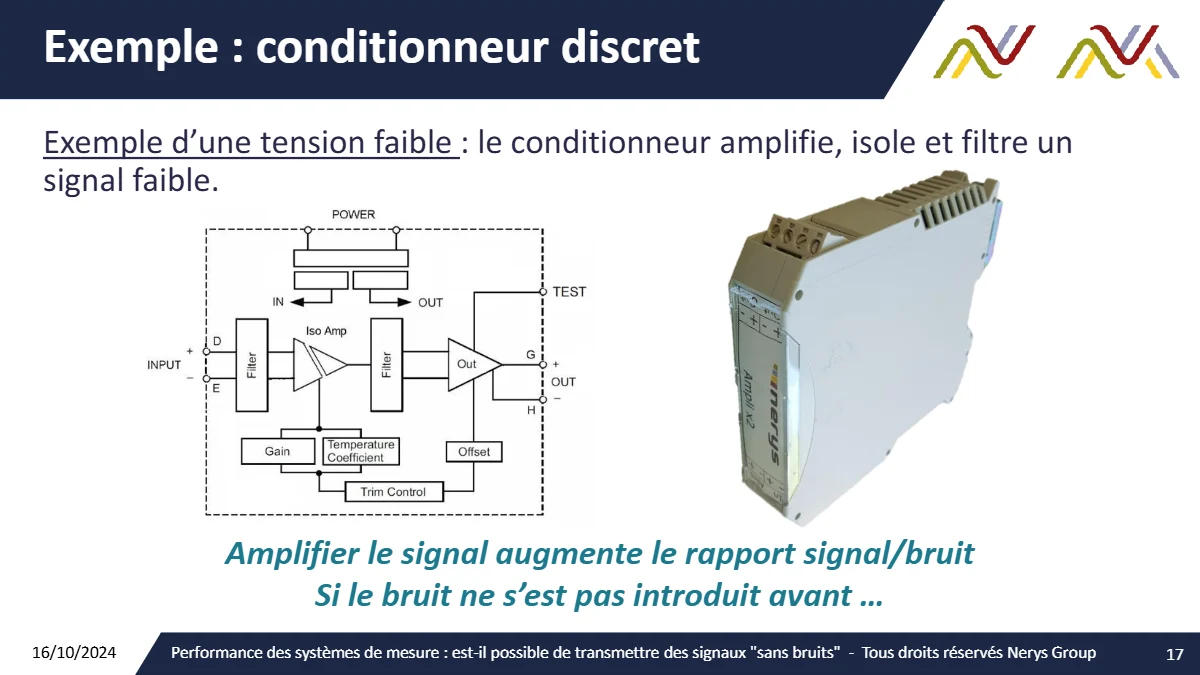
Example: discrete conditioner. Example of a low voltage: the conditioner amplifies, isolates and filters a weak signal. Amplifying the signal increases the signal-to-noise ratio, provided the noise did not get in beforehand…
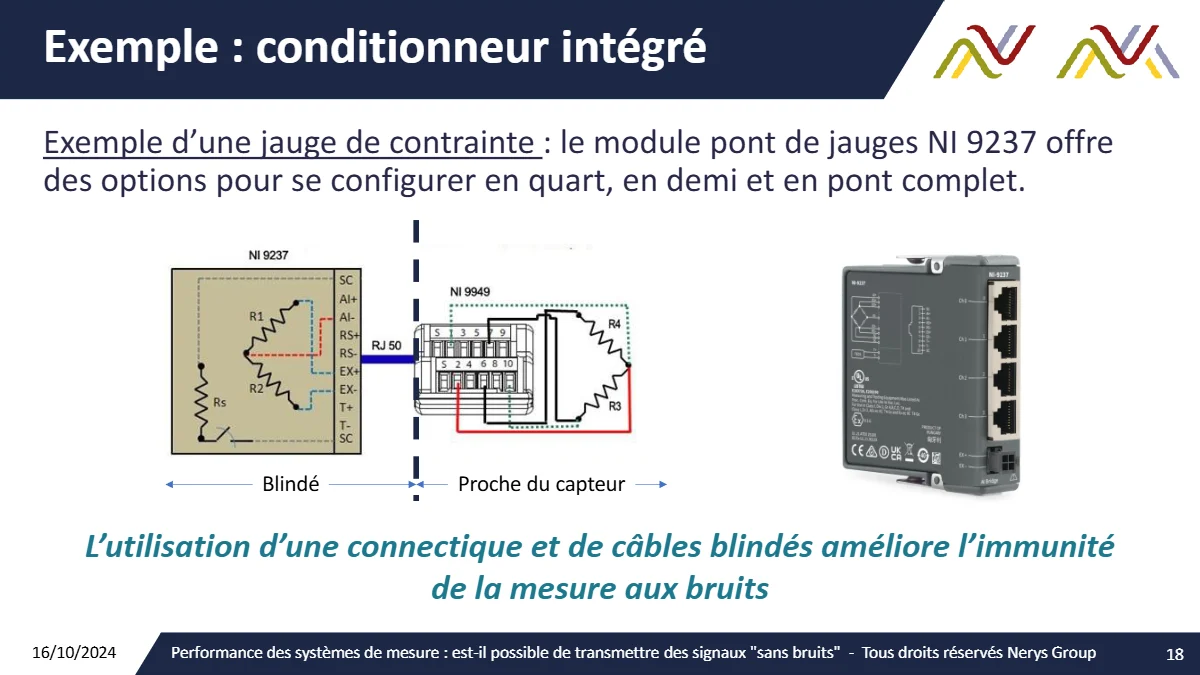
Example: integrated conditioner. Example of a strain gauge: the NI 9237 bridge module offers options for quarter-, half- and full-bridge configuration. Using shielded connectors and cables improves the measurement's immunity to noise.
… from cable to cable…
The influence of wiring is too often forgotten! Good practices are essential. Not following them can lead you to measure more noise than signal.
A few reminders
Some signals are more sensitive to noise: a voltage is more easily disturbed than a current or a frequency
A measurement is often a voltage
Voltage is the difference in electrical potential between two points
Ground is the reference for electrical potentials
Ground is often referenced to 0 V by being connected to earth
Good practices…
Separate high-power and low-level circuits
Respect the referencing modes (referenced, non-referenced, differential, pseudo-differential)
Avoid circulating currents:
Avoid ground loops
Ensure good-quality equipotential bonding
Balance impedances
Avoid floating signals
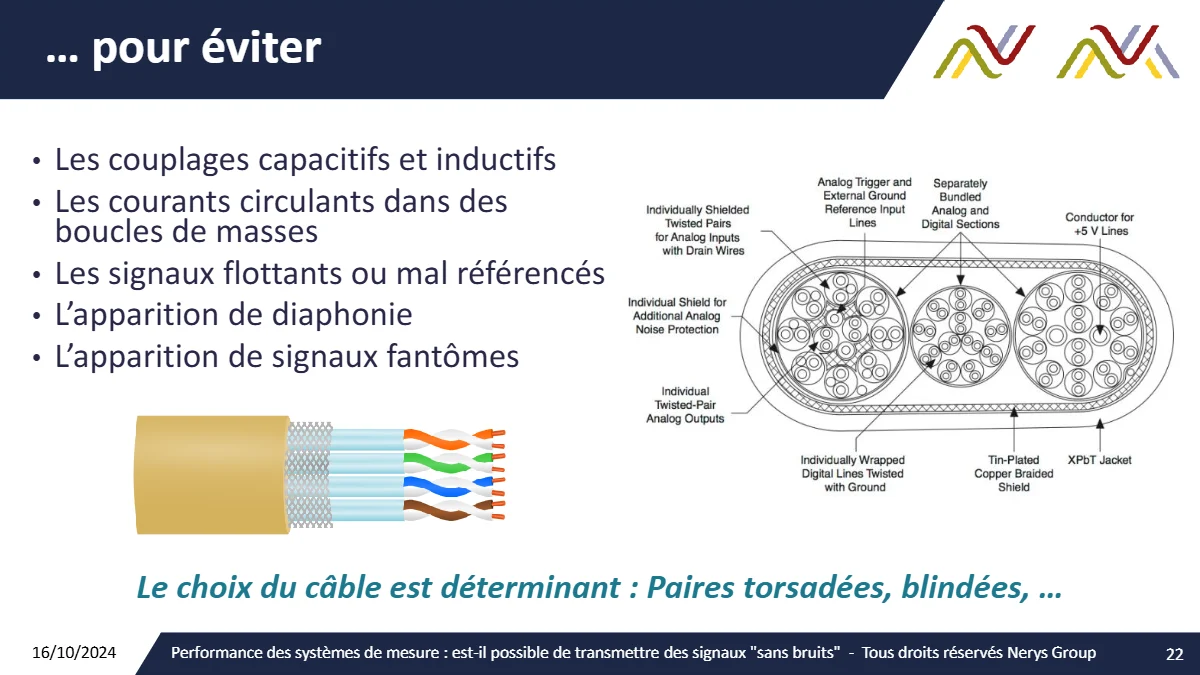
… to avoid
Capacitive and inductive coupling
Currents flowing in ground loops
Floating or poorly referenced signals
Crosstalk
Ghost signals
The choice of cable is decisive: twisted pairs, shielded…
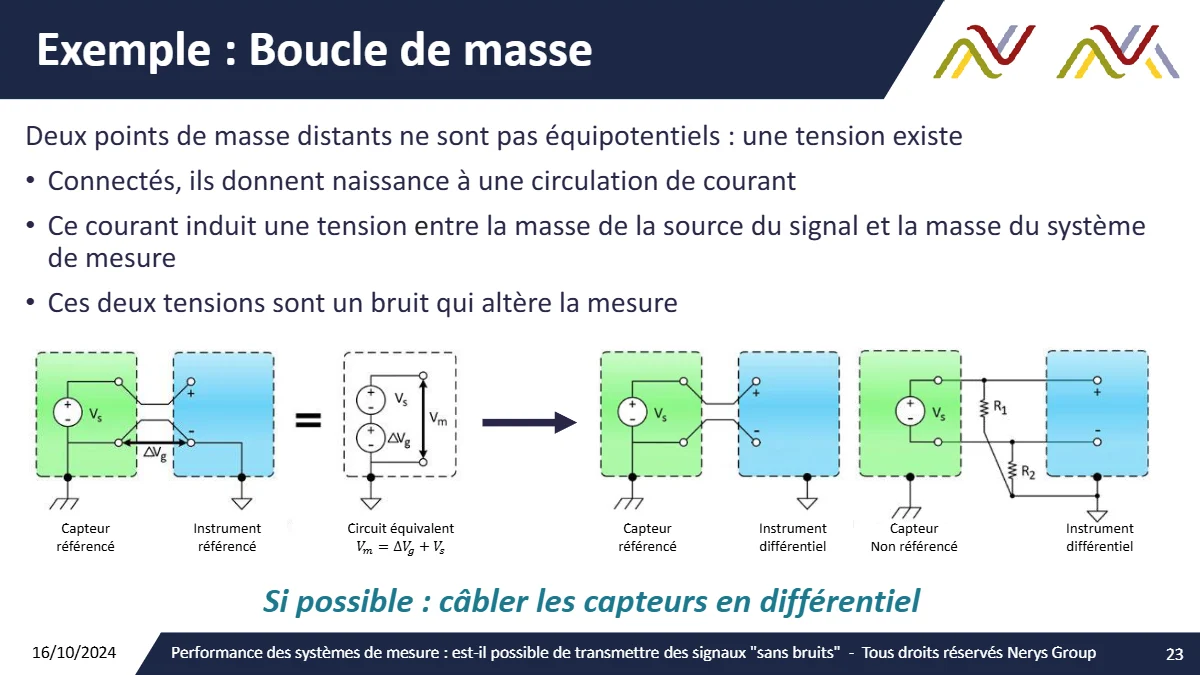
Example: ground loop. Two distant ground points are not equipotential: a voltage exists.
When connected, they give rise to a circulating current
This current induces a voltage between the ground of the signal source and the ground of the measurement system
These two voltages are noise that corrupts the measurement
If possible: wire the sensors in differential mode.
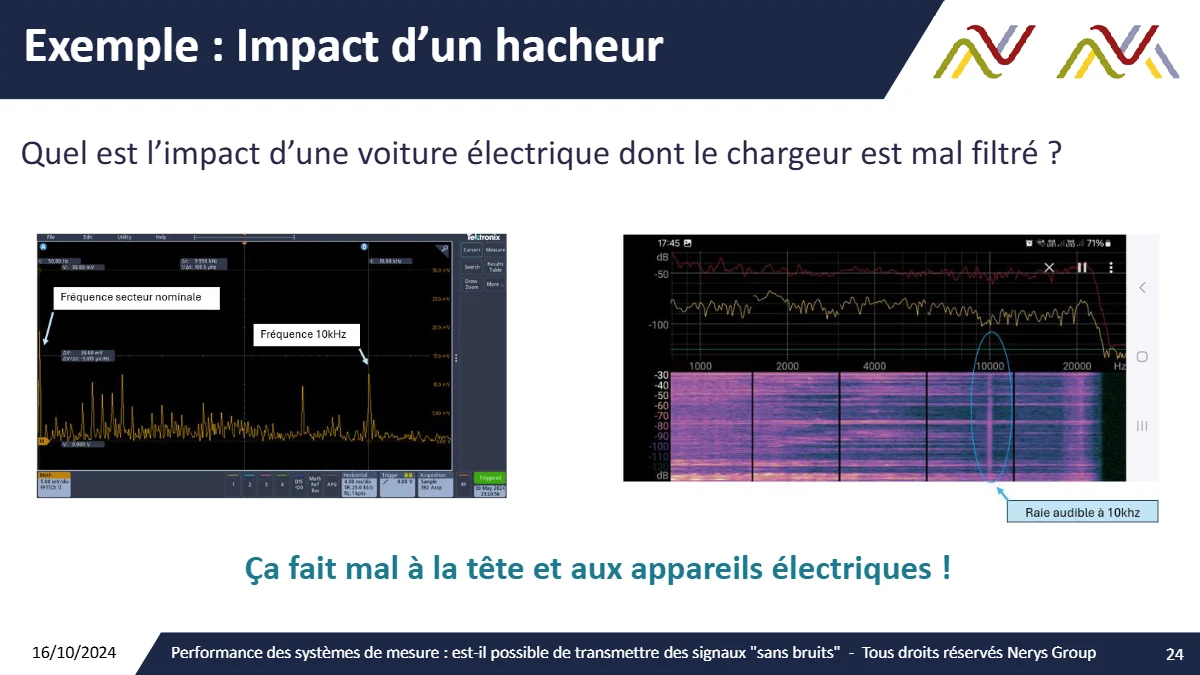
Example: impact of a chopper. What is the impact of an electric car whose charger is poorly filtered? It hurts your head and your electrical equipment!
Beware of computers. The computer is currently the preferred platform for instrumentation systems. Acquisition hardware often shares the same reference as its computer.
A desktop computer is referenced to earth via the wall socket: the acquisition system may be poorly referenced.
A laptop is unreferenced on battery and rarely referenced by its charger: the acquisition system may be floating. Adding a reference to the system must then be considered by connecting its 0 V to ground.
Let us not forget that for a quality measurement it is imperative to have a single point of contact with ground.
… and ends up in the software
Too late!
The noise has taken hold
It has been amplified
It has multiplied
It has distorted the signal
It is still possible to attenuate it using the software (filtering) or to quantify it (FFT…).
A few points to watch
Resolution must be consistent with accuracy
Beware of non-linear calculations (RMS, log…)
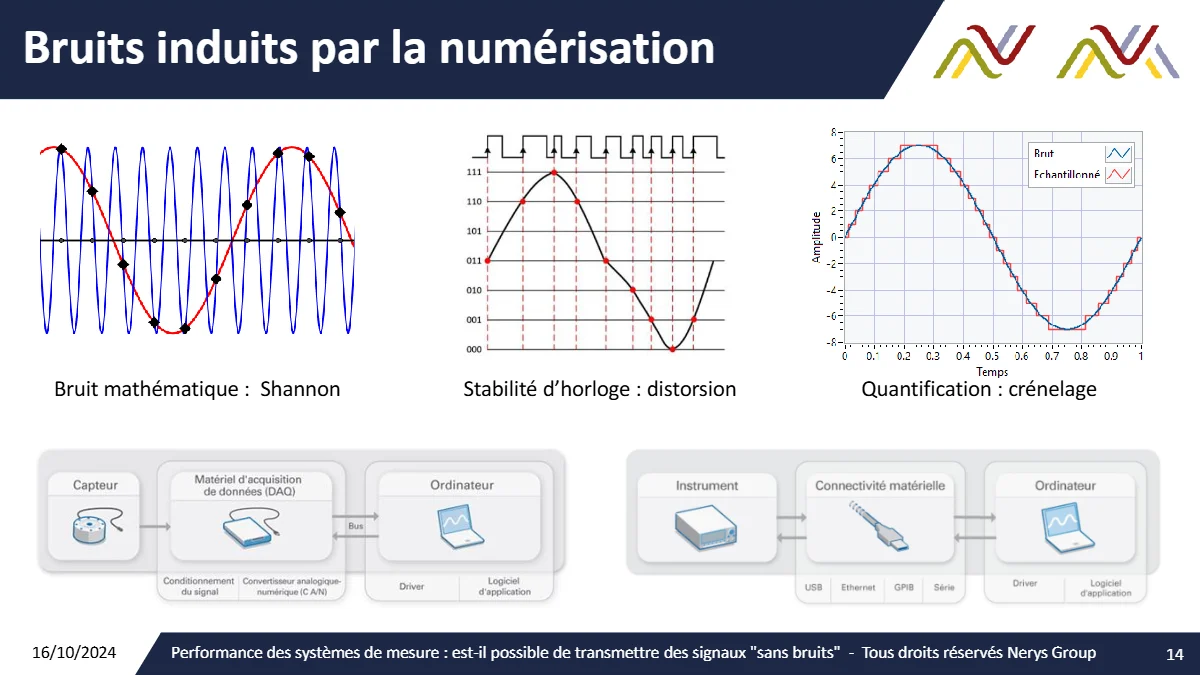
Data encoding can degrade the signal
Rounding or truncation may be lurking in the algorithms
Accumulation of residuals is possible (recursive filters)
Mathematical phenomena can modify the signal (convolution, windowing…)
Conclusions
Transmitting signals without noise in a high-performance measurement system:
There is no measurement without noise; the aim is to minimise it
The further upstream noise enters the measurement chain, the greater its impact
To transmit a signal well, it is important to know it
Dealing with noise as early as possible prevents it from propagating
Respecting the electrical reference is a fundamental point
We are pleased to inform you that NERYS GROUP will take part on 16 and 17 October 2024 in the MESURES SOLUTIONS EXPO trade show at the Lyon Convention Centre. Our company's second participation in this major show, organised by Réseau MESURE, will have a special flavour, as we will be involved in several ways.
First of all, Stéphanie GARRON and Florent FONTEIX will be pleased to welcome you on our stand B41 on Wednesday 16 and Thursday 17 October. Feel free to come and meet them to introduce yourself and discover our various professions: designer of test benches and measurement systems, developer of industrial software, trainer…
Amaury LAURENT and Frédéric BERNARD will give a technical talk on the theme: "Measurement system performance: is it possible to transmit signals without 'noise'?", on Wednesday 16 October at 3:30 pm. Learn more about this talk
We look forward to seeing you at this reference event for our industry. It promises to be rich in discoveries and quality exchanges.